
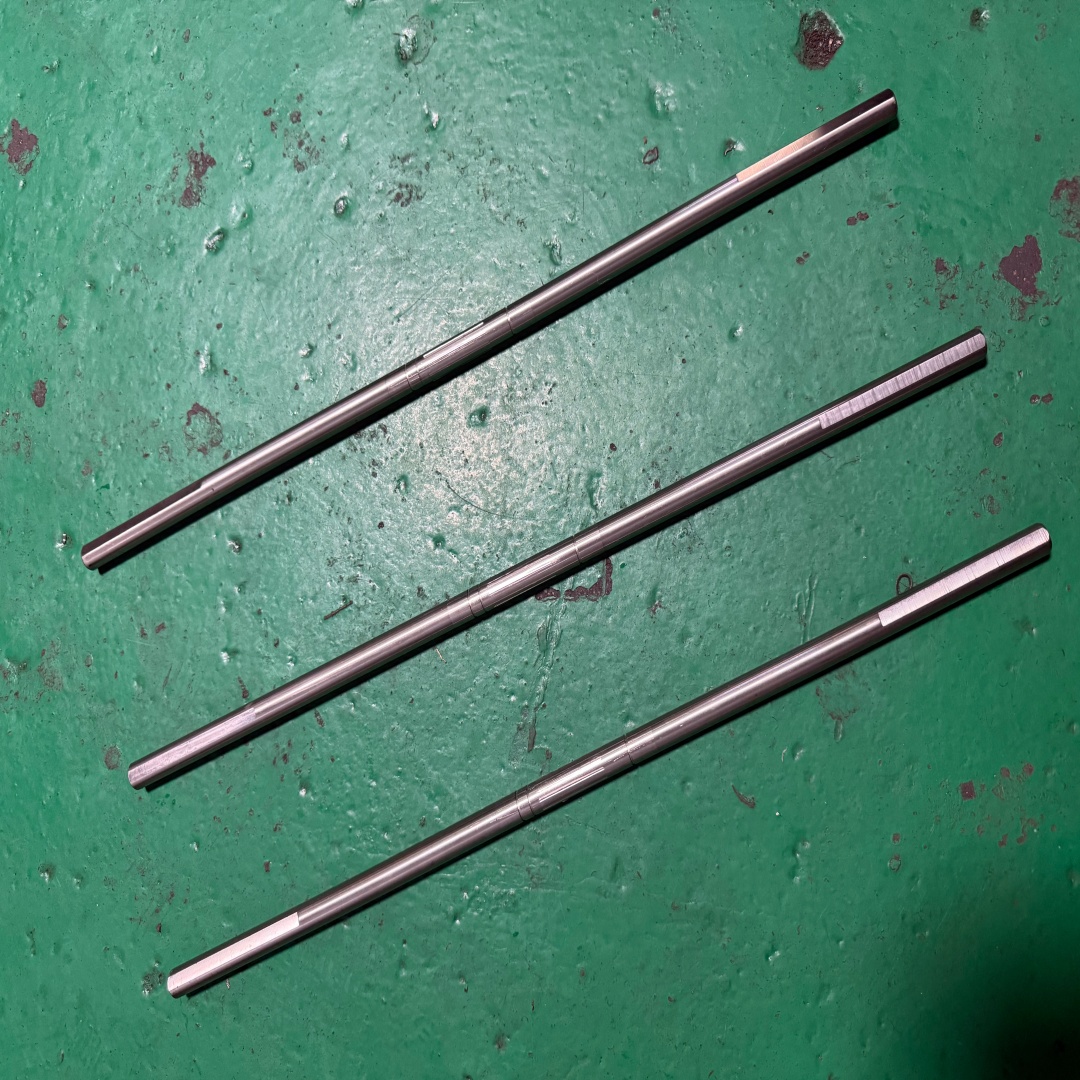
A shaft straightening machine for steel shafts and cylindrical bar-type parts has to do more than “make the bar look straight”: when the workpiece contains several diameters, the machine must rotate the part on an agreed datum, measure only approved diameters, select one or more safe correction points, and protect the specified surface finish. This page is the product page for automatic straightening of shaft type parts—the tested machine specification and video first, then the complete engineering layer: runout and datum logic, why this family is difficult, the closed-loop process, and the controlled-benchmark method for replacing existing equipment.
Tested Specification and Machine Video
Tested workpiece for this trial: steel shaft, 12 mm diameter x 400 mm length, required straightness 0.1 mm. The machine runs the full automatic loop—rotational multi-point measurement, servo press correction, and complete remeasurement—as shown in the video.
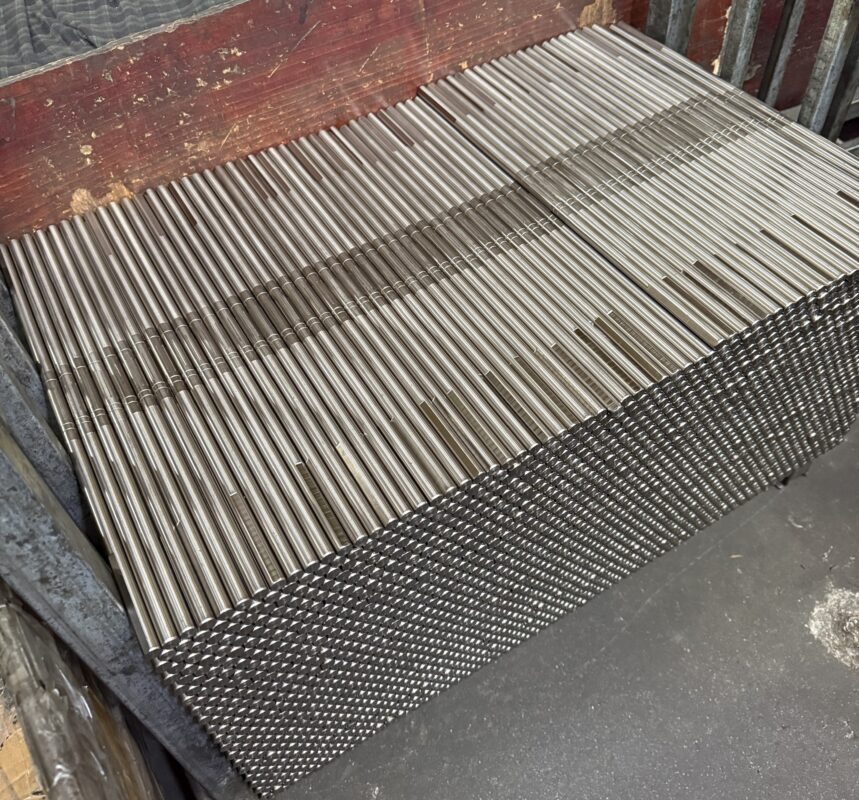
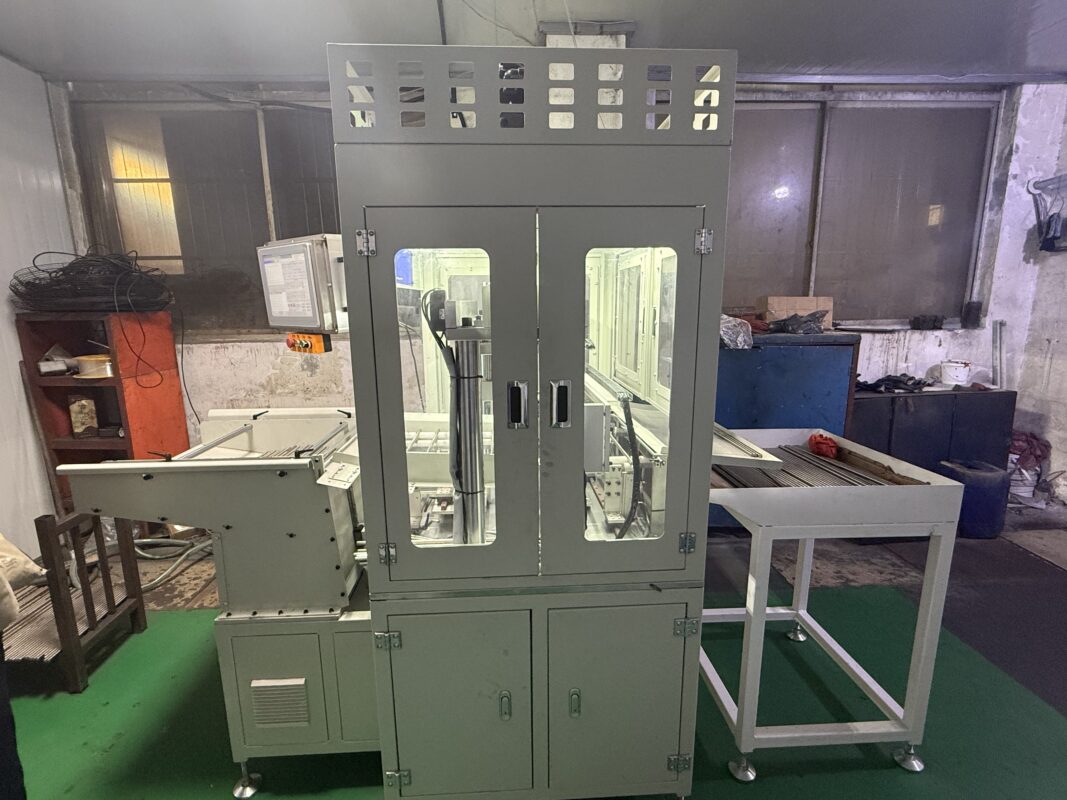
Steel Shaft / Bar Project Requirements
Steel shafts and cylindrical bars develop bow and radial runout after heat treatment, turning, grinding, storage, or handling. One reported project brief for this family is based on 25 steel or equivalent material, hardness HB 241–302, lengths from 183 to 720 mm, and measuring diameters from 14 to 23.5 mm, with a maximum incoming runout of 0.5 mm, a target outside-diameter runout of 0.2 mm, and 1–5 straightening points. These are project inputs: they must be correlated with the drawing, datum, measuring positions, and representative sample tests before they become machine acceptance guarantees.
| Project Item | Customer Input / Status |
|---|---|
| Workpiece | Steel shaft / cylindrical bar-type part; final application to be confirmed |
| Material | 25 steel or equivalent; exact standard and certificate required |
| Surface roughness | Ra 1.25 μm |
| Hardness | HB 241–302 |
| Maximum incoming runout | 0.5 mm customer input |
| Target OD runout | 0.2 mm customer requirement; datum and measuring method to be confirmed |
| Measuring diameter | 14.0–23.5 mm |
| Other diameter | 14.0–28.5 mm |
| Length | 183–720 mm |
| Straightening positions | 1–5 customer input; measuring/correction-point definition required |
| Proposed method | Automatic rotating measurement with point press-straightening and full remeasurement |
The project data distinguishes measuring and non-measuring diameters, which indicates a rotating shaft/runout inspection problem rather than a simple full-length straightedge check. The final drawing must identify the functional datum, the exact measuring diameters, and the features that may be used for support, rotation, and pressing.
Radial Runout Is Defined by the Datum
Radial runout is the difference between the maximum and minimum probe readings while the workpiece rotates around a defined axis. If the shaft is supported on centers, two journals, rollers, or another pair of diameters, each setup can produce a different result—the 0.2 mm target must therefore be connected to the same datum used in the final inspection. Straightness and runout are related but not interchangeable: a straight surface can still show runout if the datum is eccentric, and an apparently acceptable runout at one diameter may hide a bend at another axial position.
| Control Item | Required Definition |
|---|---|
| Datum | Centers, selected journals, or specified reference diameters |
| Measuring diameters | Exact positions within the stated 14–23.5 mm range |
| Incoming limit | Maximum 0.5 mm runout; confirm whether this applies at every point |
| Final target | 0.2 mm OD runout; customer requirement, not yet an accepted result |
| Straightening positions | 1–5 approved axial press zones; not automatically identical to measuring points |
| Surface condition | Ra 1.25 μm and permitted support/probe/press contact areas |
| Final inspection | Same datum logic, rotation method, and filtering as the agreed customer gauge |
Why This Shaft and Bar Family Is Difficult to Straighten
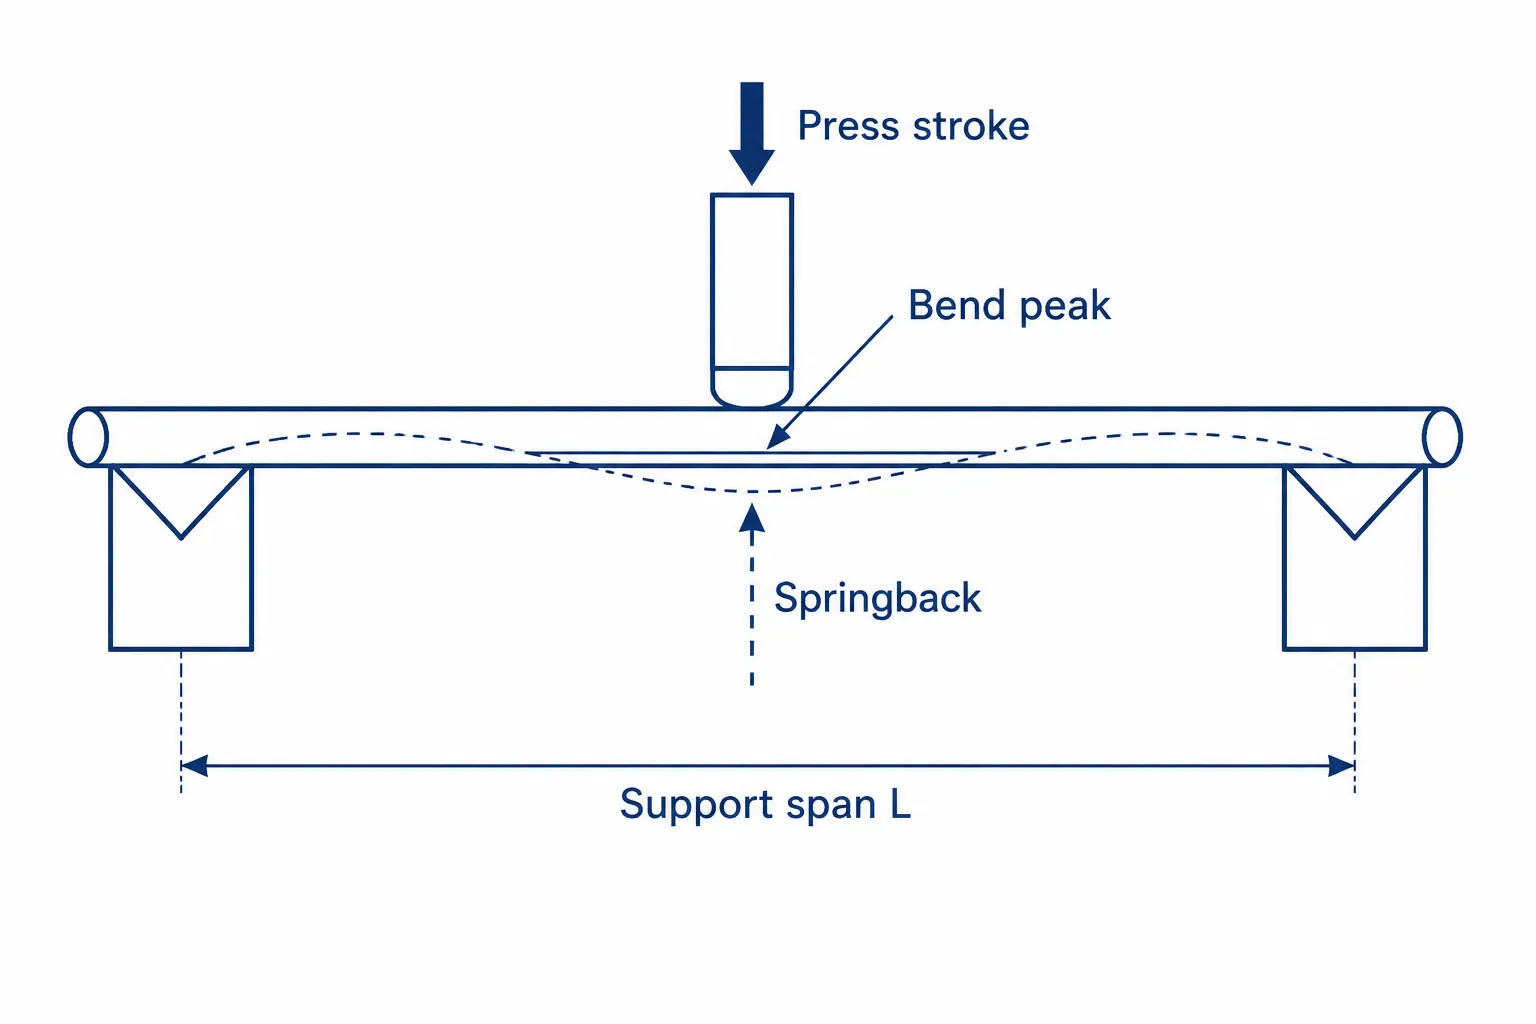
The length changes by almost four times across the family and the diameter envelope includes both measuring and non-measuring sections—a 720 mm part at the smaller diameter is much more flexible than a short part at the largest diameter, so one fixed support span or press stroke cannot cover the family safely. Hardness variation from HB 241 to 302 changes springback and the permanent correction produced by the same stroke, and the Ra 1.25 μm surface must remain free from unacceptable probe scratches, support marks, or press impressions.
| Workpiece-Specific Challenge | Risk | Required Control |
|---|---|---|
| 183–720 mm length range | Incorrect support span, unstable response | Model-specific support positions and recipes |
| Measuring vs non-measuring diameters | Probe on the wrong surface, datum mismatch | Drawing-based measuring-point definition and sensor travel |
| HB 241–302 hardness range | Variable springback, over-correction, crack risk | Adaptive stroke, conservative limits, batch/sample validation |
| Ra 1.25 μm surface | Contact marks, noisy measurement | Clean contoured supports, suitable probe force, approved contact zones |
| 1–5 correction positions | One press action changes neighboring points | Full-length measurement, validated correction sequence |
| Possible section transitions | Local stress concentration | No-press zones, suitable punch/support geometry |
| Competitor replacement request | Unsupported equivalence or price claim | Same-sample benchmark with agreed acceptance criteria |
Recommended Straightening Method
Automatic point press-straightening is the preferred starting method because the part is measured by radial runout at several possible axial locations: the system rotates the shaft, identifies bend magnitude and angular direction, positions the workpiece or press at an approved correction point, applies controlled over-bending, and repeats the complete measurement. A continuous roll straightener may be appropriate if the final workpiece is a constant-diameter bar with distributed curvature and a throughput requirement that favors through-feed processing; it is less suitable when the part has several diameters, protected finished surfaces, or specific 1–5 press zones. If the actual part is hollow tube rather than solid shaft/bar, wall thickness, inside diameter, and collapse/ovality limits must be added before the method is selected—see the tube straightening machine line for that workpiece family.
Proposed Automatic Straightening Process
| Step | Process | Engineering Purpose |
|---|---|---|
| 1 | Part identification and recipe selection | Match length, diameters, datum, points, limits |
| 2 | Feeding and singulation | Transfer one cylindrical part without scratching or double-feeding |
| 3 | Datum positioning and rotation | Establish a repeatable axis for runout measurement |
| 4 | Initial multi-point measurement | Record incoming runout at every required diameter |
| 5 | Signal validation and bend calculation | Separate real bend from roughness, eccentricity, feature effects |
| 6 | Correction-point and angular positioning | Align one of the approved 1–5 press zones with the ram |
| 7 | Controlled over-bending | Compensate springback within force/stroke limits |
| 8 | Complete remeasurement | Evaluate all points after each correction |
| 9 | Adaptive correction or NOK decision | Continue only inside the validated process window |
| 10 | Final sorting and data record | Separate OK/NOK parts, retain required quality values |
Feeding and model control
A staging tray or magazine can present cylindrical parts to the station. Guide rails, separators, and contact materials must cover the 14–28.5 mm diameter envelope without jamming, mixing two parts, or damaging the Ra 1.25 μm surface. Mixed models require recipe verification through part ID, length check, diameter check, or an equivalent poka-yoke method. The final feed system should be validated using the shortest, longest, smallest, and largest real variants.
Multi-point rotation and measurement
The part rotates on the agreed datum while contact probes or laser sensors collect runout at the specified measuring diameters. Probe force, sensor range, and filtering are selected for the surface and rotational speed; surface roughness, roundness error, or contamination must not be mistaken for shaft bend. The 1–5 straightening positions are mapped separately from measuring points—a probe may measure a functional journal while the safest press location lies on a neighboring, stronger section, and the controller must use the drawing relationship between these points rather than pressing directly at every measured maximum.
Bend calculation and controlled over-bending
The control identifies the dominant bend vector and selects a correction sequence. Over-bending moves the part beyond the desired final position so elastic springback returns it closer to target. Initial stroke limits should be conservative—especially near the HB 302 end of the material range—and refined from the measured response of representative samples. Where force measurement is available, force/displacement behavior provides an additional abnormal-response limit; the system stops if the response differs substantially from the validated recipe, the maximum correction count is reached, or the part fails to converge safely.
Complete remeasurement and final decision
After every press action, all required measuring points are checked again on the same datum—a local improvement is not enough if another diameter moves outside tolerance. The final OK decision requires the complete set of specified points to meet the customer criterion. Quality records may include model ID, incoming and final runout, measuring-point results, correction positions/count, recipe version, and final classification, scoped to the customer’s traceability requirement.
Replacing Existing Equipment: Use a Controlled Benchmark
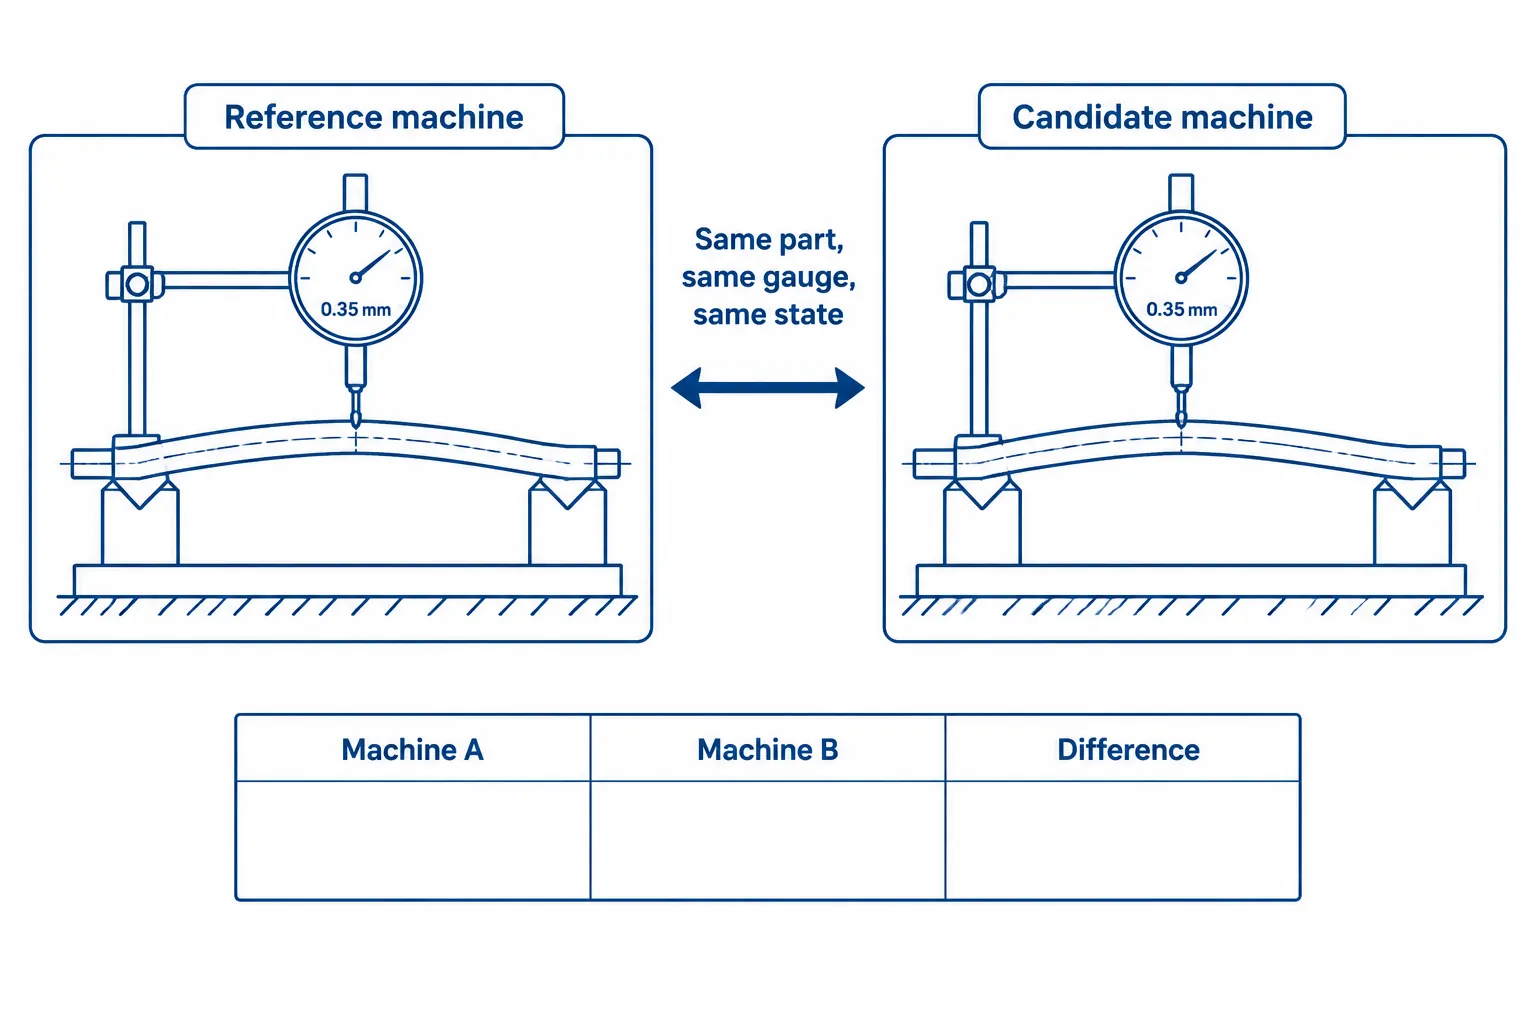
When a buyer is evaluating an alternative to existing straightening equipment, it is not technically sound to claim identical performance or a fixed price reduction without comparing the same workpieces, measuring method, automation scope, tooling, and lifecycle support. A defensible replacement decision uses:
| Benchmark Item | Required Comparison |
|---|---|
| Workpiece set | Same shortest/longest, smallest/largest, worst-bend samples |
| Datum and gauge | Same support, rotation, probes, acceptance calculation |
| Quality | Final runout at every required point; surface and crack condition |
| Process | Correction count, cycle time, repeatability, NOK rate |
| Changeover | Tooling, recipe, operator time for all models |
| Automation | Feeding, sorting, traceability, plant interfaces in both scopes |
| Ownership cost | Equipment, tooling, installation, training, maintenance, spares, downtime assumptions |
| Acceptance | Written FAT/SAT criteria rather than an unsupported equivalence statement |
Recommended Cell Configuration
| Module | Proposed Requirement | Why It Is Needed |
|---|---|---|
| Machine concept | Automatic rotating point press-straightening cell | Closed-loop correction for multi-point shaft runout |
| Workpiece envelope | Length 183–720 mm; measuring OD 14–23.5 mm; other OD up to 28.5 mm | Covers the stated project family, subject to drawing review |
| Measuring system | Multi-point contact or laser runout measurement | Match datum, surface, sensor-travel requirements |
| Rotation / datum | Centers, rollers, or journal supports selected from the drawing | Repeatable angular bend measurement |
| Straightening unit | Fine-controlled servo/electromechanical/hydraulic press as sized | Manage springback across HB 241–302 |
| Supports and punch | Adjustable, contoured, surface-protective tooling | Cover length/diameter range, protect Ra 1.25 μm surfaces |
| Control strategy | Recipes, bend vector, adaptive stroke, hard iteration limits | Correct 1–5 points without uncontrolled repeated pressing |
| Feeding | Tray, magazine, or manual loading based on validated takt and part mix | Match production flow without assuming unsupported automation |
| Quality data | Before/after results, correction history as required | Benchmarking, acceptance, traceability |
| Safety | Guarding, interlocks, overload and abnormal-measurement alarms | Protect operator, part, tooling |
Project Validation Before Final Quotation
Representative samples should cover the minimum and maximum length, all measuring-diameter variants, normal and maximum incoming runout, HB 241 and HB 302 material conditions, every relevant heat-treatment batch, and all section transitions. The test report should record the datum, each measuring point, incoming value, correction position/count, final value, surface condition, and cycle time. The customer’s inspection gauge and the machine should be correlated before the 0.2 mm value becomes an acceptance guarantee; if the actual workpiece is hollow or contains hidden features, the drawing and sample review must revise the tooling and risk assessment before final machine selection.
Information Needed for a Proposal
Please provide the final workpiece name and application, drawing, material standard and certificate, hardness and heat-treatment stage, all diameters and feature positions, center holes/journals, incoming runout distribution, target at each measuring point, datum and gauge method, approved support/press zones, surface protection requirement, target takt, annual volume, loading direction, and representative sample parts. These inputs confirm whether the part is a solid shaft/bar or hollow tube, select the measuring and straightening method, size the force/stroke and tooling, and build an objective FAT/SAT benchmark.
FAQ
Is the target 0.2 mm straightness or radial runout?
The current input calls it outside-diameter runout. The drawing must confirm the datum, measuring positions, and rotation method; it should not be rewritten as straightness without that evidence.
Can the machine reduce maximum runout from 0.5 to 0.2 mm?
That is the project target, not yet a verified result. Feasibility depends on the datum, geometry, hardness, bend distribution, approved correction zones, and sample-test response.
Can one machine handle lengths from 183 to 720 mm?
Potentially, if the support travel, measuring positions, press axis, feeding system, and recipes cover the full range. The endpoint variants must be included in validation.
How is the Ra 1.25 μm surface protected?
The solution uses clean contoured supports, controlled probe force, and drawing-approved contact/press zones. Surface inspection remains part of the sample-test acceptance plan.
Why are 1–5 straightening points important?
They indicate that different models or bend profiles may require different correction locations. The machine must remeasure all controlled diameters after each correction because improving one point can change another.
Can this equipment be presented as equal to an existing competitor at a fixed lower price?
Only after a controlled same-sample benchmark and a comparable commercial scope. Quality, cycle time, tooling, automation, service, and lifecycle cost must be compared using written acceptance criteria.
Conclusion
This steel shaft/bar machine is defined by multi-diameter runout measurement, 1–5 controlled correction positions, HB 241–302 springback management, and protection of the Ra 1.25 μm surface. A reliable solution measures the complete part on the functional datum, corrects only approved zones, and verifies every point after each press action. The same automatic platform covers dedicated workpiece families—bolts, ball screws, worm shafts, and splined shafts. Send your drawings, material/hardness certificates, incoming runout data, acceptance definition, part mix, and sample information via the contact page for a feasibility and benchmark review—final performance is agreed through objective FAT/SAT criteria rather than unverified equivalence or price statements.