
Large seamless steel pipes pick up global bow, local bends and handling deformation through rolling, heat treatment, transport and storage. A pipe that is not straight enough creates downstream problems in machining, welding, inspection, coating, assembly and field installation. And because these pipes are long and heavy, the correction process must first learn to tell actual deformation apart from the deflection the pipe’s own weight produces on any support layout.
The solution outlined here is based on a customer range running from OD 127 mm × 9.525 mm wall to OD 349.25 mm × 38.1 mm wall, with lengths from 1,828.8 to 12,192 mm. It combines controlled support, full-length measurement, hydraulic point press-straightening and closed-loop remeasurement. One recorded requirement — “1 in 1000 mm” — must be clarified before quotation; this page provisionally reads it as a possible 1 mm deviation per 1000 mm gauge length, not as a one-inch tolerance.
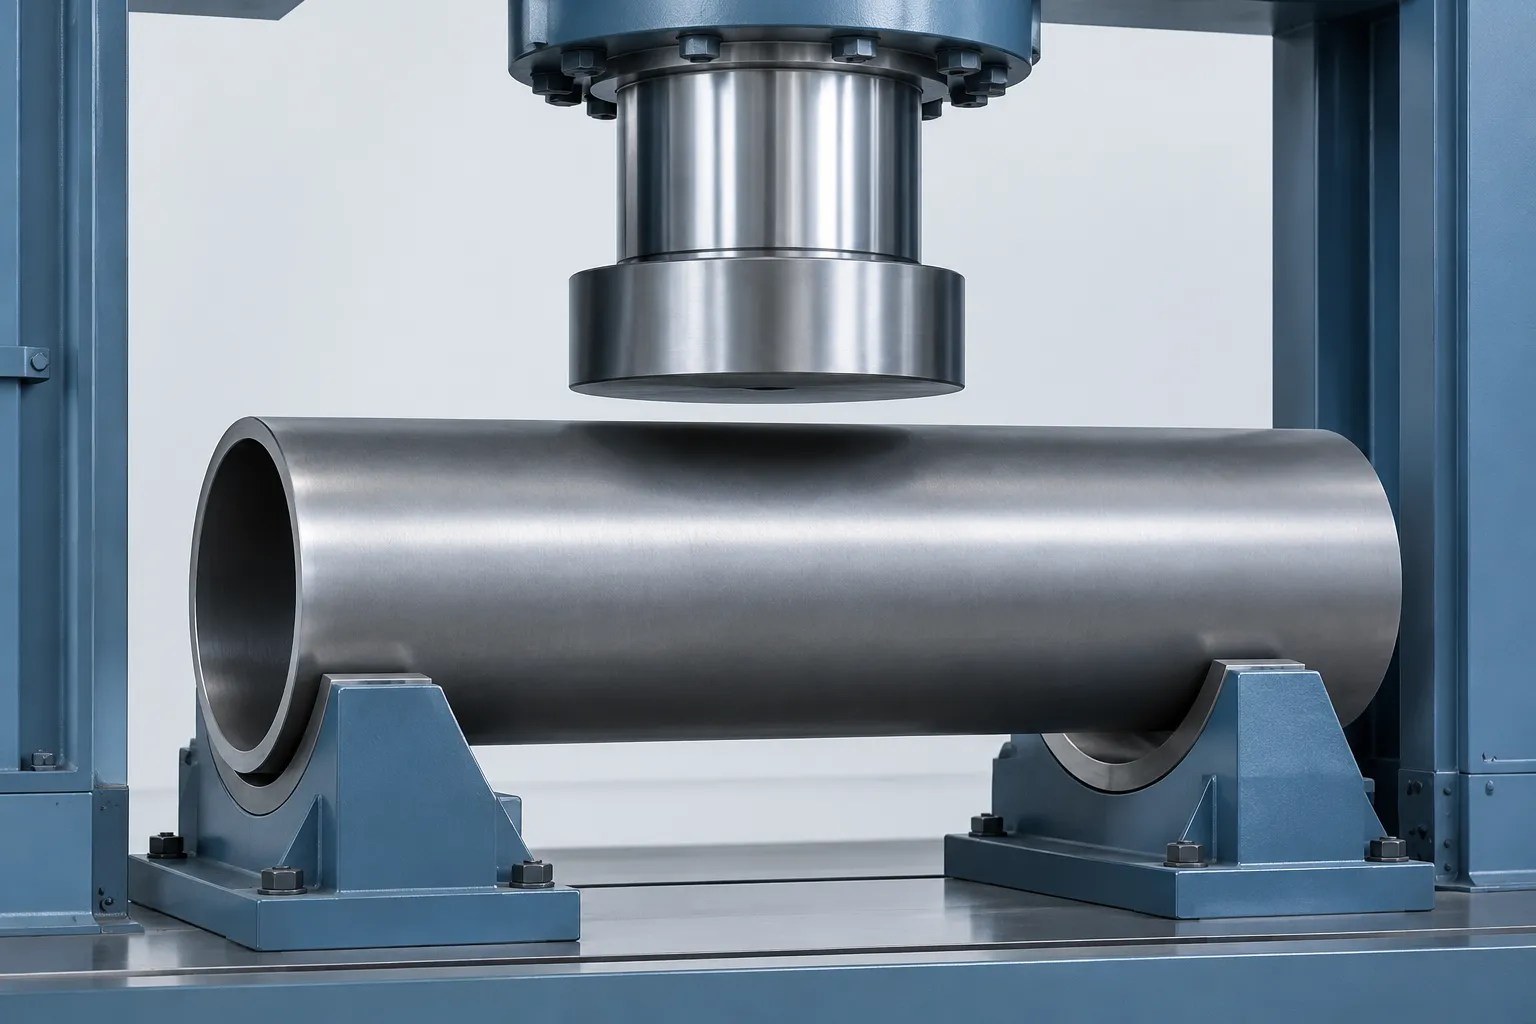
Engineering concept illustration of a heavy-duty hydraulic press correcting a large-diameter seamless steel pipe.
Seamless Steel Pipe and the Project Requirement
The project envelope is unusually wide. Outside diameter changes by almost three times, wall thickness by four times, and total length runs from roughly 1.8 to 12.2 m. Every one of those differences moves stiffness, self-weight, support spacing, measuring method, required correction force and material handling.
Taking 7,850 kg/m³ purely as a preliminary steel-density estimate, the smallest stated size at the shortest stated length weighs approximately 50 kg, while the largest stated size at the longest stated length would reach approximately 3,564 kg if those maxima ever occur together. The real part schedule, steel grade and certified weights are required before the loading and support system can be sized.
| Project Item | Customer Input / Status |
|---|---|
| Workpiece | Seamless steel pipe |
| Outside diameter | 127–349.25 mm |
| Wall thickness | 9.525–38.1 mm |
| Length | 1,828.8–12,192 mm |
| Material grade / yield strength | Not yet provided |
| Incoming deformation | Range and bend distribution not yet provided |
| Recorded straightness | “1 in 1000 mm” — unit, gauge length and acceptance method to be confirmed |
| Current method | Skilled manual straightening reported by the customer |
| Main goal | Cut production time and reduce dependence on highly experienced manual correction |
| Proposed method | Heavy-duty hydraulic point press-straightening with measured support and remeasurement |
| Machine model / rated force | To be confirmed by engineering calculation and representative sample testing |
Define Local and Overall Straightness Before Selecting the Machine
A requirement phrased as “1 mm per 1000 mm” normally describes a local straightness check over a defined gauge length. It does not automatically cap the maximum deviation over a complete 12.2 m pipe. Overall straightness may be assessed against a chord, a laser reference, specified supports or another standard method. The two controls can produce different acceptance verdicts and must not be merged into a single number.
The inspection condition must also fix pipe orientation and support positions. A long pipe sags under gravity; if the machine supports it at different points from the customer’s inspection station, the two systems report different values even when neither measurement is wrong. Gauge correlation therefore demands the same datum logic, an agreed support layout, and a repeatable method for separating self-weight deflection from permanent bend.
| Control Item | Required Definition |
|---|---|
| Local straightness | Allowed deviation and exact gauge length, potentially 1000 mm |
| Overall straightness | Full-length chord/axis requirement and measurement method |
| Measuring datum | Pipe OD, centerline, reference generators or specified end features |
| Support condition | Number, position, height and contact type of supports |
| Orientation | Fixed clocking position, or rotation through defined angles |
| Ovality / diameter | Required only if the drawing or standard controls it |
| Surface acceptance | No unacceptable dents, local flattening or support/press marks |
Why Large Seamless Pipes Are Difficult to Straighten
The workpiece is hollow, so the press never acts on a solid section. A narrow punch or a misplaced support can leave local indentation, flattening or ovality behind even while the longitudinal bow improves. Contoured saddles must spread contact over a suitable area, and the permitted contact stress must be validated for the actual OD, wall thickness, grade and temperature. The same section-preservation rules, scaled down, govern thin-wall tube straightening.
Length and weight add the second challenge. A 12 m pipe is not a short part sitting between two fixed supports. Multiple powered or adjustable supports may be needed to control sag, move the pipe through measuring and pressing positions, and prevent uncontrolled rolling. The support system is part of the metrology and straightening process — not just material handling.
| Workpiece-Specific Challenge | Risk | Required Control |
|---|---|---|
| Hollow circular section | Denting, flattening or ovality during point pressing | Wide contoured press shoe and saddles; force/stroke limits |
| 1.8–12.2 m length range | Self-weight creates false straightness readings | Defined support model and repeatable full-length measurement |
| Up to OD 349.25 × 38.1 mm | High and variable correction force | Grade/yield data, bend profile, calculation and sample validation |
| Potential multi-ton part | Unsafe or slow manual positioning | Powered rollers, anti-roll devices, crane/gantry interface, guarded movement |
| Several local bends | One correction shifts neighboring sections | Full-length bend map and controlled correction sequence |
| Wide size family | Excessive changeover or wrong tooling | Size-specific recipes, adjustable supports, verified tooling set |
| Skilled manual process today | Operator-dependent press point and stroke | Measured bend location, controlled correction, repeat verification |
Recommended Straightening Method
For large pipes with localized or multi-point bow, a hydraulic three-point press-straightening concept is the preferred starting point. The pipe rests on two or more controlled saddles, the bend profile is measured, and a hydraulic ram applies an over-bending stroke at an approved location. Depending on the final layout, the pipe indexes through a stationary press frame, or the press and measuring frame travel along the pipe.
A multi-roll straightener makes more sense for continuous production of uniform pipe sizes with distributed curvature. It is not automatically the right choice for a wide mix of large diameters, thick walls and localized bends. Final method selection weighs throughput, size mix, material grade, incoming deformation, ovality risk and whether the pipe can be rotated safely — the same family of trade-offs that separates roller straightening for long steel bars from press correction. Oil tubing and casing follow a related OCTG-specific route of their own.
Proposed Automatic Straightening Process
| Step | Process | Engineering Purpose |
|---|---|---|
| 1 | Pipe identification and recipe selection | Match OD, wall, length, grade, tolerance and tooling |
| 2 | Loading and anti-roll positioning | Transfer a heavy pipe safely onto controlled supports |
| 3 | Support-height setup and datum establishment | Create a repeatable condition for long-pipe measurement |
| 4 | Initial full-length measurement | Map local and overall bend before any correction |
| 5 | Bend calculation and correction sequencing | Select press point, support span, orientation and initial stroke |
| 6 | Pipe or frame indexing | Bring the selected bend under the hydraulic correction station |
| 7 | Controlled hydraulic over-bending | Correct the pipe inside force, stroke and ovality limits |
| 8 | Remeasurement and adaptive correction | Close the loop, or stop at the validated process limit |
| 9 | Final straightness/ovality inspection | Verify every required characteristic with the agreed method |
| 10 | Data recording and unloading | Store results and move OK/NOK pipes safely out of the cell |
Loading, Support and Positioning
The pipe arrives by crane, gantry, walking beam or powered roller system according to its real weight and the plant flow. Anti-roll devices and positive stops are essential, because a large round workpiece can move unexpectedly on any incline. Supports should adjust in position and height and carry replaceable, contoured contact surfaces matched to the pipe finish.
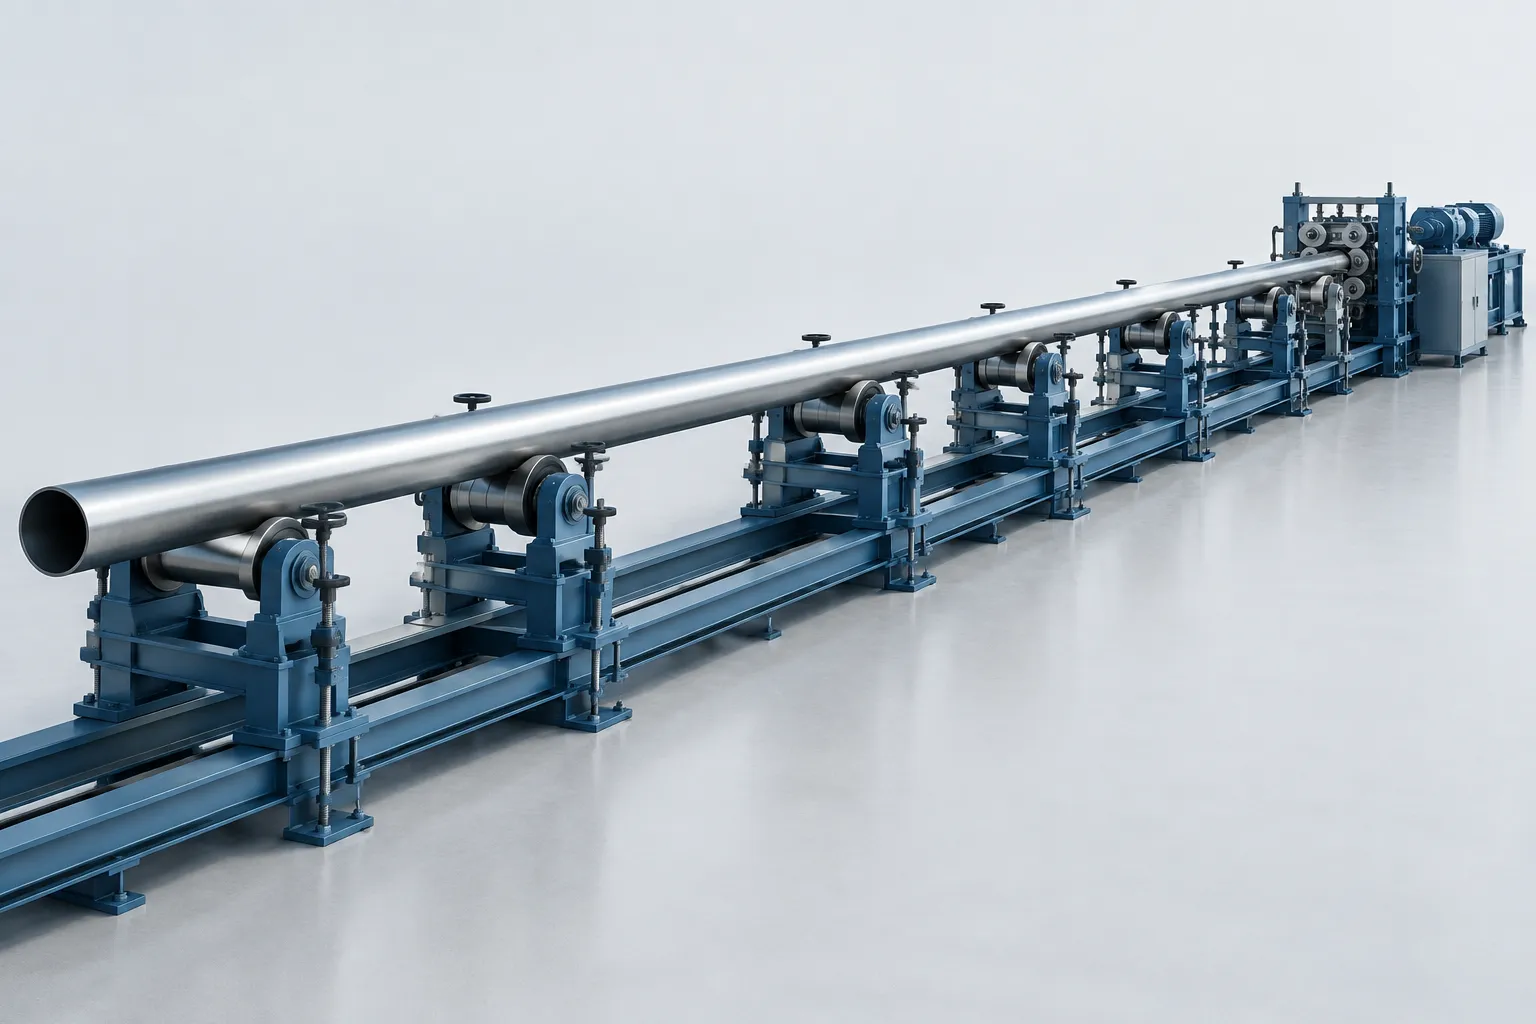
Engineering concept illustration — a long seamless steel pipe supported through a hydraulic straightening station.
On parts this long, support deflection and foundation level influence the measurement. Commissioning must include support alignment, repeatability checks and a defined zero/reference procedure before production recipes are accepted.
Full-Length Bend Measurement
The measuring system may use laser scanning, contact displacement sensors or another validated method to record the pipe profile along its full length. The measurement plan states resolution, gauge length, support condition, surface handling, and whether the pipe is measured at one clock position or rotated to separate multi-plane bend from ovality.
Where the customer uses a string line, straightedge or offline laser station, the automatic machine result should be compared against that method on the same sample set. The target is not only repeatability inside the machine — it is agreement with the final acceptance method.
Hydraulic Correction with Section Protection
The controller selects a correction point and support span from the measured bend. A contoured press shoe distributes load across the pipe surface while two or more saddles provide the reaction points. The stroke must exceed elastic deflection enough to produce controlled permanent correction, yet stay below limits that could dent, flatten or crack the pipe.
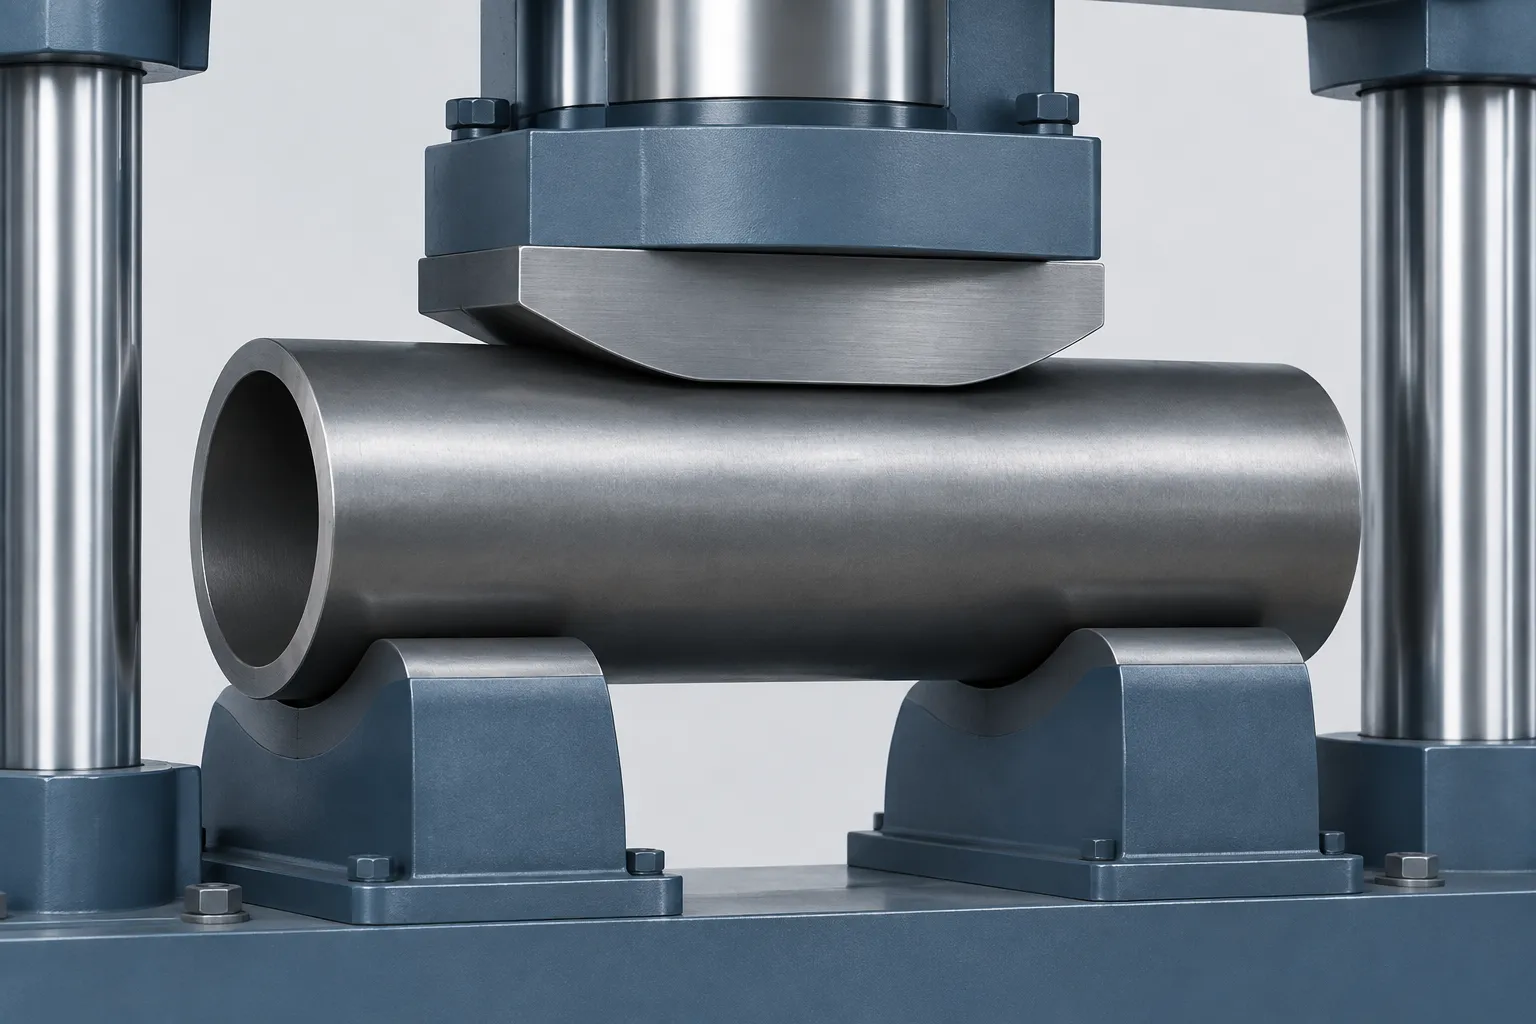
Engineering concept illustration — hydraulic press head positioned above a large steel pipe on contoured saddles.
Rated force cannot be picked from outside diameter alone. It depends on wall thickness, steel grade and yield strength, support span, section modulus, incoming bend, desired residual result and allowable local stress. Initial force and stroke limits come from calculation, then from representative sample tests.
Remeasurement, Iteration Limits and NOK Handling
After correction the pipe is remeasured under the same support condition. If the result is still outside tolerance but the measured response is normal and the recipe remains within its validated limits, the system may calculate one more correction. Maximum stroke, force, correction count and abnormal-response rules prevent uncontrolled repeated pressing.
A pipe that cannot reach the target safely is classified NOK or routed to engineering review. When project traceability requires it, the machine retains the before/after profile, correction positions, strokes and forces where available, the recipe version and the final decision.
Recommended Cell Configuration
| Module | Proposed Requirement | Why It Is Needed |
|---|---|---|
| Machine concept | Heavy-duty hydraulic three-point pipe straightening press | Local, controlled correction for large hollow sections |
| Workpiece envelope | OD 127–349.25 mm; wall 9.525–38.1 mm; length 1,828.8–12,192 mm | Covers the stated project range, subject to size-schedule confirmation |
| Rated force / stroke | Sized by calculation and sample test | Prevent undersizing, excessive stress or a misleading model choice |
| Measuring system | Full-length laser/contact profile measurement as validated | Distinguish local from overall bend and support closed-loop correction |
| Supports | Powered/adjustable contoured saddles with defined height and spacing | Control self-weight and protect the pipe surface |
| Positioning | Powered rollers, indexing drive or movable press frame | Bring each measured bend to the correction point safely |
| Tooling | OD-specific press shoes and saddles | Reduce indentation and ovality risk |
| Controls | Size recipes, bend map, correction limits, remeasurement logic | Reduce dependence on manual judgment |
| Handling | Crane/gantry/walking beam/roller interface with anti-roll control | Manage a part range that may extend into multiple tonnes |
| Quality data | Initial/final profile, correction history, OK/NOK result as required | Process verification and traceability |
| Safety | Guarding, interlocked movement, overload protection, safe access | Protect operators around a heavy moving round workpiece |
Concepts of this scale line up with a large pipe straightening machine architecture; the final configuration is always set by the confirmed size schedule rather than the range endpoints alone.
Project Validation Before Final Quotation
The sample matrix should span the smallest and largest OD/wall combinations, the shortest and longest pipes, normal and worst-case bends, all relevant steel grades and any heat-treatment conditions. Each trial documents support positions, orientation, incoming profile, correction position, force/stroke where available, final profile, ovality and surface condition, and total cycle time.
Before the straightness target becomes a machine guarantee, the customer must confirm whether the recorded requirement means 1 mm per 1000 mm, another unit, or an overall straightness ratio. The machine and customer inspection methods are then correlated on the same samples.
Information Needed for a Seamless Pipe Straightening Proposal
Please provide the complete pipe schedule, material grade and yield strength, certified or calculated weight, OD and wall tolerances, incoming bend distribution, local and overall straightness requirements, inspection standard and gauge method, ovality limit, surface and marking restrictions, support condition, target cycle time, annual volume, plant layout, crane/roller interface and representative sample pipes.
These inputs let the solution team calculate force and support span, select the measuring principle, design contoured tooling, define handling and safety requirements, and validate the process before the final machine model and rated force are committed. Send the package through the contact page for a feasibility review.
FAQ
Does “1 in 1000 mm” mean one inch of bend per 1000 mm?
It is ambiguous and should not be read that way without confirmation. It was most likely intended as 1 mm per 1000 mm gauge length. The customer drawing or specification must define the unit, gauge length, support condition and inspection method.
Can one machine cover OD 127 to 349.25 mm and lengths up to 12.2 m?
Potentially — but the force range, press travel, support positions, measuring field, tooling changes and handling system must cover the full size schedule. A list of actual OD/wall/length combinations is required; range endpoints alone are not enough.
How is pipe flattening prevented during press straightening?
Through contoured press shoes and saddles, a controlled support span and validated force/stroke limits. Ovality and surface condition belong in the sample-test acceptance plan whenever they are functional requirements.
How does the machine compensate for the pipe’s own weight?
The pipe is measured under a defined, repeatable support condition. Support positions and heights are part of each recipe, and the machine result is correlated with the customer’s final inspection method.
Is the required machine tonnage already confirmed?
No. Rated force must be calculated from material grade, yield strength, section, support span and incoming bend, then validated with representative samples. No unverified model or tonnage is assigned on this page.
Can the system replace an experienced manual straightening operator?
It standardizes measurement, bend-location selection, correction limits, remeasurement and records. Operators remain necessary for material supply, tooling checks, inspection audits, maintenance and abnormal pipes, unless the complete cell is engineered for a different staffing model.
What is required before quotation?
The minimum useful package: pipe schedule, grade, weight, incoming bend, local/overall target, inspection method, ovality and surface limits, production target, plant layout and sample pipes.
Conclusion
Large seamless pipe straightening is a combined metrology, structural-correction and material-handling problem. The final result depends on controlling self-weight, mapping the full-length bend, distributing press contact across the hollow section, and repeating measurement under the same support condition every time.
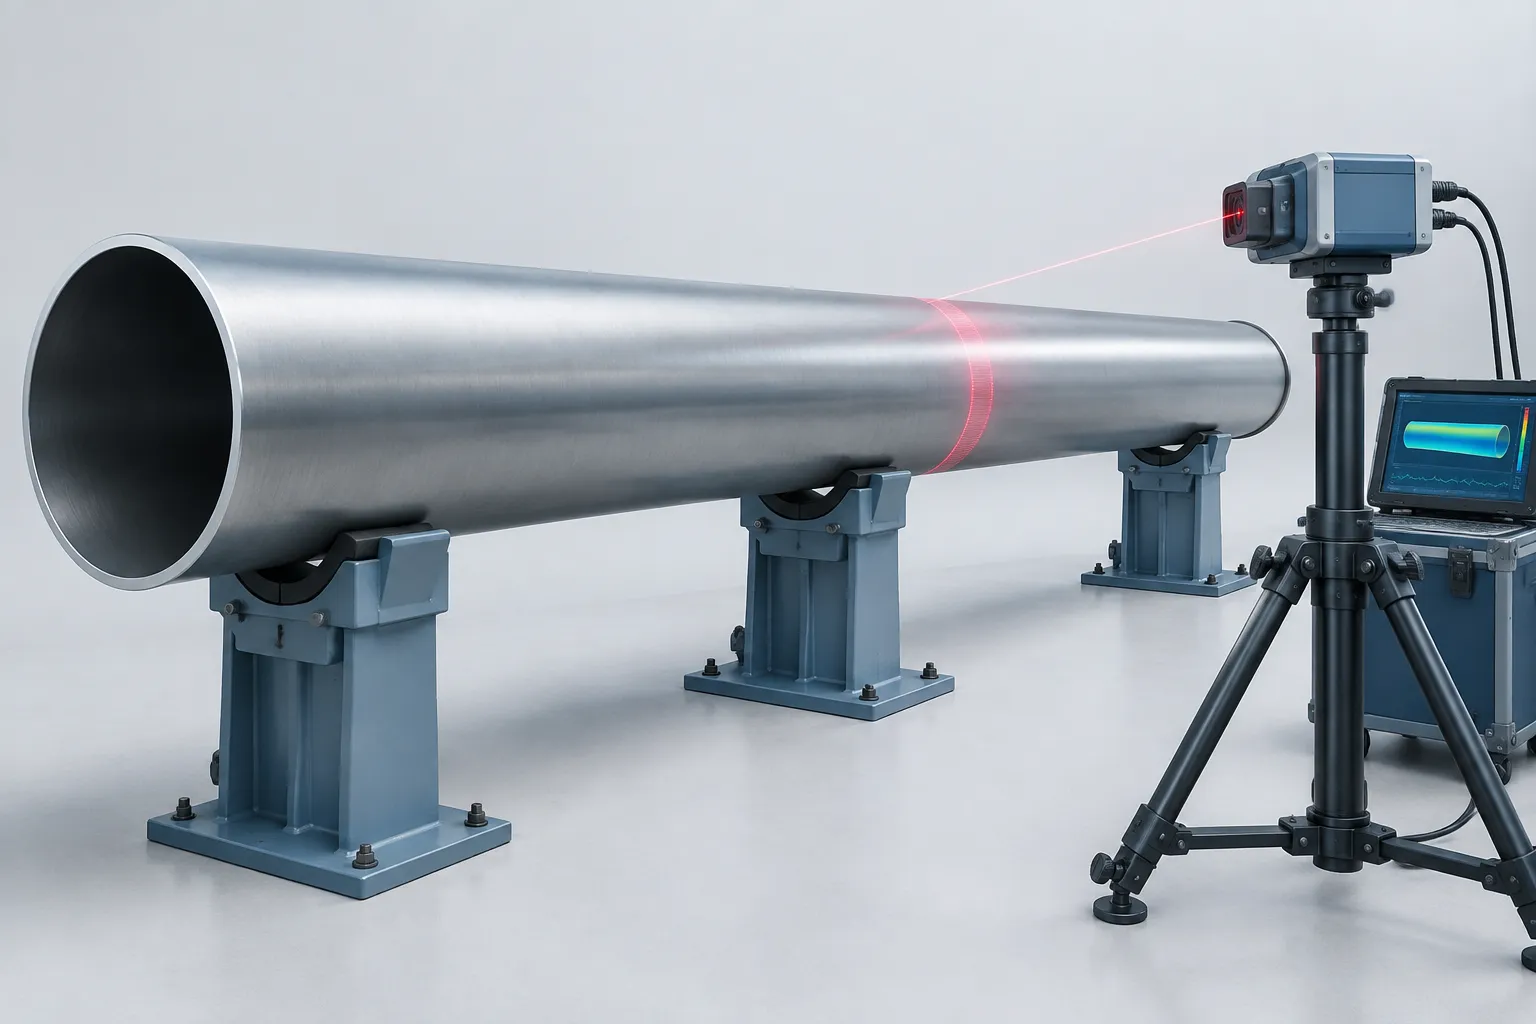
Engineering concept illustration — remeasurement of the released pipe under the same frozen support condition after hydraulic correction.
Send your pipe schedule, steel grade, incoming bend profile, straightness definition, production target and sample information for a feasibility review. The final press force, tooling, supports, measurement system and machine model should be confirmed through engineering calculation and representative sample trials — never assumed from a catalogue page.