
Input, output and intermediate gearbox shafts mix smooth bearing journals with gears, splines, shoulders, grooves, centre holes and the occasional radial oil hole. Heat treatment, rough machining, gear cutting and plain handling can leave behind a global bow or a local runout that resurfaces at grinding, gear inspection and assembly. Getting those shafts back inside tolerance is a measurement problem before it is a pressing problem.
One scoping note first: shafts whose integrated gear teeth are the functional feature of the single component, gear shafts proper, are covered on the gear shaft straightening page. This page deals with the shaft families inside a gearbox, where multi-journal measurement, family-level acceptance and line-rate economics dominate the engineering.
That means the part cannot be treated as a plain round bar. The process has to establish functional datums, separate journal runout from gear-related readings, keep fragile features out of the force path, apply a limited over-bend and then remeasure every controlled station. Force, support span, stroke, accuracy and cycle time all wait for confirmation from drawings and representative sample tests.
Why Gearbox Shafts Need Their Own Process
Primary and secondary transmission shafts usually need more than one correction position. Equipment makers publishing on this workpiece family describe two or three straightening points per shaft and gear pitch-diameter checking with a master gear; automated transmission-part lines add centre cleaning, complete measurement at multiple stations, crack-formation control and final remeasurement. Those are useful process references, not performance evidence for any particular machine on any particular customer part.
| Workpiece feature | Straightening consequence |
|---|---|
| Multiple bearing journals | Measurement must preserve the drawing datum relationship between journals |
| Helical or spur gear section | Tooth-tip readings cannot automatically be treated as shaft-centre runout |
| Spline | Needs functional measurement or a validated reference surface; teeth stay protected |
| Radial oil hole or cross-hole | Pressing across the hole creates a local stress concentration |
| Shoulders, grooves, fillets | Poor default support or press zones because stiffness changes locally |
| Heat-treated surface | Springback and crack risk evaluated by batch and process condition |
| Dirty or damaged centre holes | Centre-based measurement becomes unreliable until inspected and cleaned |
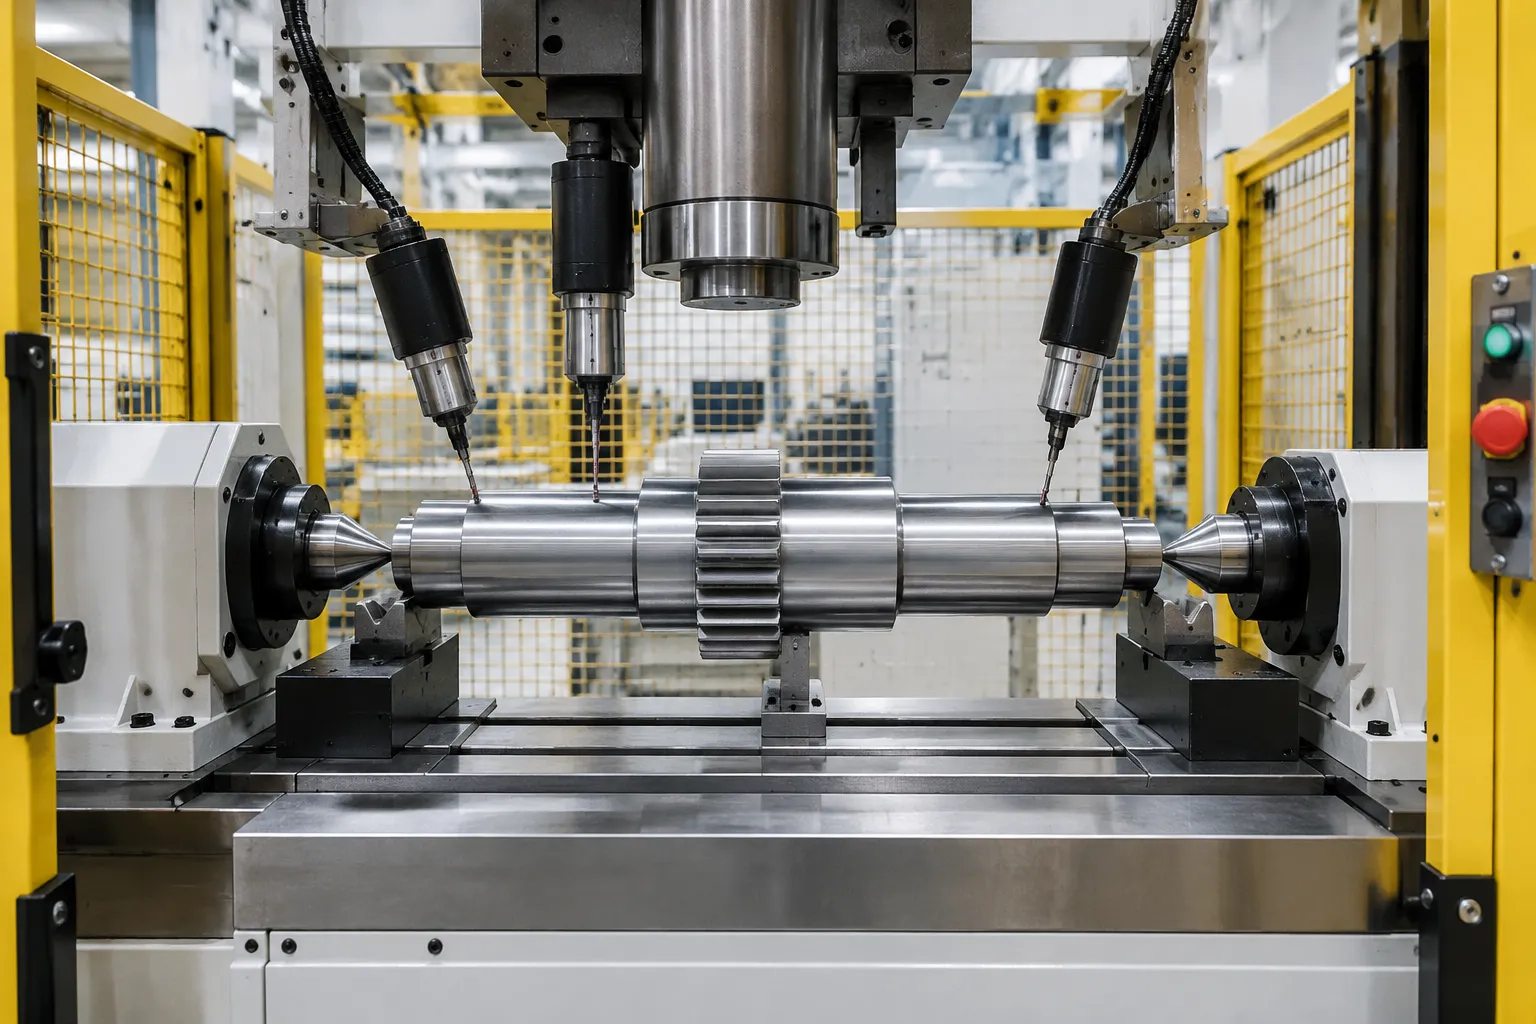
Concept illustration of a possible measurement and correction arrangement, not a customer-site photograph and not proof of any supplied machine configuration.
Define the Acceptance Characteristic Before Anything Else
Straightness, radial runout and TIR are different geometric controls, and gear pitch-diameter variation is yet another functional characteristic. A low indicator reading on one journal proves nothing about whether the gear, the spline and the remaining journals share the required axis. The drawing and the inspection plan decide what is controlled and which surfaces establish the datum, a distinction that matters for every shaft project from motor shaft straightening up to heavy transmission parts.
| Control item | Possible method | Datum / contact rule | Project status |
|---|---|---|---|
| Journal radial runout | Contact displacement probe or validated non-contact sensor | Rotate from drawing-defined centres or journals | Confirm from drawing |
| Axis straightness | Multi-station displacement measurement | Defined support condition and axial stations | Confirm from drawing |
| Gear pitch-diameter runout | Master gear, ball probe or validated laser method | Functional gear datum, controlled mesh | Confirm gear specification |
| Spline functional runout | Spline master or validated functional gauge | Never infer from tooth-tip contact alone | Confirm spline standard |
| Surface condition | Visual plus agreed surface inspection | All support, probe and press contact areas | Confirm acceptance sample |
| Crack control | Approved NDT method where required | High-stress zones, post-correction condition | Confirm risk and quality plan |
ISO 1101 supplies the general geometrical-tolerancing vocabulary, but it does not choose the correct datum or gauge for an individual gearbox shaft. The machine recipe has to match the controlled drawing revision and the customer’s own final inspection method.
Measurement Strategy for Journals, Gears and Splines
1. Establish a repeatable rotational datum
Use centre holes, finished journals or another drawing-defined datum only after confirming the surfaces are clean, undamaged and right for the manufacturing stage. Centre holes carrying heat-treatment residue can shift the apparent bend direction, which is why inspection or automatic cleaning may be needed before the first measurement.
2. Measure several axial stations
One probe cannot describe a stepped shaft. Measure the relevant journals and lands at fixed axial positions while the shaft rotates, and let the control system reject readings from grooves, reliefs, holes, keyways and interrupted surfaces instead of treating every peak as bending.
3. Evaluate the gear as a functional feature
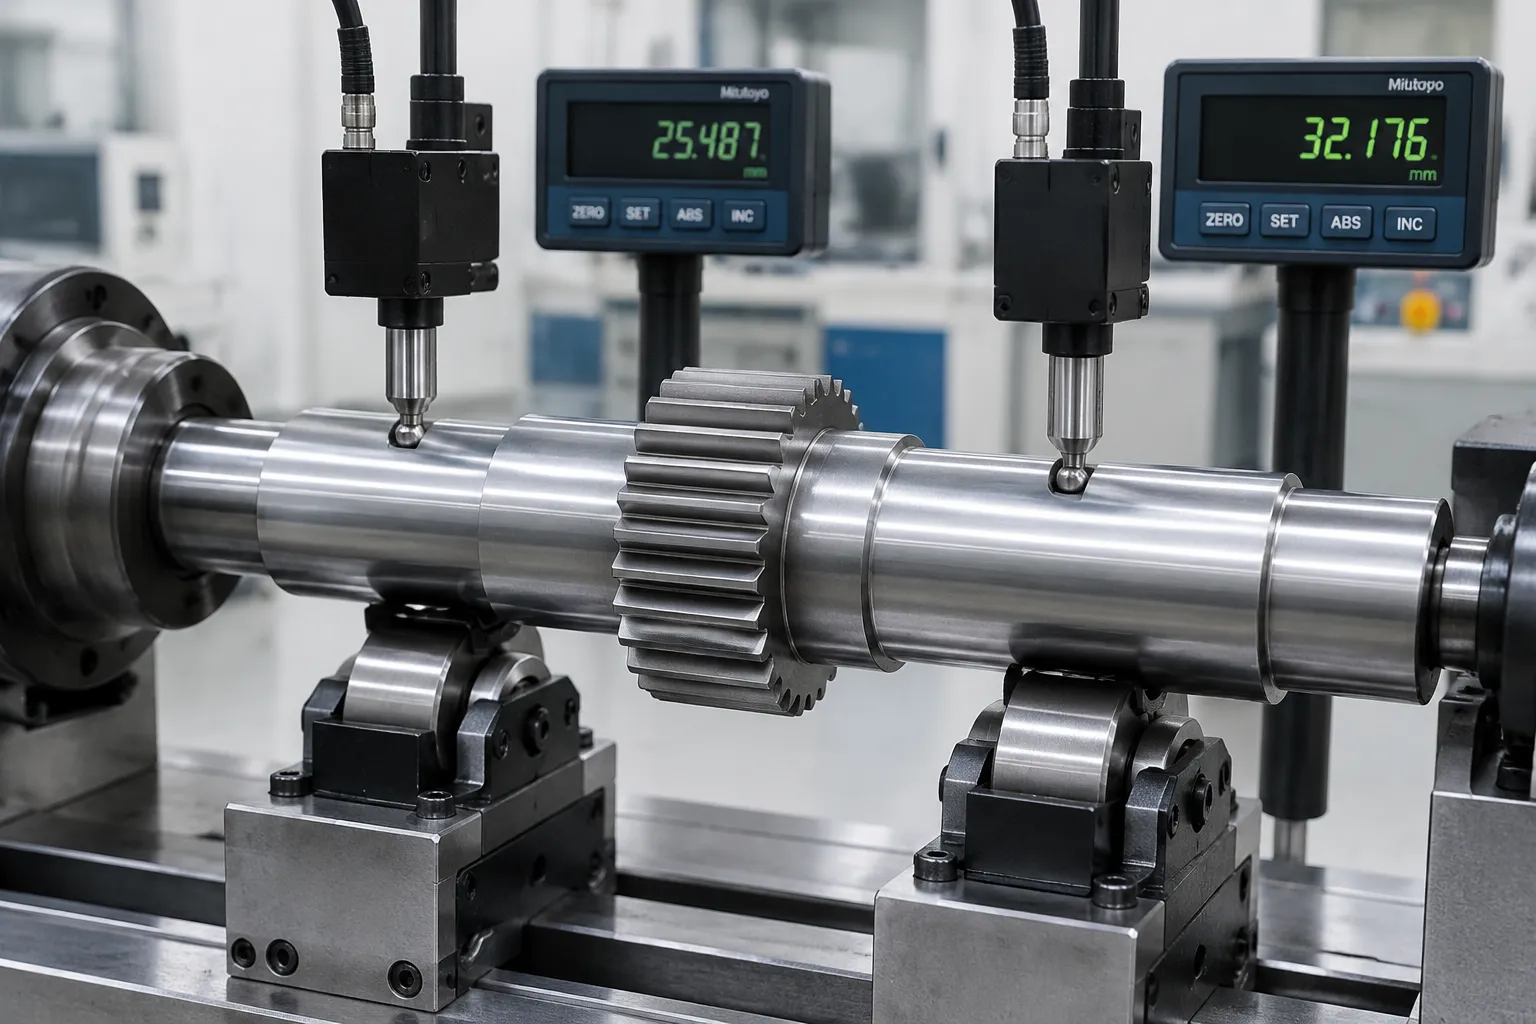
Concept illustration: smooth journals measured separately from the gear section, radial-hole position identified before a correction zone is chosen.
A master gear evaluates the pitch-diameter relationship under controlled mesh; tactile or laser alternatives suit other gear types. Whatever method is selected must be correlated with the customer’s gear inspection equipment, because a number that only one gauge believes is not an acceptance result.
Build a Protected Correction Map
The maximum measured deviation is not automatically the right press location. The algorithm chooses from approved correction lands and keeps high-risk features outside the support and press path:
| Zone | Default rule | Reason |
|---|---|---|
| Stable smooth cylindrical land | Candidate measurement, support or press zone after stress review | Predictable contact and section stiffness |
| Gear teeth and spline | No direct press contact | Profile damage and false functional geometry |
| Radial or cross-hole | Excluded from the primary force path | Local section loss and stress concentration |
| Shoulder, groove, fillet | Avoid unless specifically engineered | Abrupt stiffness change, marking risk |
| Finished bearing or seal journal | Contact only with validated protected tooling | Surface damage affects assembly and sealing |
| Hollow or deeply bored section | Verify section capacity before pressing | Local ovalization or collapse |
Radial-hole orientation can be detected before correction so the shaft is never loaded through its weakest angular position. Force and displacement limits should also end the cycle when the expected response stops appearing.
The Closed-Loop Process, Step by Step
For most stepped gearbox shafts with local bend, automatic point-press straightening beats a generic through-feed roller process: point correction reaches selected lands and keeps separate recipes for each shaft variant. Roller straightening can still serve simpler blanks before gear and spline features are finished, but it should never be assumed suitable for completed gearbox shafts.
- Identify the part and load its controlled recipe.
- Inspect or clean centre holes and approved datum surfaces.
- Locate the shaft axially and establish repeatable rotation.
- Measure every drawing-defined journal and functional gear station.
- Filter interrupted-surface effects; calculate bend magnitude and angular direction.
- Detect radial-hole orientation; exclude prohibited correction zones.
- Position supports and press tooling on approved lands.
- Apply a limited correction under force and displacement monitoring.
- Release the load and remeasure every affected station.
- Repeat only inside validated stroke, force and iteration limits.
- Complete final functional measurement, surface inspection and any required crack check.
- Record OK, NOK or engineering-review status together with recipe and results.
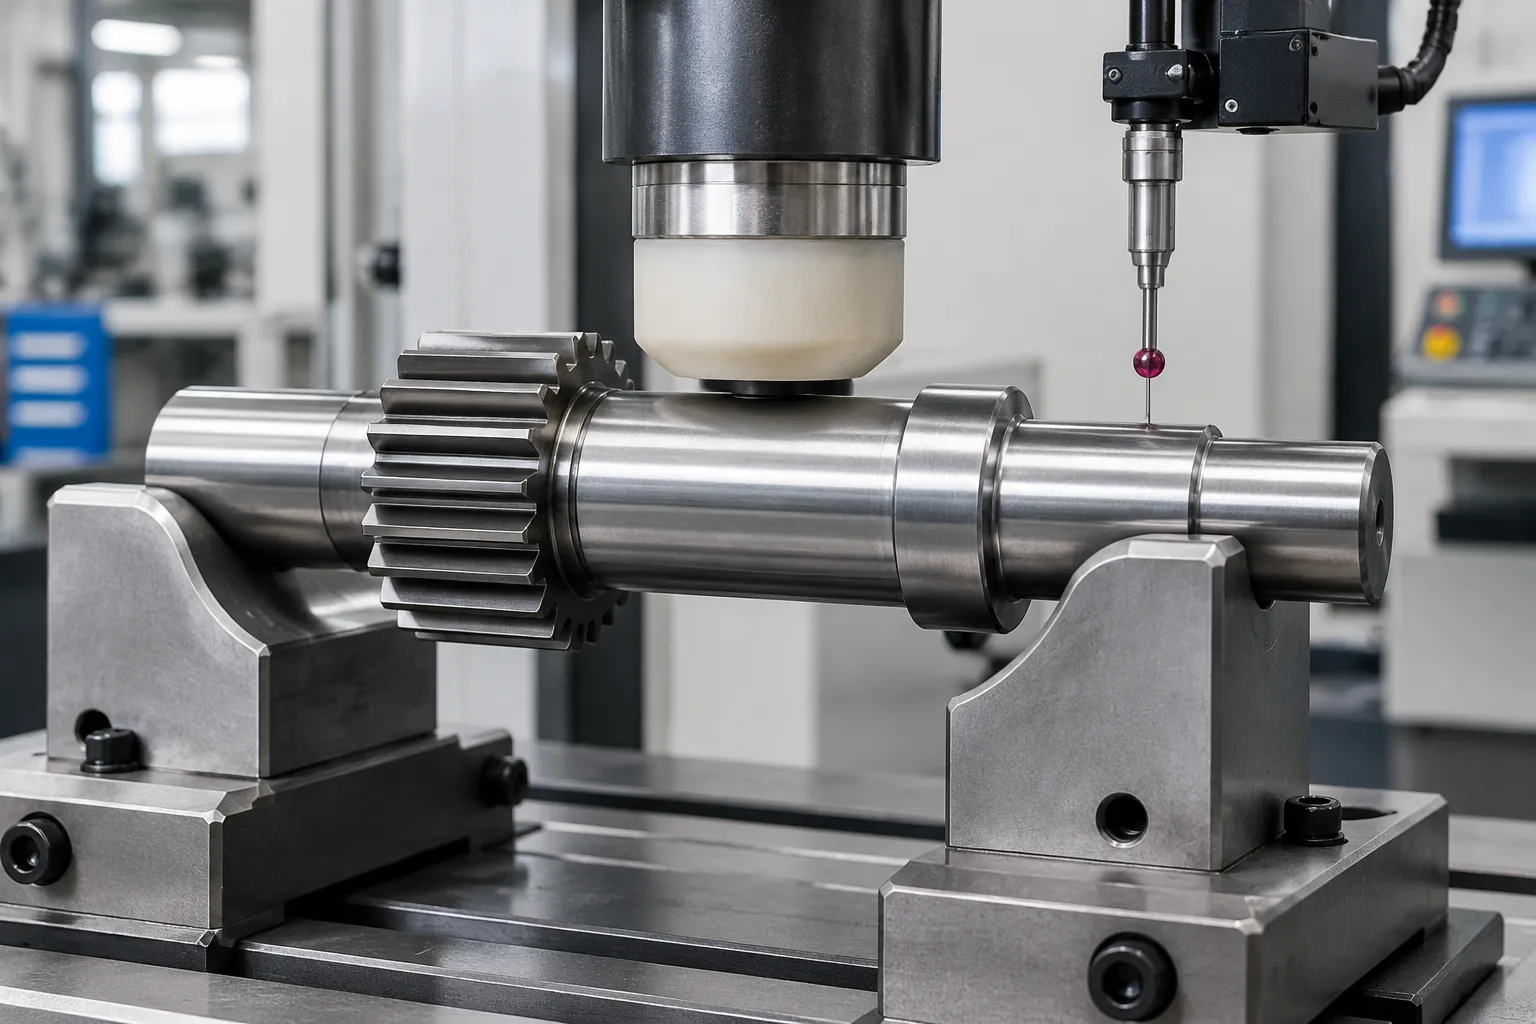
Concept illustration: press and supports act on smooth approved lands while teeth, splines, shoulders and cross-holes stay clear.
Springback and Crack-Risk Control
Heat-treatment condition, material strength, local section changes and incoming bend history all move springback. A fixed stroke copied across batches will under-correct one shaft and over-correct its neighbour. The controller should update the next stroke from the released, remeasured result, never from the loaded deflection alone.
Hard safety limits belong in the recipe: maximum force, displacement, iteration count and residual error, all set during sample development. When correction response turns non-linear, when a shaft exceeds its incoming-reject envelope, or when a protected feature threatens to enter the force path, the machine stops and routes the part to engineering review.
Crack control is application-specific: force-curve monitoring, surface inspection or a customer-approved NDT method. A straightening machine cannot claim zero cracks merely because a force limit exists.
Recommended Cell Configuration
| Module | Recommended concept | Engineering purpose |
|---|---|---|
| Machine principle | Servo-electric or servo-hydraulic point press | Controlled local correction with recipe limits |
| Datum and rotation | Centres, journal rollers or dedicated clamping | Repeatable angular measurement without feature damage |
| Journal measurement | Multiple contact probes or validated laser sensors | Map bend and runout at drawing-defined stations |
| Gear / spline measurement | Master gear, functional master, ball probe or validated laser | Measure the torque-transmitting feature correctly |
| Feature detection | Radial-hole and orientation sensor where required | Prevent pressing through fragile sections |
| Tooling | Adjustable contoured supports, protected press tips | Keep stress and contact marks within validated limits |
| Control | Recipe, filtering, adaptive stroke, iteration limits | Manage springback and part variants |
| Quality | Final remeasurement, OK/NOK sorting, data record | No unverified part flows downstream |
| Automation | Manual loading, conveyor, gantry or robot | Match volume, layout and changeover needs |
Machine sizing comes from the shaft drawing, material condition, maximum incoming bend and the sample-test force. Larger gate-style machines in the UBS20MF class exist for long, heavy transmission shafts; their suitability and any performance value require project-specific confirmation.
Sample Validation Plan
This page is a concept-level solution, not a manufacturing case study. Before any quotation or accuracy statement, samples must cover minimum and maximum shaft length, journal diameter, gear geometry, material strength, heat-treatment batch and incoming bend.
Record the controlled drawing revision, datum setup, incoming readings, correction position, force and displacement, iteration count, released final readings, surface condition and crack-inspection result. Machine and customer gauges must be correlated on the same parts. A published accuracy or cycle-time figure is only as good as the characteristic, sample count, gauge and acceptance record behind it.
Information Needed for a Proposal
- controlled part drawing and revision;
- shaft function: input, output, intermediate or pinion shaft;
- material, hardness and heat-treatment condition;
- manufacturing stage at straightening;
- total length, journal diameters, gear and spline data;
- centre-hole, radial-hole, groove and shoulder locations;
- incoming bend or runout distribution;
- drawing-defined datum and target characteristic;
- customer gauge or correlation samples;
- prohibited contact zones and surface criteria;
- production volume, cycle target and changeover matrix;
- loading, traceability and plant-layout requirements.
With those inputs the measurement method, force path, tooling, correction limits and sample-validation plan follow without inventing unsupported parameters. The same input discipline applies across the wider shaft portfolio described in the shaft-type parts straightening overview.
Frequently Asked Questions
Can a gearbox shaft be measured on its bearing journals alone?
Only when the drawing and downstream function allow it. Gear or spline runout may need a functional master or another validated method in addition to journal measurement.
Can the machine press directly on a gear or spline?
Normally no. Direct contact risks profile damage and builds an unreliable force path. Approved smooth lands and dedicated tooling are defined from the drawing.
How are radial oil holes protected?
The hole location is detected or mechanically indexed, and the recipe blocks press directions that load through the weakened section. The final rule is validated on representative parts.
What straightening accuracy can be guaranteed?
No universal value exists from the workpiece name alone. The achievable result depends on geometry, material, heat treatment, incoming deformation, datum, gauge correlation and the agreed sample test.
Does every shaft need crack detection?
No. Crack inspection follows the material, heat-treatment condition, correction strain and the customer quality plan. High-risk applications may need an integrated or downstream approved NDT method.
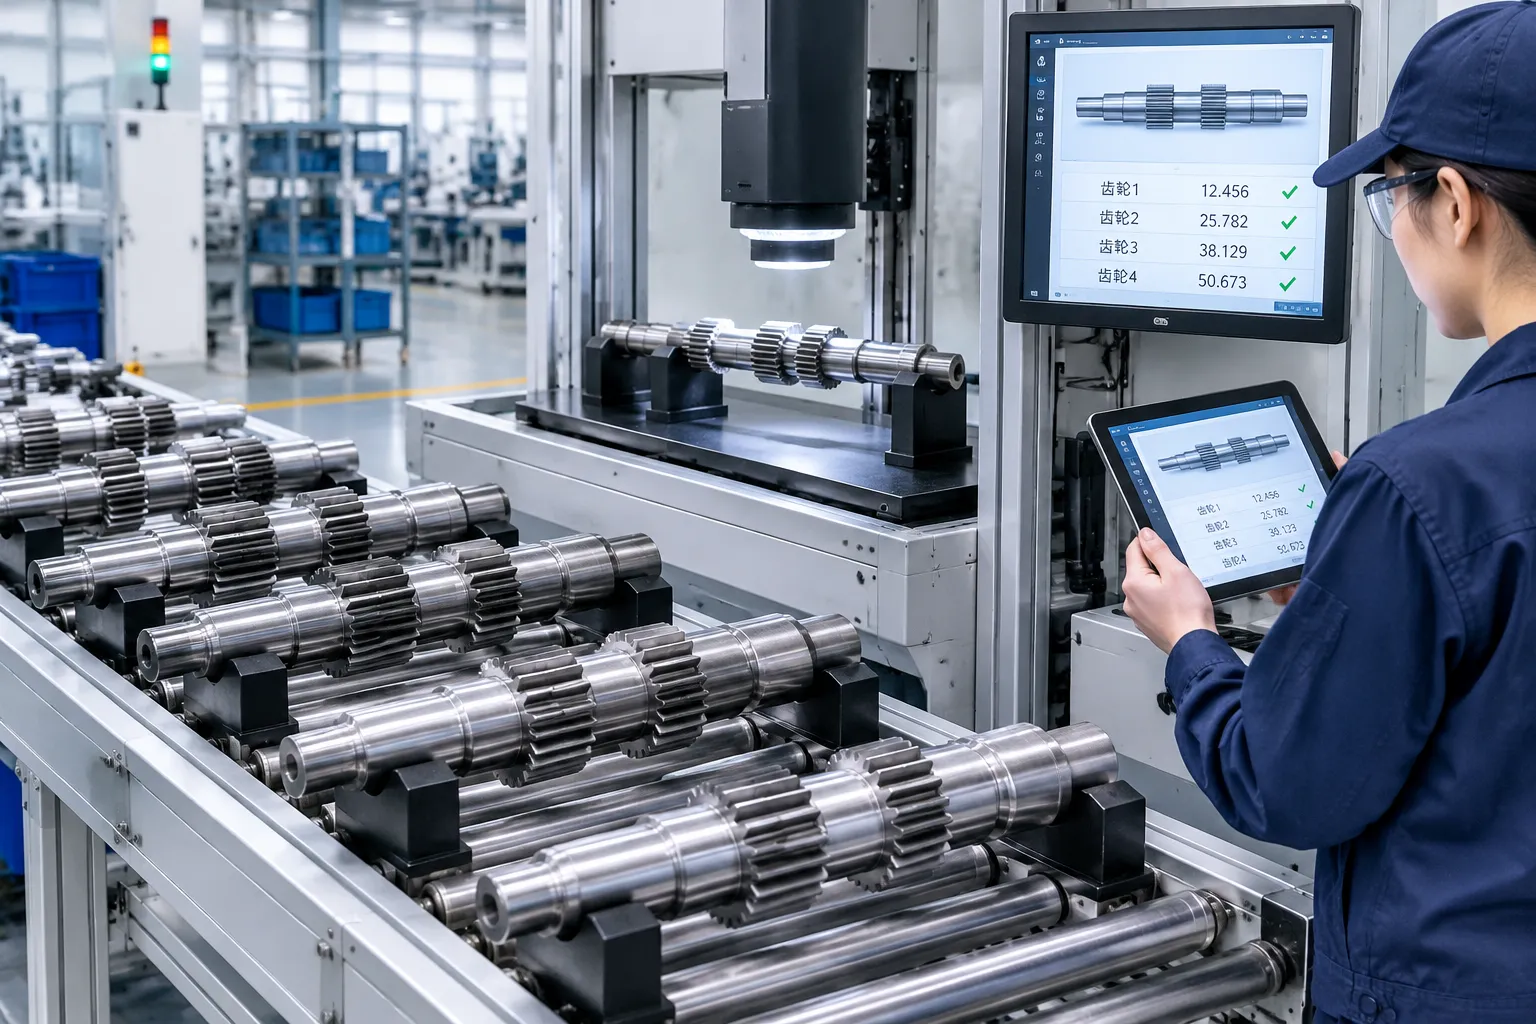
Start the Conversation With Data
Send the drawing set and a sample matrix through the contact page, and the engineering discussion starts from datums and gauges instead of adjectives. For a sense of how these shafts sit inside the wider machine portfolio, the shaft-type parts straightening overview collects the related workpiece families.