

A worm shaft straightening machine has to handle a workpiece that combines a slender small-diameter body with a functional worm thread and precision journals—the worst case for naive pressing, because the thread must never see contact load and the shaft itself is extremely sensitive to stroke. This page gives the tested machine specification and video first, then the complete engineering layer for small motor worm shaft straightening: datum selection, thread protection, springback control, the closed-loop cycle, and the validation plan that turns a demo into a production process.
Tested Specification and Machine Video
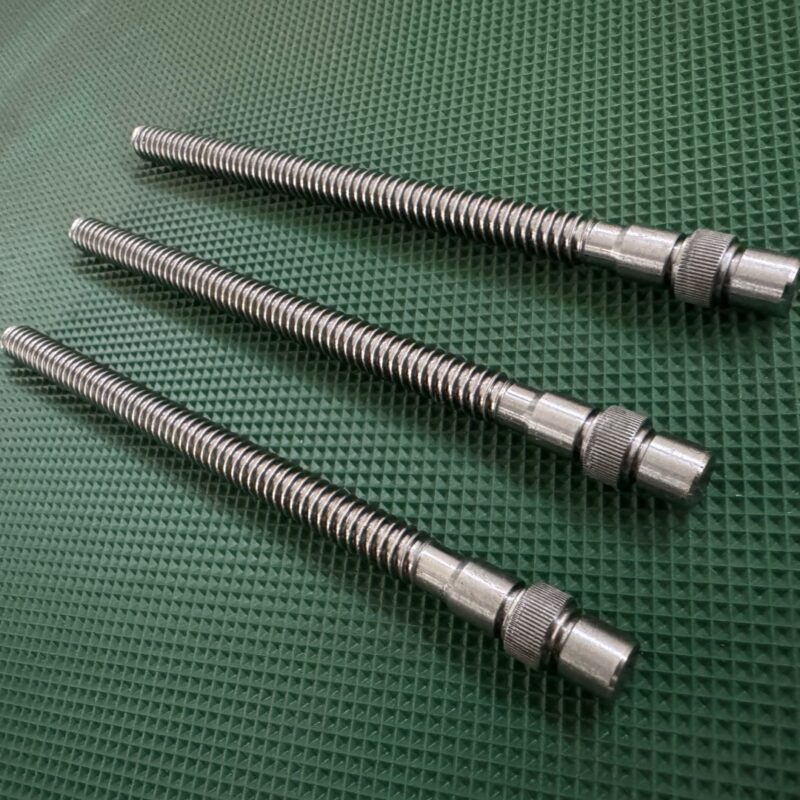
The tested worm shaft family for this trial: 8 mm diameter x 130 mm length, required straightness 0.01 mm, corrected on an AMS-PS300H precision automatic straightening machine. The video shows threaded worm shafts, the internal support and correction station, and parts moving through the machine in the closed measure–press–recheck loop.


What Is a Small Motor Worm Shaft and Why Does It Need Straightening?
Small motor worm shafts are used in compact gear motors, smart locks, appliance drives, and automotive actuators. A small motor worm shaft combines a motor shaft with a worm thread that drives a mating worm wheel; depending on the design it may also include bearing journals, shoulders, grooves, rotor seats, and assembly ends. These different diameters and functional features make the shaft harder to support and measure than a constant-diameter pin. The long, small-diameter body can bend after thread machining, heat treatment, grinding, or handling—and even a small deviation may affect bearing assembly, worm-wheel contact, noise, and rotational stability.
| Item | Project Input |
|---|---|
| Workpiece | Small motor worm shaft |
| Trial input (this page) | 8 mm x 130 mm; 0.01 mm straightness required, on AMS-PS300H |
| Functional features | Worm thread, slender shaft body, bearing journals, shoulders, assembly ends |
| Material / hardness | To be confirmed per project |
| Possible distortion sources | Thread machining, heat treatment, grinding, transport, storage |
| Main quality characteristic | Radial runout or straightness, as specified on the drawing |
| Measuring datum | Normally selected bearing journals, centers, or designated reference diameters |
| Protected areas | Worm thread, finished journals, grooves, shoulders, assembly surfaces |
| Production requirement | Part mix, takt time, annual volume, loading method to be confirmed |
Straightening Target and Acceptance Criteria
Straightness and radial runout are related but not interchangeable. Straightness describes deviation from an ideal straight line; radial runout is measured while the shaft rotates around defined references and includes the influence of the selected datum. The drawing and the customer’s inspection method must be reviewed before a target is entered into the machine recipe. For a stepped worm shaft, measuring on the thread or across a shoulder creates a misleading signal—stable cylindrical journals are normally better reference or measuring surfaces, provided they represent the functional assembly datum.
| Control Item | Requirement | Verification |
|---|---|---|
| Initial radial runout | Record actual incoming range | Rotate the shaft and measure at defined points |
| Final TIR / straightness | To be confirmed from drawing | Automatic remeasurement using the agreed datum |
| Worm thread protection | No unacceptable press or clamp damage | Visual and functional inspection as required |
| Journal surface protection | No unacceptable support marks | Visual or surface inspection |
| Correction limit | Maximum cycles and stroke set by sample test | Machine recipe and alarm logic |
Why Small Motor Worm Shafts Are Difficult to Straighten
The high length-to-diameter ratio makes the shaft sensitive to both real bending and measurement error. Dirt on the supports, unstable contact, self-weight, and an unsuitable measuring point can all change the reading, and the machine must distinguish the actual bend from variation caused by steps, grooves, or surface features. The correction window is also narrow: too little over-bending leaves residual runout, while too much can reverse the bend or overload a thread root, groove, or section transition. Support spacing, press position, press direction, and stroke cannot be copied from another shaft model without validation.
| Challenge | Cause | Control Strategy |
|---|---|---|
| Unstable measurement | Small diameter, surface contamination, poor support | Clean reference areas, precision supports, repeatable rotation |
| Signal variation | Steps, grooves, thread geometry | Measure on approved journals, filter feature-related variation |
| Springback | Material and hardness variation | Closed-loop correction with model-specific limits |
| Overcorrection | High sensitivity of the slender section | Fine displacement control and staged correction |
| Thread damage | Pressing or clamping on the worm profile | Define the worm section as a protected/no-press zone |
| Secondary bend | Incorrect support span or correction sequence | Validate support and press positions through sample testing |
Recommended Straightening Method
For this type of stepped, short, slender shaft, automatic point press-straightening with rotational runout measurement is generally more suitable than a continuous multi-roll process. Point correction lets the system use designated journals as references, avoid the worm thread, and apply a model-specific correction at selected axial and angular positions. A multi-roll or through-feed process may suit constant-section bars, wire, or uniform shafts, but it should not be assumed suitable for a worm shaft with steps and protected functional features. The final machine concept should be selected only after reviewing the part family, initial runout distribution, tolerance, volume, and required changeover time.
Closed-Loop Automatic Straightening Process
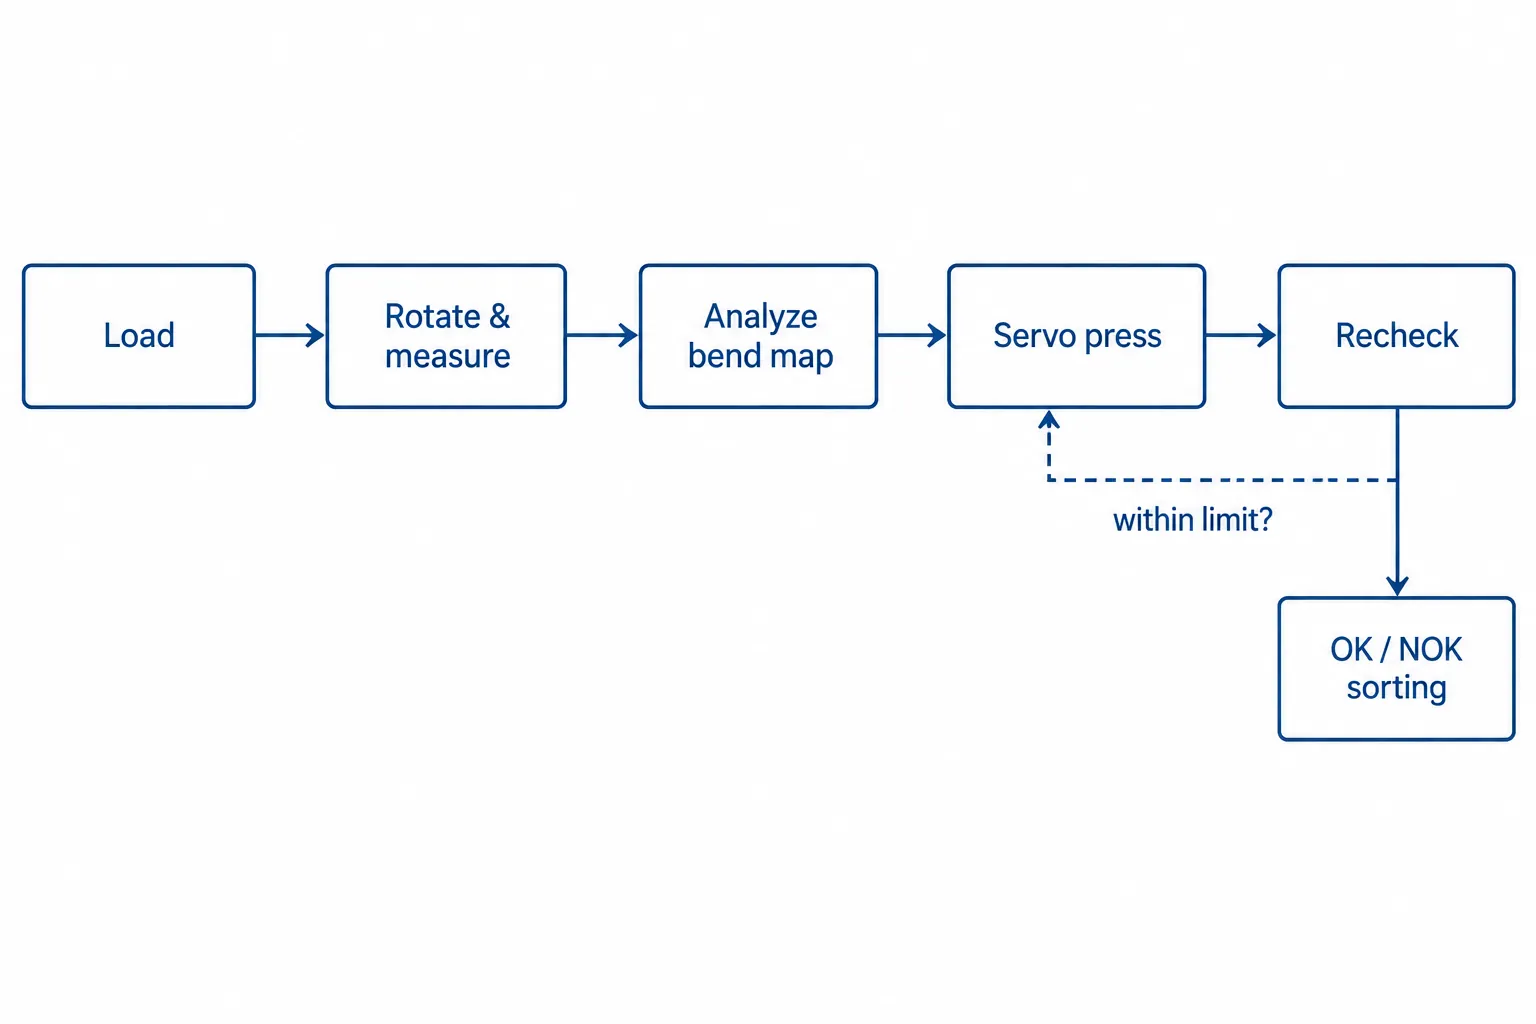
The process uses a measure–calculate–press–remeasure loop. The measuring system first creates a runout profile at defined axial positions; the control identifies the correction point and direction, positions the safe shaft section relative to the press tool, and applies a limited over-bending stroke to compensate elastic springback. After each correction the shaft is measured again using the same datum, and the part is accepted only when all required points are within the confirmed tolerance. If the result remains outside tolerance after the permitted number of cycles or reaches a force/stroke limit, the machine classifies the part as NOK instead of continuing uncontrolled correction.
| Step | Process | Key Control |
|---|---|---|
| 1 | Identify the shaft model | Load the correct tolerance, measuring points, and tooling recipe |
| 2 | Load and position | Support approved reference sections without contacting the worm thread |
| 3 | Rotate and measure | Record runout magnitude and angular position at defined points |
| 4 | Calculate correction | Select the bend peak, safe press point, support span, initial stroke |
| 5 | Index the shaft | Align the bend direction with the press axis |
| 6 | Apply controlled over-bending | Limit displacement and, where configured, monitor force |
| 7 | Remeasure and adapt | Compare the new result with the target and calculate the next action |
| 8 | Accept or reject | Use tolerance, cycle, and safety limits to determine OK/NOK |
| 9 | Log and unload | Save available process data and transfer the part |
Initial measurement
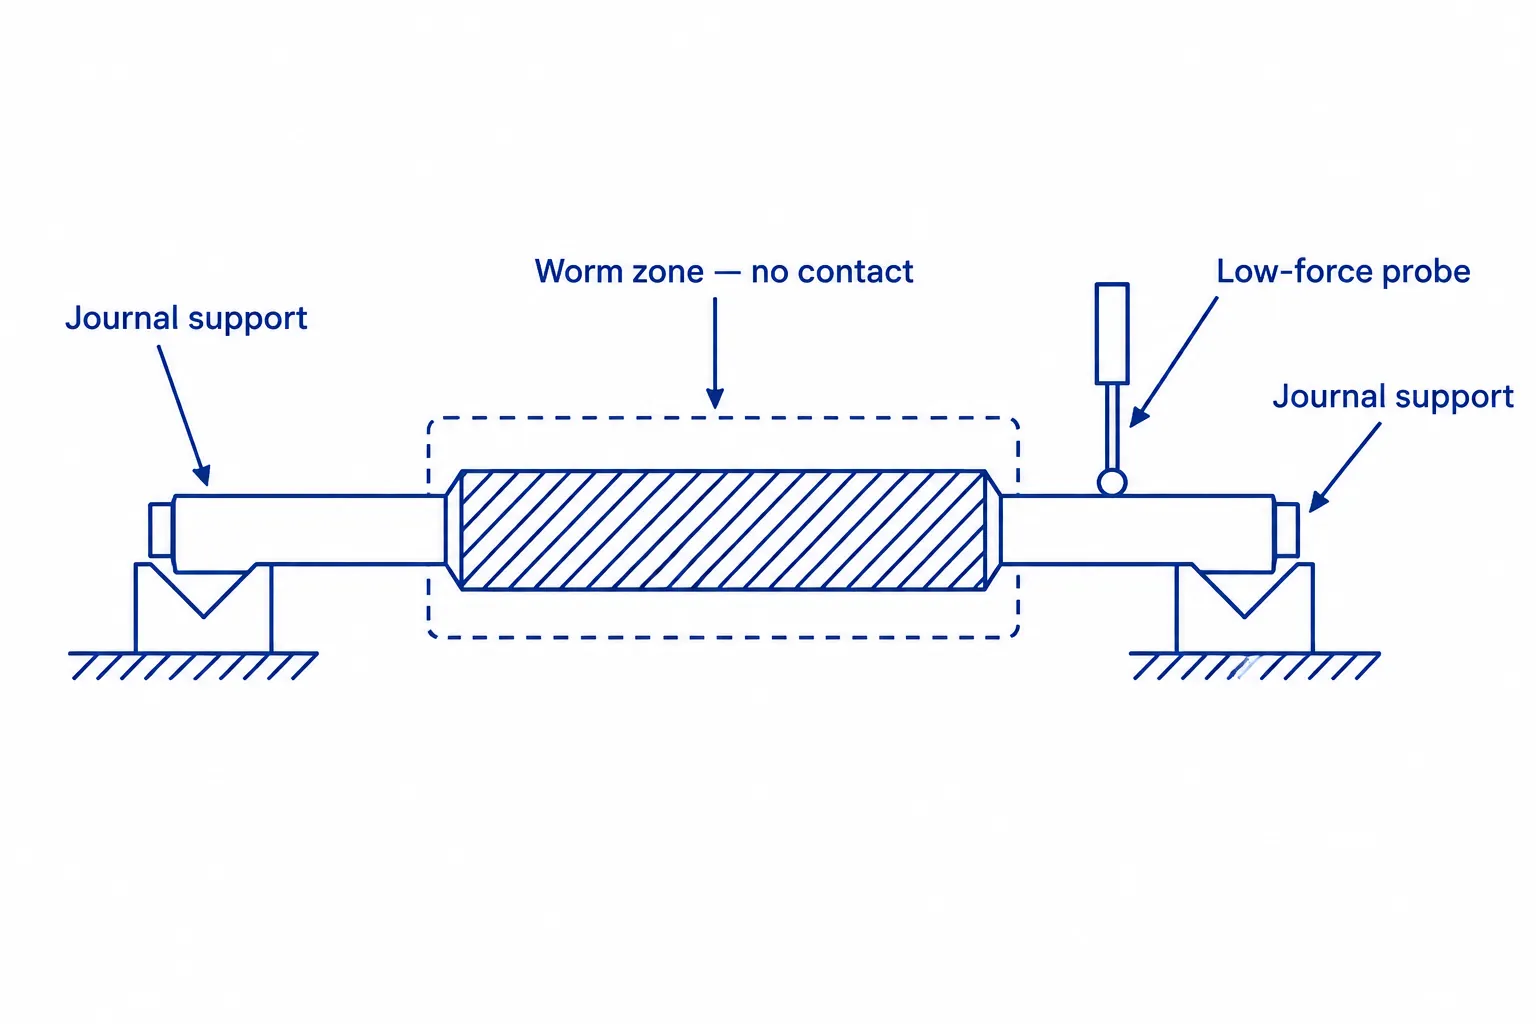
The shaft is placed on miniature supports or between suitable centers, depending on the agreed production datum. The fixture must prevent axial movement while allowing stable rotation. Sensors measure only at approved cylindrical sections; the worm thread is not treated as a normal measuring surface unless a dedicated method has been validated.
Correction calculation and press positioning
The controller uses the measured waveform to determine the angular direction and axial location of the dominant bend, then selects an allowed press point and support position from the model recipe. Grooves, shoulders, thread roots, and abrupt section transitions are excluded or specially evaluated because they concentrate stress.
Controlled over-bending and springback
Straightening requires the shaft to be bent beyond its final target so that it settles closer to straight after elastic springback. The required over-bending depends on the material condition and local section stiffness; it should be established from controlled sample trials and refined by measured response, not by an unsupported universal coefficient.
Remeasurement and sorting
The same measuring sequence is repeated after correction. A qualified part moves to the OK output; a part that reaches the permitted correction count, force, displacement, or measurement-consistency limit moves to NOK or manual review. This protects the part and prevents a machine from hiding an unstable upstream process behind excessive correction cycles.
Engineering Difficulties and Control Strategy
Difficulty 1: Establishing a functional datum
The visually straightest surface is not always the correct datum. Bearing journals or centers may determine how the shaft runs in the motor, while other diameters may be non-functional machining surfaces. The solution is to align machine measurement with the drawing and the customer’s final inspection method; datum selection, support contact, and sensor locations should be documented in the recipe and in the acceptance test.
Difficulty 2: Protecting the worm thread
The worm thread transmits load and controls meshing with the worm wheel. Direct pressing, hard clamping, or incorrect support near the thread can damage the profile or concentrate stress at the root. The worm area should be defined as a protected zone: pressing occurs on an approved smooth section, and support materials and contact geometry are selected to avoid unacceptable marks on finished journals.
Difficulty 3: Controlling a small correction window
On a slender shaft, a small change in stroke produces a meaningful change in runout, and batch variation in hardness and heat treatment changes the response. The control strategy is staged correction with conservative initial limits, followed by remeasurement and adaptation. Recipe limits should include maximum stroke, maximum cycles, and plausibility checks for inconsistent sensor data.
Difficulty 4: Managing several shaft models
Different worm shaft models may change in overall length, journal position, thread length, and safe pressing zones, so a single fixture or program may not cover them reliably. Changeover should be based on a validated model matrix—each recipe with its own datum, measuring points, protected zones, support locations, and correction limits. Mechanical poka-yoke, barcode, or DMC selection can be added when the line requires model traceability.
Recommended Cell Configuration
| Module | Proposed Configuration |
|---|---|
| Machine | Precision automatic point straightening machine for small shafts (AMS-PS300H class) |
| Measuring | Fine-contact displacement probes or another validated runout system |
| Rotation | Controlled shaft rotation on precision supports or centers |
| Press unit | Fine-displacement servo-electric or precision hydraulic unit, sized by test |
| Tooling | Model-specific miniature supports and protected press contact |
| Controls | HMI recipes, closed-loop correction, cycle/stroke limits, OK/NOK logic |
| Loading | Manual for low volume; feeder, conveyor, or robot for validated high-volume parts |
| Data | Before/after readings, correction count, part result where required |
| Safety | Interlocked guarding, overload protection, abnormal-measurement alarms |
Proposed Validation Plan
This page describes a tested machine plus a proposed engineering process. Before final quotation, representative samples from the expected material and heat-treatment range should be tested to confirm the datum, incoming runout distribution, achievable result, support and press positions, surface condition, correction count, and any crack or thread-damage risk. The acceptance report should clearly separate the customer’s target from measured sample results; once mass-production data is available, the process can be upgraded to a documented manufacturing case with sample size, inspection method, cycle time, and customer-approved results.
Information Needed for a Straightening Proposal
Please provide the shaft drawing, material and hardness, heat-treatment and machining stage, overall length and all relevant diameters, worm thread position, bearing-journal locations, initial runout range, final tolerance, inspection datum, allowed pressing areas, protected surfaces, required takt time, annual volume, loading method, and representative samples. These inputs let the engineering team select the measurement method, support spacing, press position, force/stroke range, correction logic, and automation level—and prevent a quotation from being based only on the shaft name or an external photograph.
FAQ
What runout can the machine achieve?
The achievable result depends on shaft geometry, datum, material, hardness, initial bend, surface condition, and measuring method. A guaranteed value should be based on the drawing and representative sample tests—the 0.01 mm trial figure above is specific to the 8 x 130 mm family tested.
Can the machine protect the worm thread and bearing journals?
Yes, when the drawing provides safe support and pressing sections. The recipe can exclude the worm thread and other functional areas, while contoured supports help distribute contact on approved surfaces.
How is springback compensated?
The machine applies a controlled over-bending stroke, remeasures the result, and adjusts the next correction within validated limits. The response should be learned from actual samples rather than assumed from material name alone.
Can one machine straighten several worm shaft models?
Potentially, if their dimensions, required force, datum, and tooling needs fall within the validated machine range. Each model still needs a dedicated recipe and may require change parts.
What happens if a shaft cannot be corrected?
The system stops when the part reaches its allowed correction count, stroke, force, or measurement-consistency limit, then classifies the part as NOK or sends it for manual review.
What is needed before quotation?
The minimum useful package is a drawing, material and hardness, process stage, initial and target runout, inspection datum, protected areas, takt time, annual volume, and sample parts.
Conclusion
Small motor worm shafts combine a slender body with a functional thread and precision journals. Their straightening process depends on accurate datum-based measurement, safe support and press positions, controlled springback compensation, and repeatable final inspection. The same automatic platform covers other precision shaft families such as ball screws, splined shafts, and steel shafts and bars. Amolin aims to provide a reliable and stable straightening machine for your need—contact the straightening solution team with your shaft drawing, initial runout range, target tolerance, production volume, and sample information for a feasibility review, or message WhatsApp +86-13851850644.