
A turbocharger shaft is the rotor at the centre of a turbocharger: a slender shaft carrying the turbine wheel at the hot end and the compressor wheel at the cold end, running on a small journal bearing or ball-bearing cartridge at speeds into the hundreds of thousands of rpm. At those speeds geometry is not a comfort item. Shaft straightness sets the running clearance of the bearing system, the seal behaviour, the vibration signature and, ultimately, the survival of the wheels. A bowed turbo shaft that passes a static inspection can destroy itself in seconds at operating speed.
Turbocharger shaft straightening is therefore a micro-precision correction problem that sits closer to precision spindle work than to general shaft work. It is also a field full of bad advice: forum threads asking whether a bent turbo shaft can be straightened usually end with “replace the core”, which is the right answer for a mechanic with a hammer and a V-block and the wrong generalization for a remanufacturing operation with a controlled process. Five questions open the solution:
- What exactly is the shaft: a one-piece turbine-and-shaft rotor, or a shaft with wheels assembled by welding or brazing?
- Is the deviation a true centreline bow, thermal distortion, assembly-induced distortion, or damage such as a bent wheel or cracked shaft?
- Which measurement convention and supports reproduce the functional axis: bearing journals, centres, or wheel pilot datums?
- Which correction route is approved at which process stage: micro point-pressing, stress-relief treatment, or scrap?
- How will post-correction verification, balancing and cycle limits be enforced?
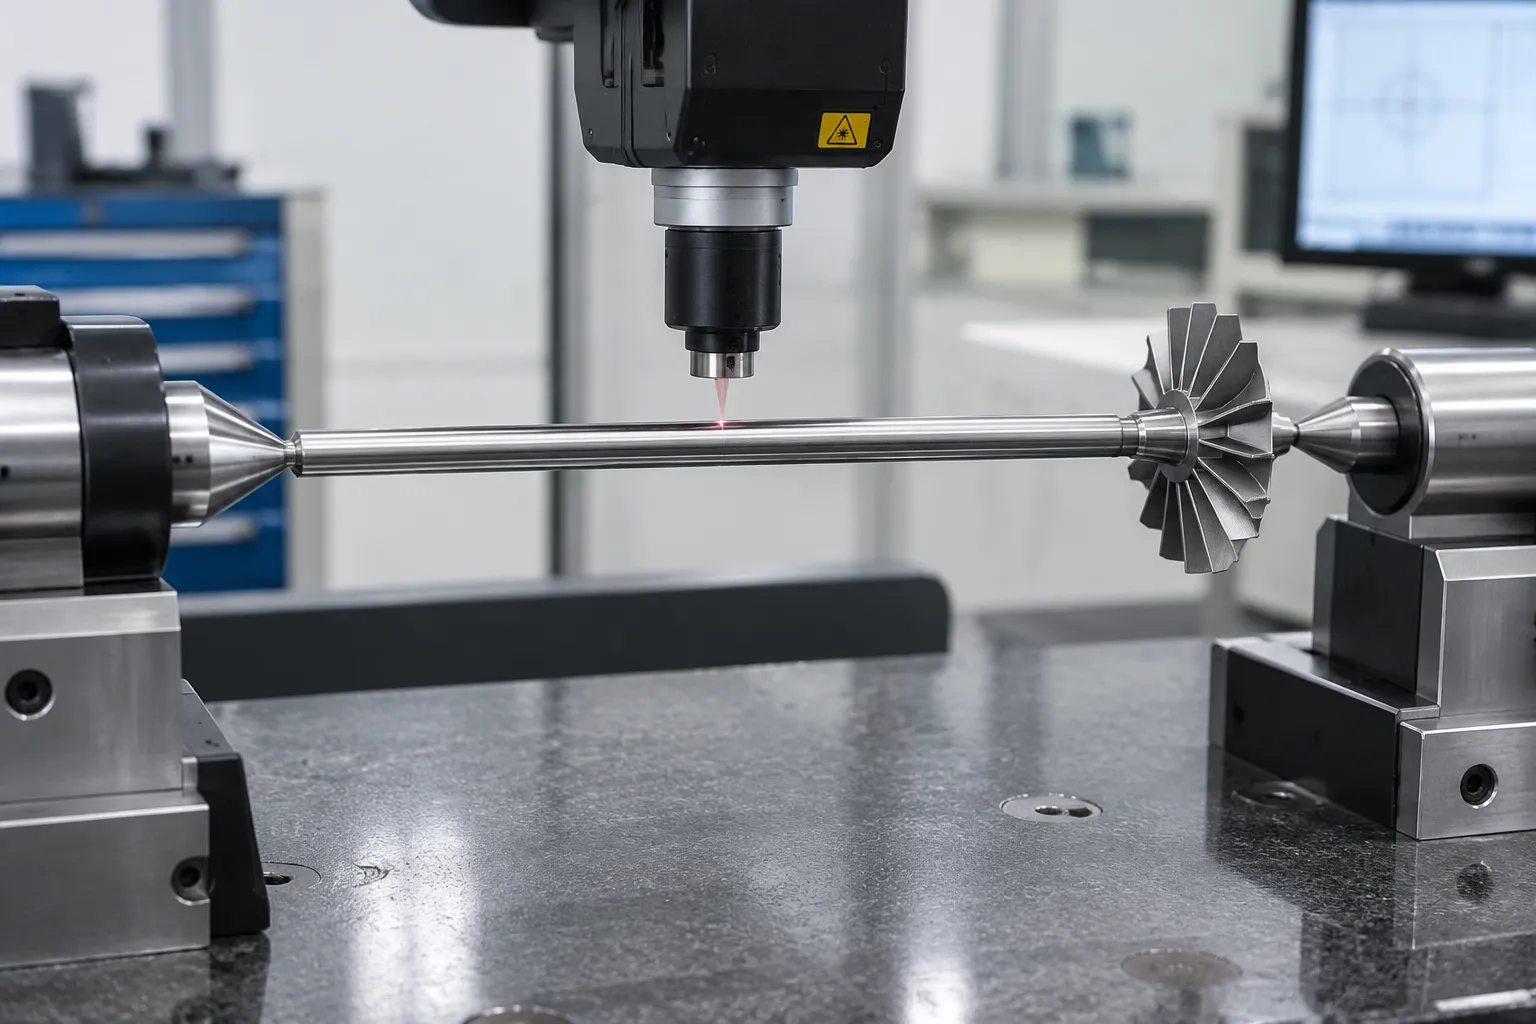
Engineering concept illustration: a turbocharger rotor supported and measured for a controlled correction study. Not a customer-site photograph; force limits, support zones and process approval require drawings and sample tests.
Know the Rotor Architecture First
The correction strategy depends on how the rotor is built, and offering one process for all of them is a red flag in any supplier discussion:
| Rotor type | Construction | Straightening implication |
|---|---|---|
| One-piece turbine shaft | Turbine wheel and shaft machined from one casting or forging | Correction acts on the shaft section; the wheel is the datum system |
| Welded / friction-welded rotor | Shaft welded to the turbine wheel | Weld distortion is a primary bow source; heat-zone correction rules apply |
| Brazed or assembled compressor side | Compressor wheel mounted on the shaft nose | Assembly-induced distortion; often correctable before wheel mounting only |
| Ball-bearing cartridge rotor | Shaft rides on a preloaded cartridge | Tightest clearances; narrowest correction windows |
How Turbo Shafts Deform
- Welding and joining distortion. Where the shaft joins the turbine wheel, the weld or braze zone introduces asymmetric residual stress and the rotor bows in a repeatable direction. This is a production-process deviation and the most systematically correctable class.
- Heat-treatment distortion. Hardening of the journals releases machining stresses, and the timing and risk rules for correcting hardened parts apply with full force.
- Thermal bow in service. A hot shutdown with the rotor stationary can permanently deform a shaft. Remanufactured cores show this signature: a smooth bow with no mechanical damage.
- Impact and FOD damage. A compressor wheel that ingested debris, or a rotor dropped at disassembly, shows bent wheels, dented seal surfaces, sometimes cracked shafts. This class is an inspection-and-reject problem; correction is not on the table until cracking is ruled out.
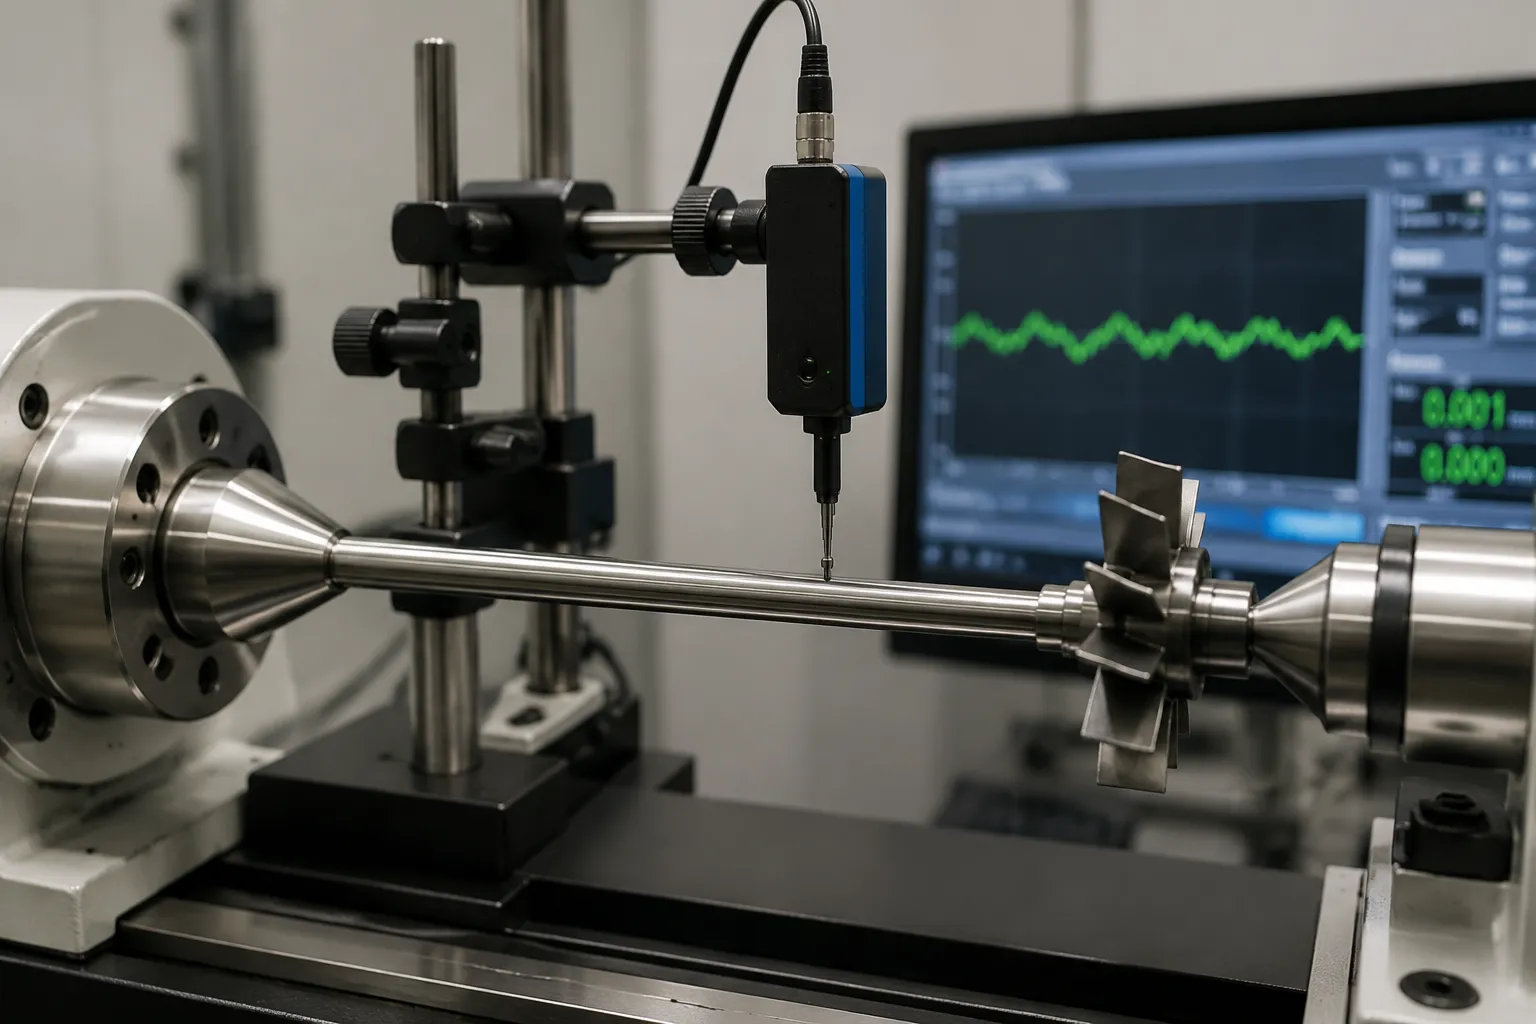
Measurement: Reproduce the Functional Axis
The functional axis of a turbo rotor is defined by its bearing journals, the surfaces that actually run in the bearing system. Everything else, seal diameters, wheel pilots, the nut thread, is measured relative to that axis:
- Support on the bearing-journal datums, or between centres where process centres exist and are proven concentric to the journals.
- Map multiple stations: journals, seal diameters, shaft mid-span, wheel pilots and nose. A single mid-span reading cannot distinguish a bow from wheel runout; multi-point electronic mapping is the standard architecture.
- Separate error types: journal roundness versus axis bow is the classic confusion in rotating measurement. Wheel face and pilot runout belong to the wheel, not the shaft axis; a rotor with a true shaft and a bent wheel does not go to the straightening press.
- Mind the measuring force. The shaft is thin, and stylus force between supports bows it measurably. Non-contact sensors or strict loaded-versus-released conventions resolve this.
New Production versus Remanufacturing
New production
In rotor manufacturing the deviation is process-generated, weld shrinkage, heat treatment, machining stress, and the population statistics are stable. Correction recipes are validated per rotor type, the correction station sits at a defined point between operations, and every rotor continues to balancing and final inspection. Straightening is a routine, audited production step whose economic value is the recovery of expensive rotor forgings and machined assemblies.
Remanufacturing and repair
A returned core arrives with an unknown history: overspeed, overheating, oil starvation, foreign object damage, previous disassembly attempts. The same visible bow can come from a benign thermal soak-back or from a rotor near its fatigue limit, so remanufacturing correction is gated by inspection, not measurement alone: crack detection on shaft and wheel before any correction; bearing-journal condition, scoring, discoloration, size, evaluated for regrind potential; wheel integrity, because bent, eroded or cracked wheels disqualify the rotor regardless of shaft geometry; prior-correction history counted against a hard cycle limit; and a defined escape route, so rotors failing any gate go to teardown and parts recovery instead of the press.
What Precision Means Here
Turbo rotor runout specifications sit among the tightest in general metalworking. Journal-to-journal runout and shaft runout relative to the bearing axis are commonly specified in single-digit micrometres, with seal-diameter runout tighter still because seal clearance governs oil control. Three implications follow. First, the measurement system is the process bottleneck: supporting a thin rotor, rotating it true and resolving one micrometre of runout repeatably is harder than applying a three-micrometre correction stroke, so budget and engineering go to metrology first. Second, correction strokes are microscopic, which puts the press in the regime where frame compliance, drive resolution and thermal drift dominate the error budget, the same regime discussed for machine tool spindle straightening. Third, documentation is part of the deliverable: incoming map, correction record with position, stroke and cycle count, outgoing map, balance record, serialized per rotor. For remanufactured cores this record chain is frequently a customer or certification requirement, not an internal courtesy.
Correction Routes
Micro point-pressing
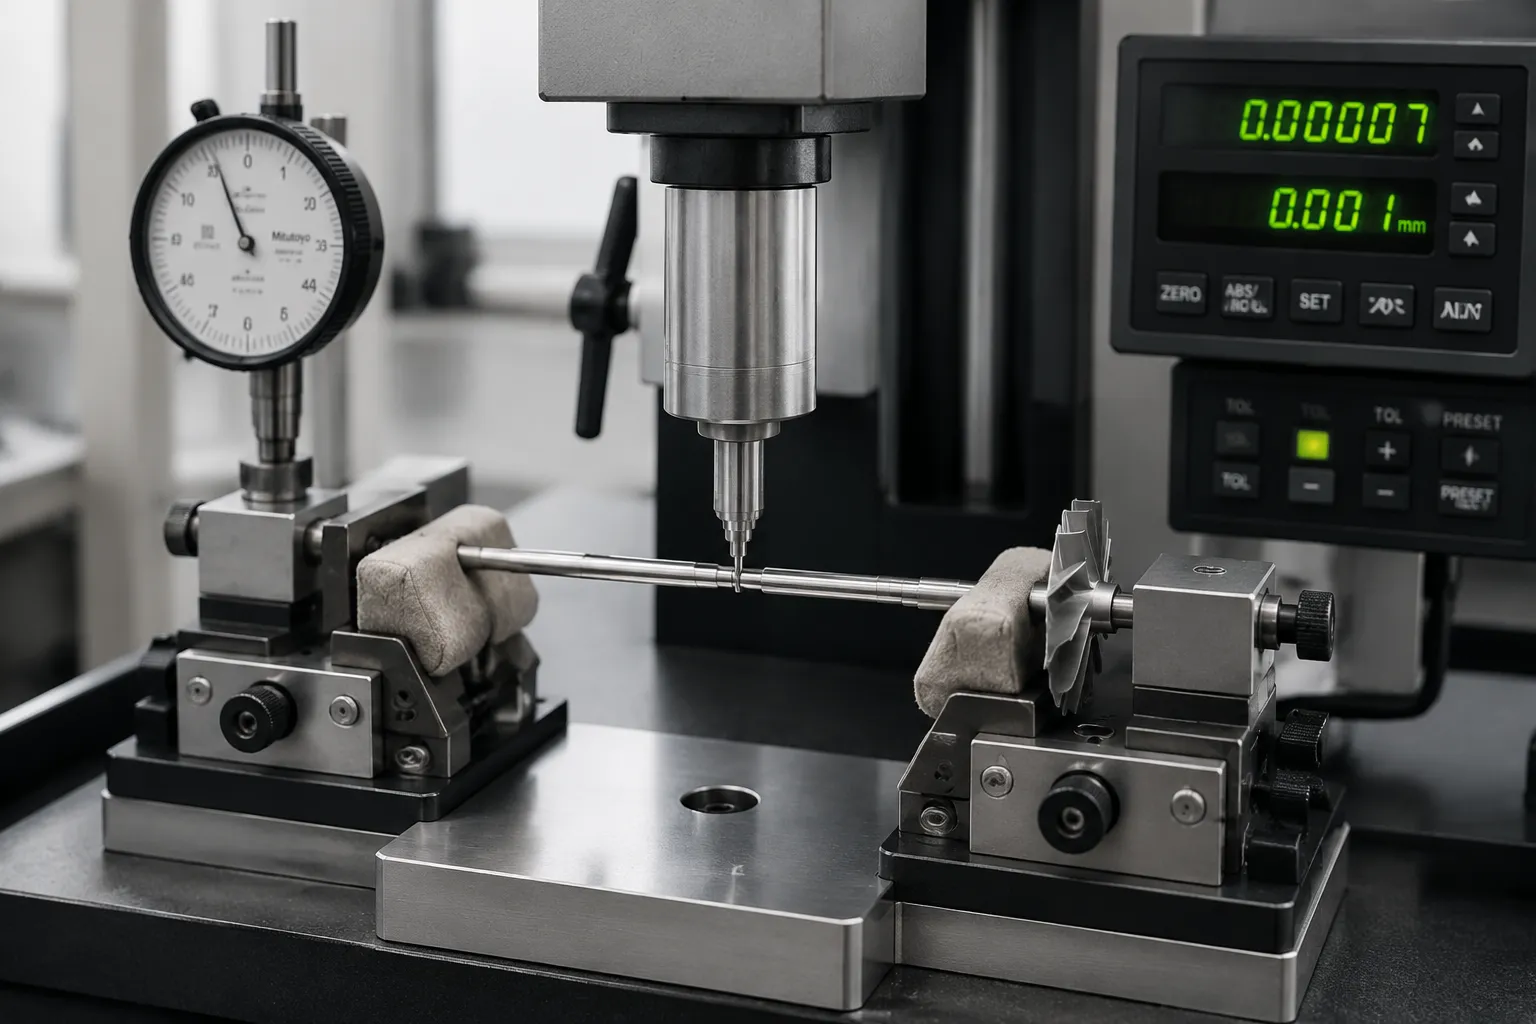
For a true centreline bow, the applicable route is precision point-press straightening scaled to its smallest and most careful form: soft or non-marring supports positioned per the bend map, a displacement-controlled micro-stroke at the apex, typically a few micrometres, and immediate re-measurement. The shaft is thin and usually hard, so springback dominates; the process needs validated compensation rules per material state, and pressing never touches the weld zone, seal lands or thread without explicit process approval.
Thermal stress relief
Where the bow stems from residual stress, welding or heat treatment, a controlled stress-relief treatment can relax it without mechanical contact. Slower and less precise than pressing, it is sometimes sequenced before a final micro-press, because pressing a highly stressed part invites drift later.
Not correctable
Cracked shafts, where crack inspection is a gate before any correction; bent or eroded wheels; damaged journals needing regrind; and rotors whose remaining stock cannot clean up after correction. For these the route is the remanufacturing decision tree. Repeated correction cycles on one rotor must be limited and recorded, with the added weight that this is a rotor, not a bracket.
Verification and Balancing: The Non-Negotiable Pair
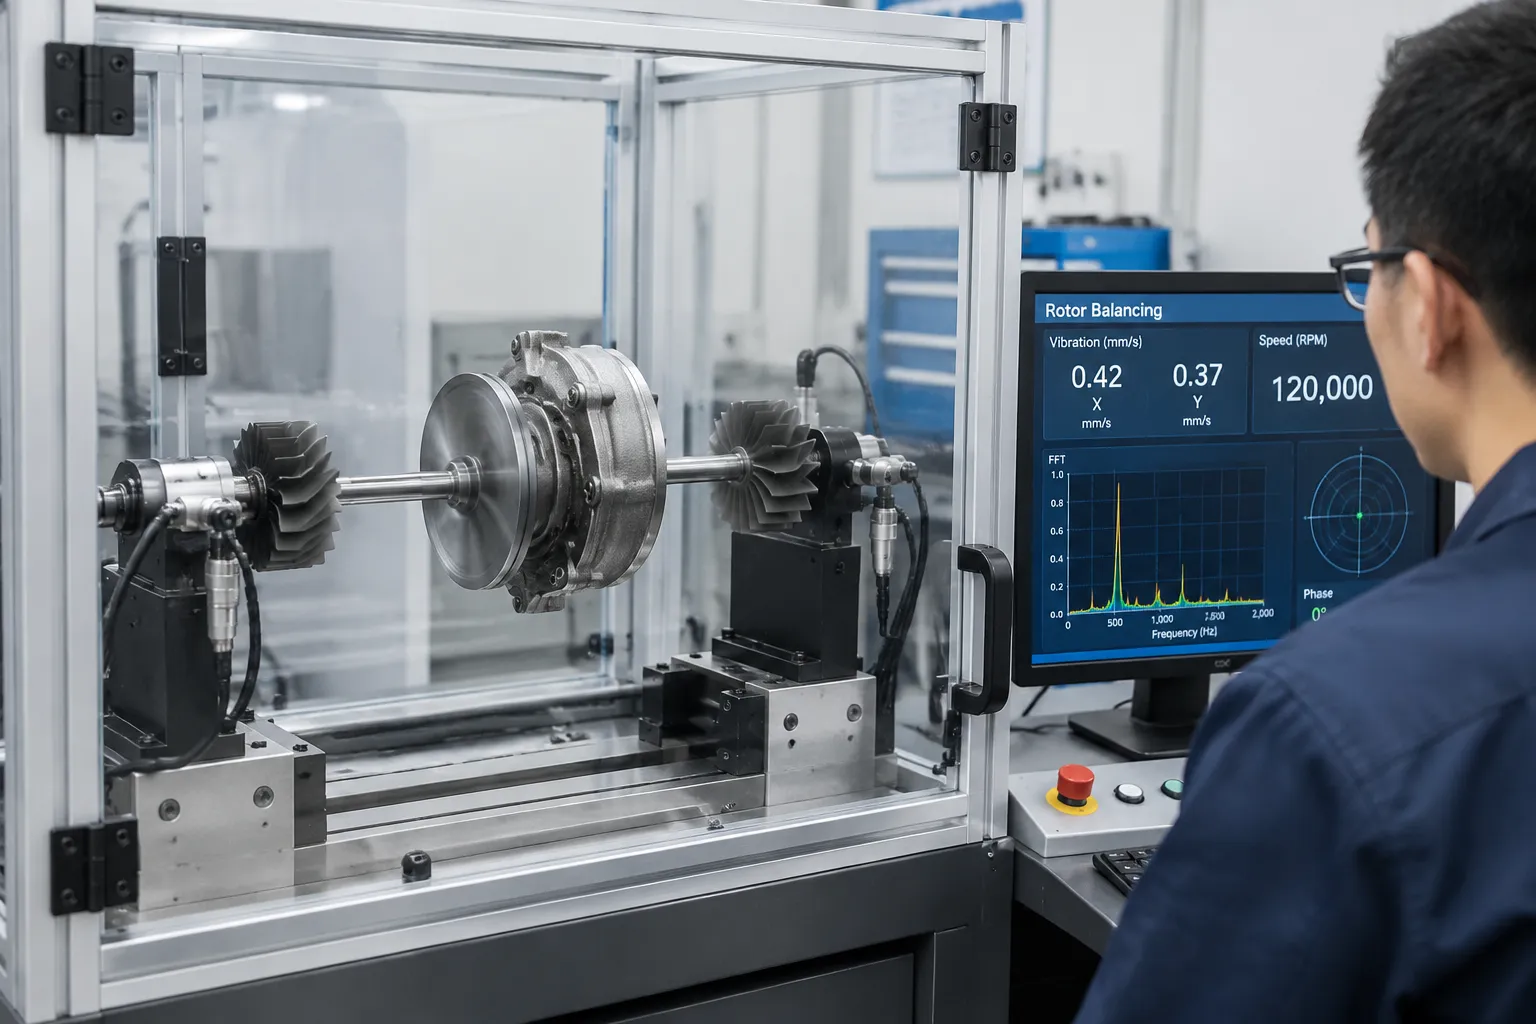
Correcting a rotor is only half the job. Acceptance requires: a post-correction runout map in the identical support and measurement condition as the incoming map, at all functional stations; form verification, journal roundness, surface finish and seal-surface condition untouched by tooling, where any witness mark on a bearing or seal surface is a reject; rebalancing, because straightening redistributes mass geometry, so every corrected rotor returns to the balancing machine and the balance record travels with the correction record; and gauge capability proven at these tolerances, because at turbo level the measurement system is the process. The same straightness-balance coupling governs other rotor families, including electric motor rotor straightening.
Machine Architecture for Micro-Correction Work
The machine that corrects turbo rotors looks almost passive next to a production shaft straightener, because its defining components are metrology and control, not force. The press frame is small but extremely stiff, so the stroke that reaches the rotor is the stroke the control commanded. The ram drive resolves sub-micrometre steps and holds position under load without overshoot. Supports are bespoke per rotor family, shaped to the bearing journals or designated loading zones, made of softer or protected materials, never touching seal lands or threads. The measuring head integrates into the same setup so the rotor is mapped, corrected and re-mapped without re-chucking, because re-clamping a thin rotor between cycles introduces more error than the correction removes. Operators matter as much as hardware: loading the rotor, interpreting the bend map and deciding press-again-or-release is skilled work, and the best cells formalize that decision logic into the machine control so the skill lives in the process rather than in one person. Buyers should evaluate a turbo shaft straightening offer by asking to see the measurement data flow first and the press second; the order of priority tells you whether the supplier understands the workpiece.
Common Failure Modes
- Correcting past a crack. A slightly bent rotor from a seized or overheated turbo may be cracked. Pressing it back to zero without inspection creates a fragility bomb. Crack detection precedes correction, always.
- Chasing wheel runout as shaft bend. The map shows runout at the wheel pilot; the press lands on the shaft; both ends are now worse.
- Pressing on forbidden zones. A stroke at a seal land, journal or thread fixes the map and destroys the rotor functionally.
- Straightened but never rebalanced. The rotor passes static runout and fails at speed with vibration, seal rub, wheel contact. Balance verification is part of straightening acceptance, not an optional extra.
- Forum-grade advice in a production setting. “Tap it back with a hammer” destroys rotors; “replace the core” wastes recoverable production rotors. The professional answer is a controlled correction process with inspection gates.
For a turbocharger shaft feasibility study, prepare the rotor drawing, the runout specification at each functional station, and incoming runout maps plus crack-inspection records from a representative rotor sample. Machine-level context for the closed-loop architecture is covered in the shaft-type parts straightening overview.