

A bolt straightening machine removes the post-heat-treatment bend from long, high-strength bolts and holds the corrected axis inside a tight tolerance window—repeatedly, without an operator judging each hit. On this page you will find the tested machine specification and trial video first, then the engineering behind the automated bolt straightening process: why long bolts bend during heat treatment, how the bend pattern is mapped before any press stroke, how threads and head zones are protected during correction, and what a complete acceptance package should contain before you sign off a supplier.

Tested Specification and Machine Video
The tested bolt family for this trial: M12 x 90 mm high-strength bolts, required straightness 0.05 mm, corrected on an AMS-PS300 automatic straightening machine at a cycle time of about 20 seconds per piece. The trial video below shows the complete measure–press–recheck loop running unattended.
The same process line scales across bolt families. A reported fastener-plant case on 15 mm x 340 mm long bolts (initial bend 0.5–1.5 mm after heat treatment) took an 8-person manual correction line to one operator supervising four machines, with straightness held under 0.1 mm on the client’s own acceptance records. Both the small-diameter trial and the long-bolt case are covered in the process sections below.
Why Heat Treatment Bends Long Bolts in the First Place
Understanding the distortion source is what makes a correction process defensible instead of decorative. During quenching, a long fastener cools unevenly: the section cools at different rates depending on its orientation in the basket or fixture, agitation contact, and local mass differences between the plain shank, the threaded length, and the head. Each cooling path wants to contract by a different amount, and the resulting locked-in stresses bend the part when it relaxes. The effect scales with length—which is why short bolts leave heat treatment usable while long bolts of the same grade systematically arrive bent. Thread rolling and machining before treatment add their own stress history, and any straightening performed at the heat treater counts as prior deformation for everything done afterward.
Two practical consequences follow. First, incoming inspection on long heat-treated bolts is not optional paperwork: the bend magnitude and pattern arriving at the straightening station determine both the correction plan and any supplier conversation, and the interaction of prior deformation with correction response is the reason reverse-loading behavior (the Bauschinger effect) matters in fastener straightening. Second, upstream process decisions—how parts are racked or basketed through quench, whether stress relief is applied—change the distribution the straightening station sees, and are usually the cheapest place to reduce total correction work.
Reading the Bend Before Correcting It
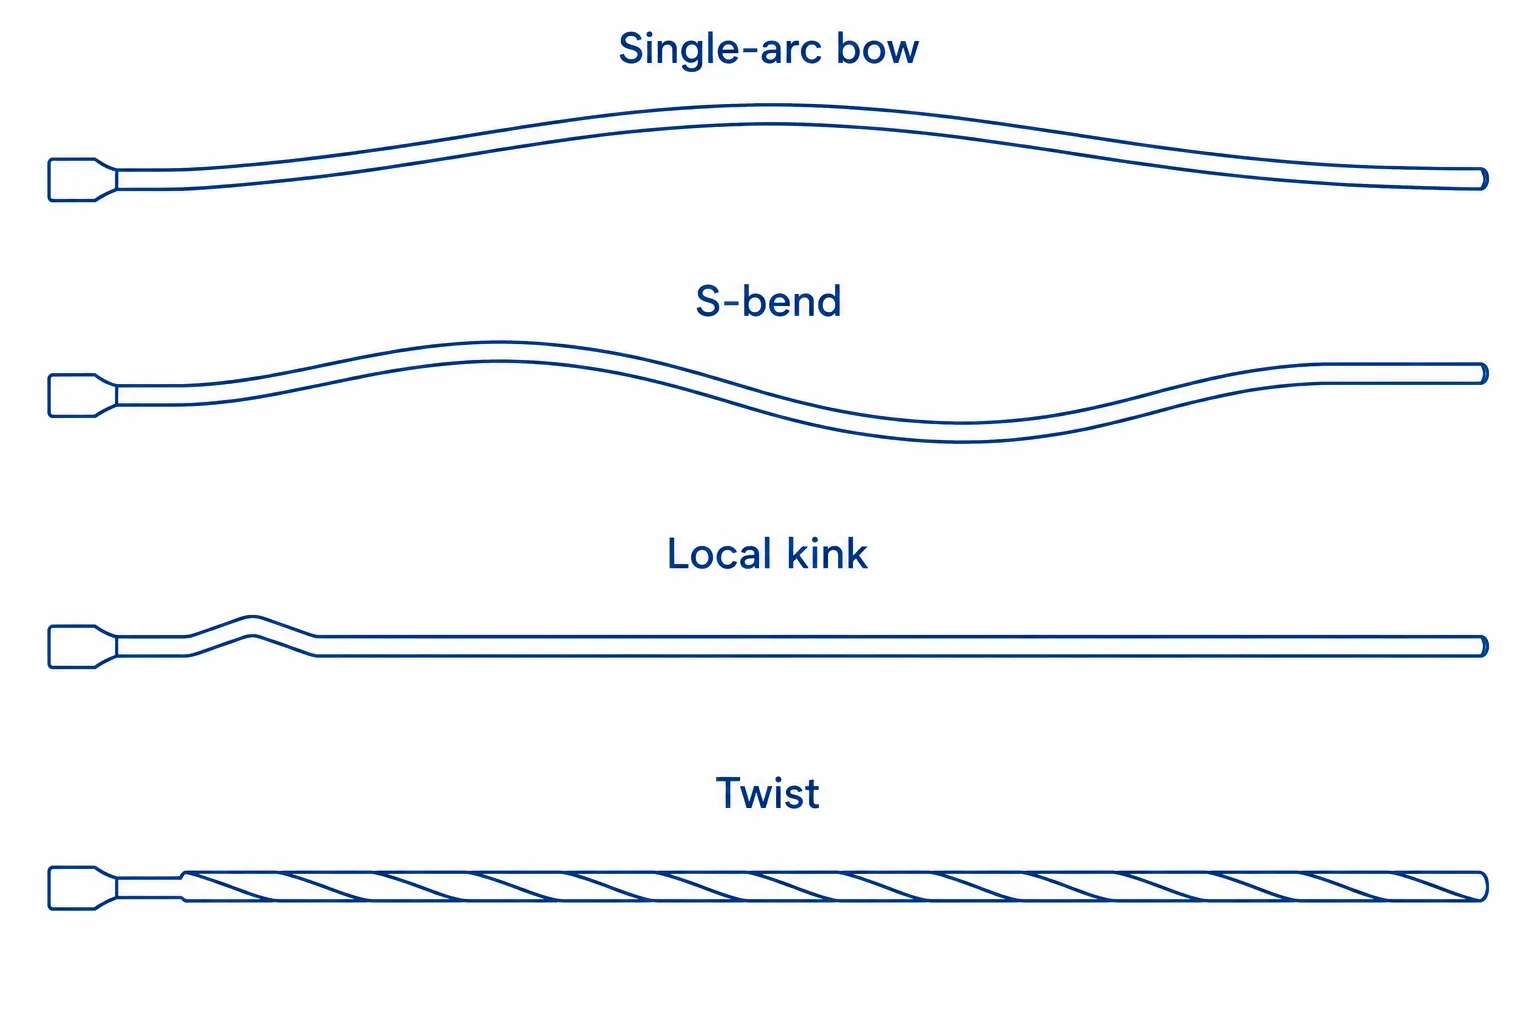
Long fasteners arrive with a small vocabulary of bend patterns, and naming the pattern is the first step of an efficient correction loop:
- Single-arc bow — one gentle curve, maximum near the middle. The most common heat-treatment signature, and the most straightforward to correct with supports positioned around the peak.
- S-shaped double bend — two opposite peaks, usually reflecting two constraint points during quench. It demands two coordinated corrections rather than one big press at the largest reading.
- Local kink near the head or thread runout — distortion concentrated where section stiffness changes; it behaves differently from a distributed bow.
- Twist about the axis — occasionally accompanies bending on parts with asymmetric features and must be separated from bend before correction.
Each pattern requires its own measurement map and correction sequence, which is why an automatic station that scans the full length and builds the map before pressing—rather than chasing the single worst reading—converges in fewer strokes.
Why Bolt Straightening Must Move Away from Manual Hammering
The comparison below is from the reported fastener-plant case mentioned above—a client’s measured baseline and post-commissioning values, not a universal benchmark for every fastener line.
| Pain Point | Manual Hammering / Manual Press | Automated Straightening |
| Labor requirement | 8 workers per shift (reported manual baseline) | 1 operator for 4 machines (reported case) |
| Straightness | 0.2–0.5 mm spread (reported manual baseline) | Under 0.1 mm (client acceptance records) |
| Cycle time | 120–180 s/piece (reported manual baseline) | 10–15 s/piece (reported long-bolt case); ~20 s in the M12 trial above |
| Overall cost | High labor cost per corrected part | Manpower reduced from 8 operators to 1 supervising 4 machines |
The Automated Bolt Straightening Process, Step by Step
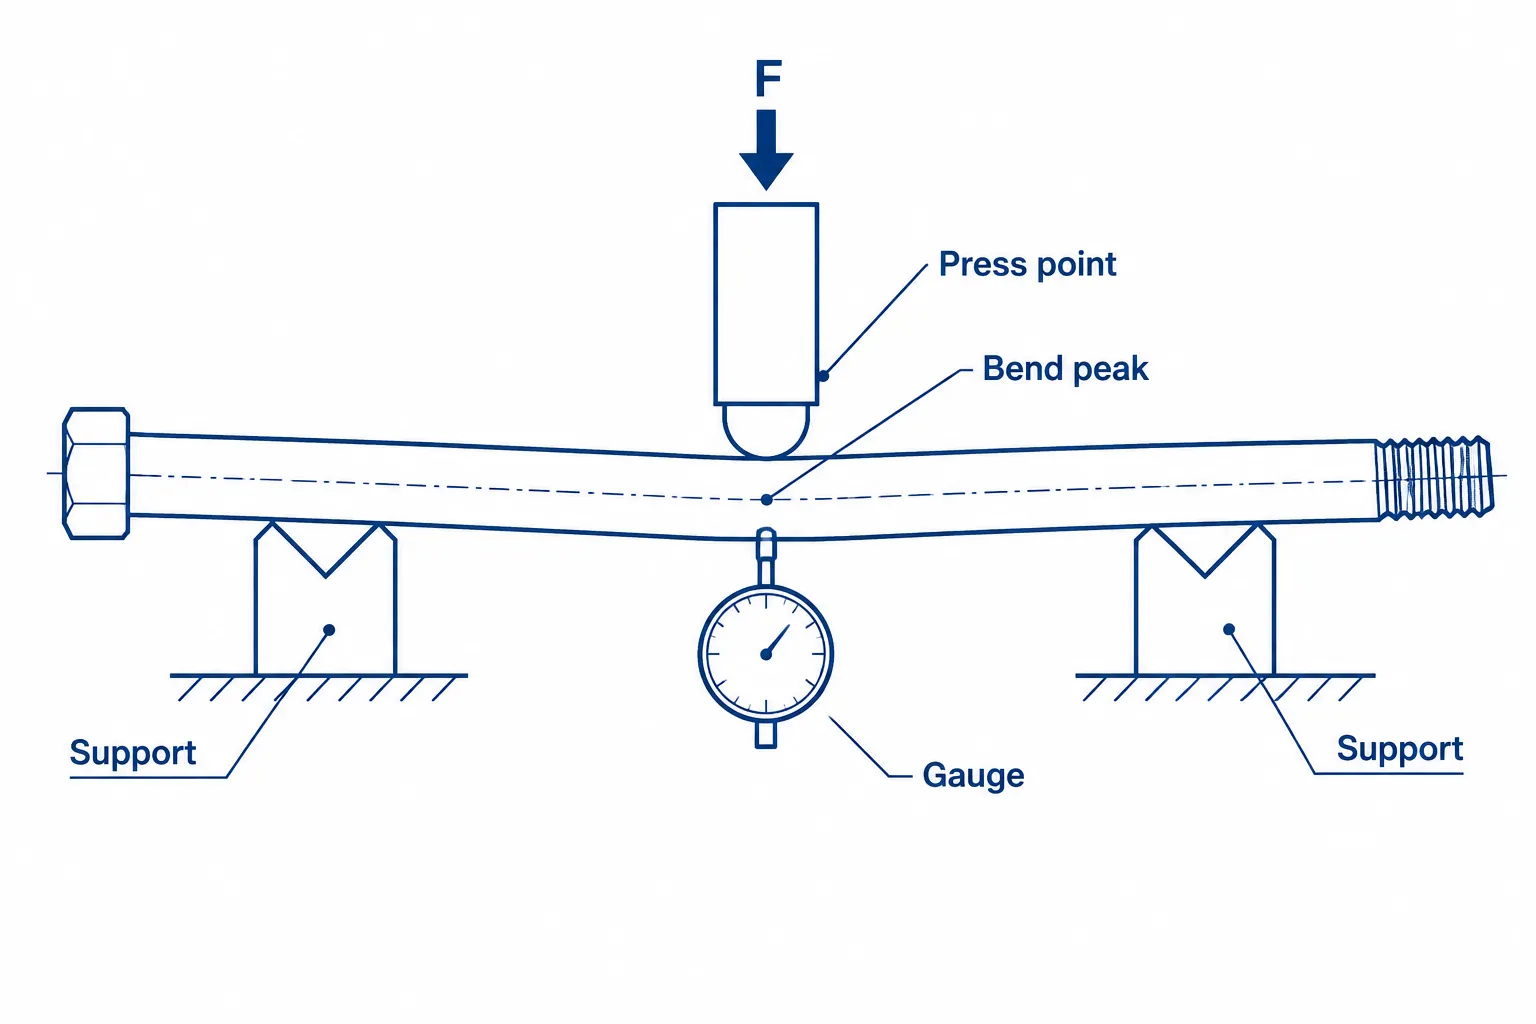
- Auto-feeding — bent bolts are fed from a hopper into the straightening station without human intervention.
- Dynamic measurement — sensors scan the rotating workpiece and capture the maximum bend point across the entire length, building the per-part bend map.
- Servo pressing — the control calculates spring-back from the material (carbon steel or alloy steel) and the servo ram applies a precise press stroke for single-pass correction where the pattern allows.
- Auto-sorting — qualified bolts proceed to the next stage; non-conforming parts are isolated automatically before they leave the machine.
Core Challenges and How the Process Answers Them
Manning: the reported “1 operator for 4 machines” case
Problem: manual hammering and press correction depend on operator skill, stamina, and shift discipline, so manning levels stay high and results vary from operator to operator.
Answer: full closed-loop automation with built-in recipes per bolt specification. A standard worker only refills the hopper periodically; measurement, straightening, and re-inspection are handled by the machine. This removes both the labor problem and the precision drift caused by fatigue.
Consistency inside the 0.1 mm window
Problem: hammer strikes leave an uneven internal stress distribution and frequently over-correct localized areas.
Answer: a fully parameterized servo control system. Instead of human judgment, sensors resolve the bolt’s axial curve with micron-level accuracy, and multi-step servo algorithms compensate the elastic spring-back of S45C and alloy steels so final straightness locks inside the qualified recipe window.
How Threads and Head Zones Are Protected During Correction
Thread protection is a contact-zone engineering problem. The correction force and the reaction forces both need somewhere to live: on a long bolt, the plain shank is the region designed to carry load, while the threaded length and the under-head fillet are the regions most easily damaged. A protection concept therefore has three parts—place supports on the shank at controlled span positions around the bend peak; direct press contact onto the shank through tooling that conforms to the section instead of touching thread crests; and keep every edge that could contact the workpiece generously radiused so load spreads instead of concentrating. Cleanliness belongs in the same discussion: debris trapped between press tooling and a thread flank is a scratch generator, and on plated or coated bolts the coating class defines how much contact the finish can tolerate at all.
The validation side is equally concrete. A thread-protection claim is proven by inspection agreed before the trial—thread gauges still running, flank condition reviewed under the method the quality function specifies—together with the released-state straightness result, on representative parts, after repeat setups. Protection and geometry are accepted together or not at all.
What a Complete Acceptance Package Should Contain
A bolt straightening process is only as good as the acceptance definition it answers to. A complete package answers five questions in writing:
- What characteristic governs — straightness of the axis, measured how: on centers, on supports, rotating, in what condition. A reading taken under restraint is not a released result.
- What the limit is, and where it applies — full length or specified spans.
- What else must survive the process — thread fit, surface finish, coating, head markings.
- How conformity is sampled — every part through an automatic gauge, or a sampling plan with a defined reaction to a failure.
- What happens to nonconforming parts — rework limits, segregation, and disposition authority.
Buyers comparing straightening suppliers are well advised to ask for exactly this package; the ability to produce it says more about a supplier than any single machine specification.
Reported Case: One Operator, Four Machines, Under 0.1 mm
The client is a well-known Indian fastener supplier providing components for global construction machinery brands. Three findings from their commissioning records:
- Repeat orders — after the performance of the first three units, the client purchased a fourth machine.
- Operator consolidation — one operator now manages all four machines, with a substantial increase in output per operator.
- Quality benchmark — the client’s records report straightness moving from 0.2 mm down to under 0.1 mm after commissioning.
FAQs
Will the straightening ram damage the bolt threads?
No. The process uses non-contact, cushioned protection tooling designed for bolt straightening: press blocks match the bolt’s shank curvature so force is distributed evenly and surface indentations are avoided, as described in the thread protection section above.
Can the machine integrate into our MES system?
Yes. The control system provides standard data interfaces to record and export real-time straightening data for every bolt, meeting modern traceability requirements.
Why do bolts from the same heat-treatment lot arrive with different bend patterns?
Because each part’s position in the basket or rack gave it a different cooling path. Quench distortion is sensitive to orientation, local mass, and agitation contact, so even identical bolts leave treatment with different locked-in stress patterns. Mapping incoming parts rather than assuming a uniform error is the practical answer—and the reason scanning-based stations build a per-part correction plan.
How many correction passes does a long bolt need?
It depends on the pattern, not a fixed number. A single-arc bow typically converges in one planned press; an S-bend needs two coordinated corrections; local kinks near section changes respond differently again. The governing rule is a rework limit set before production—parts that stop responding are routed to review, not pressed repeatedly, because each additional plastic cycle consumes fatigue life and changes the material’s response.
Should straightening come before or after thread rolling?
The route belongs to the fastener process engineer, but the trade-off is explicit: correcting before thread rolling lets subsequent operations work from a straight blank, while correcting after heat treatment on finished threads demands the contact-zone protection described above. Whichever route is chosen, the acceptance package must define what state the straightness limit applies to, and correction validation must run on parts carrying that state.
Summary and Next Steps
For fastener factories chasing lower manning and 0.1 mm delivery precision, an automated bolt straightening machine is a direct route to both. The figures on this page—one client’s reported case plus the M12 x 90 mm trial—are concrete but not universal: your own results depend on the bolt family, incoming distortion, and the acceptance definition you write. Standard bolt and rod machine lines include the AMH-B80, AMH-B240, and AMH-B450 bolt straightening machines; the same automatic process family also covers shafts and bars of other families. Facing labor management issues or a precision bottleneck? Contact us with your bolt drawing and incoming bend data for a customized technical proposal.