
How do you straighten a drill bit extension bar? The trial video below shows the machine loop on a real 150 mm extension bar, and the engineering sections after it cover what actually decides the result: the functional datum, the difference between straightness, runout, and bit-holder wobble, the contact zones that must stay protected, and the acceptance evidence a supplier should be asked for. Whether the part family is called an extension bar, bit holder extension, or screwdriver bit extension bar, the power tool extension bar straightening process follows the same rules summarized on this page.

Trial Specification and Machine Video
Tested workpiece for this trial: drill bit extension bar, 150 mm length, required straightness 0.2 mm. The video shows the complete measure–press–recheck loop on the real part.

Identify the Workpiece Before Selecting a Machine
A power tool extension bar may look like a simple slender shaft, but its two ends usually perform different functions: one end interfaces with a drill or impact driver, the other holds or drives a bit or accessory. Hexagonal sections, retaining grooves, sockets, holes, and local heat treatment make the workpiece asymmetric and leave only limited zones suitable for measurement, support, and press contact:
| Feature | Why It Matters for Straightening |
|---|---|
| Input hex shank | May define the power-tool axis but is not automatically a suitable rotating measurement surface |
| Output holder or socket | Functional wobble can depend on its bore, retention feature, and assembly condition |
| Smooth shaft zones | Potential measurement, support, or correction locations if the drawing permits contact |
| Groove, cross-hole, or transition | Creates a local stiffness change and may be excluded from pressing |
| Heat-treated zone | Changes springback and crack risk compared with the shaft core |
| Coating or finished surface | Limits permissible probe, support, and punch contact |
Tool manufacturers use terms such as universal bit holder and 1/4-inch hex-shank extension for related product families. These names define the application, but they do not prove that every extension has the same interface, material, or acceptance method—the customer drawing remains the controlling source. Earlier project records also reported a 6.35 mm x 200 mm workpiece with a 0.2 mm target; treat those as reported project inputs, not universal specifications, since the source does not define whether 0.2 mm means straightness, runout, TIR, coaxiality, or functional tip wobble. A commercial guarantee should only cover the tested workpiece family, incoming-condition window, and agreed acceptance method.
Straightness, Runout, and Functional Wobble
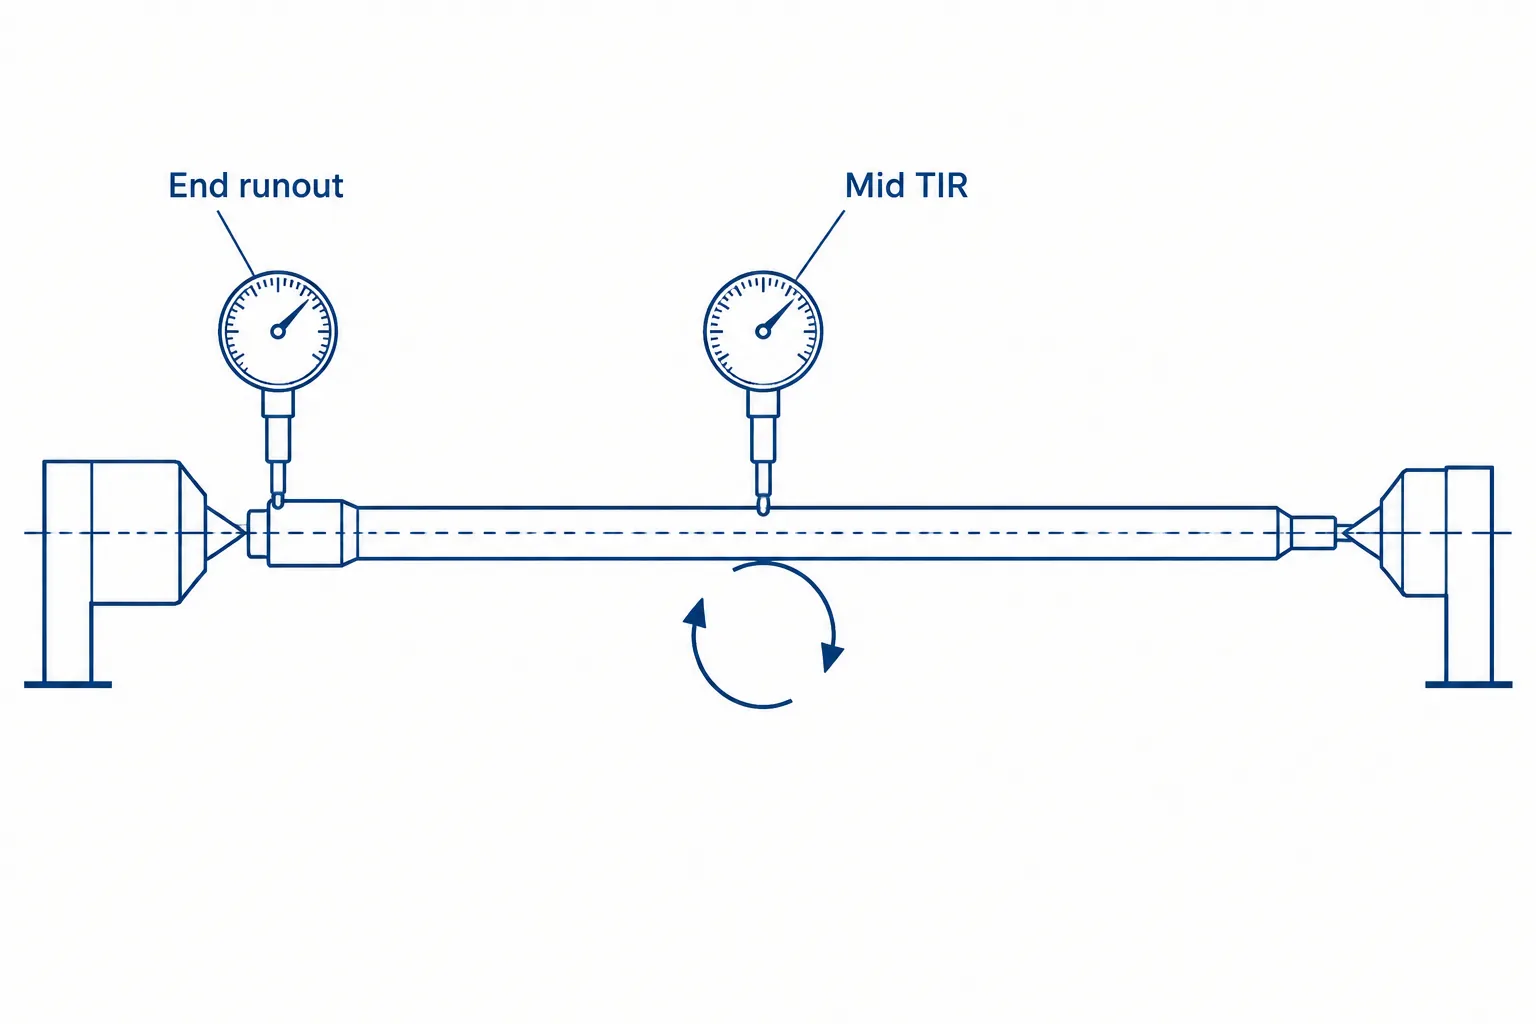
| Characteristic | Question It Answers | Required Definition |
|---|---|---|
| Straightness | How far does a selected shaft line or surface deviate from an ideal straight line? | Controlled zone, evaluation length, and datum rule |
| Radial runout/TIR | How much does a surface vary while the part rotates about a defined axis? | Rotation datum, probe position, and filtering |
| Coaxiality | How well do the input and output functional axes align? | Both axes and the applicable drawing requirement |
| Functional wobble | How much does an installed master bit or accessory move during rotation? | Master tool, engagement depth, test speed, and reading location |
A part can have an acceptable smooth-shaft reading but still fail at the output holder if an end feature is eccentric or assembled incorrectly. Conversely, a varying hex envelope can produce an unstable probe signal even when the functional axis is acceptable. The machine measurement and the customer’s final gauge must therefore be correlated during sample testing.
Recommended Closed-Loop Straightening Process
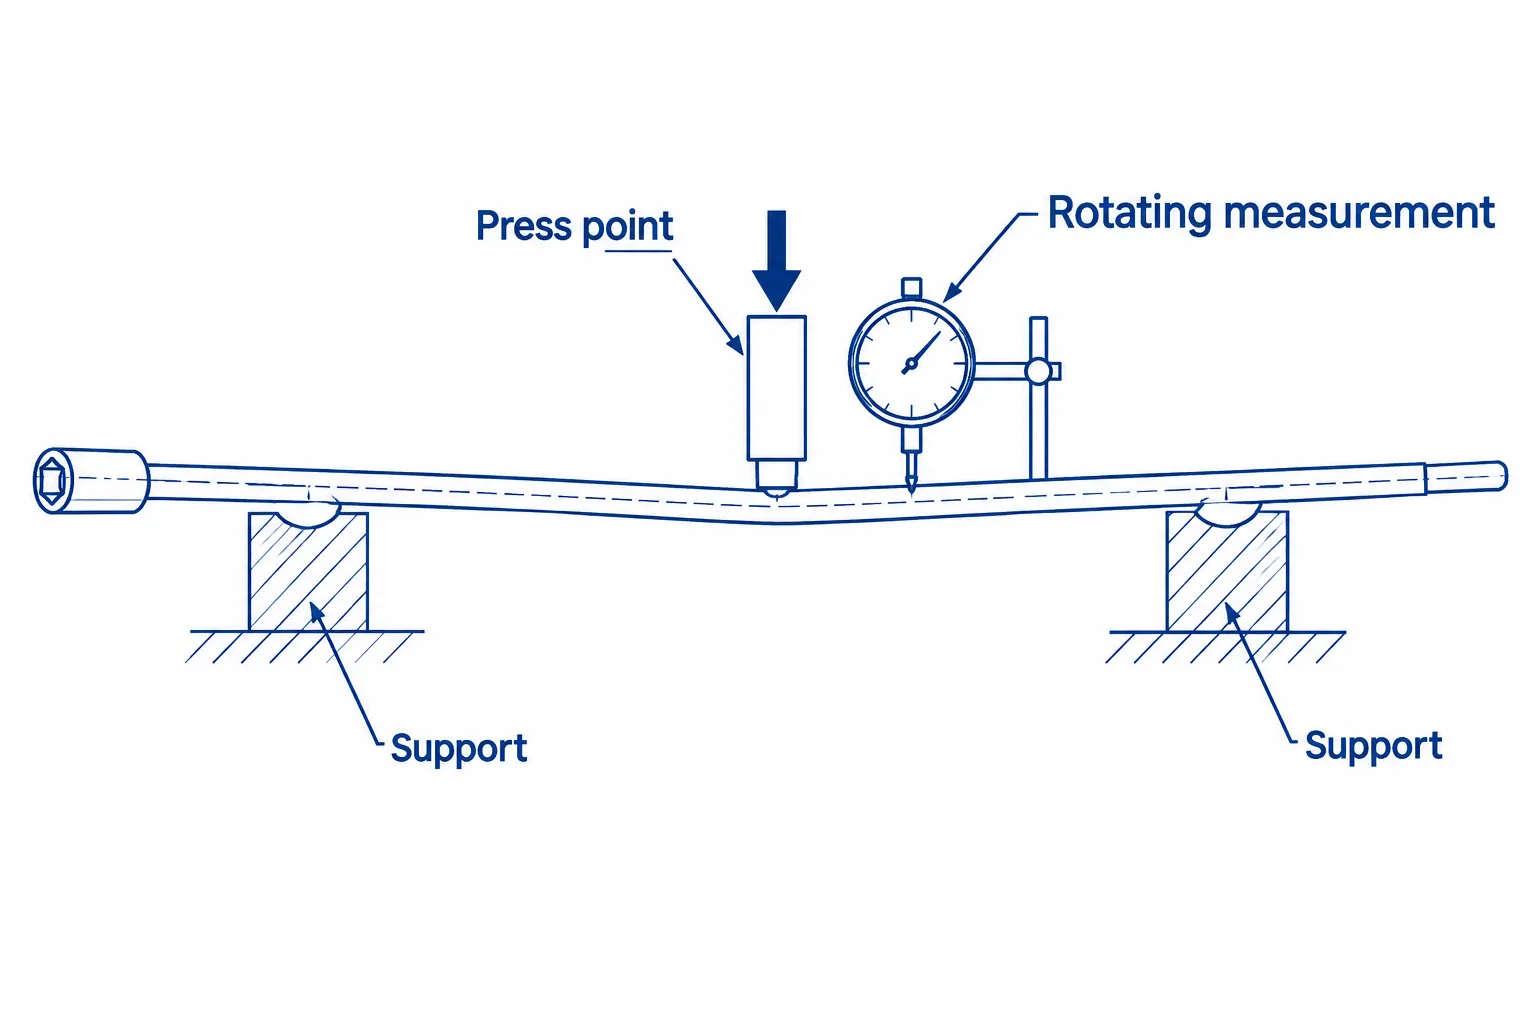
- Identify and orient the extension bar — the cell identifies the selected variant and confirms the orientation of the asymmetric ends. Feeding may be manual, tray-based, conveyor-based, or built around a validated bulk-feeding system; random bulk loading is not assumed until the real part family has passed entanglement, overlap, and orientation trials.
- Establish the functional datum — the workpiece is located by centers, approved journals, a controlled hex interface, or dedicated fixtures according to the drawing. Supports must reproduce the inspection logic without forcing the slender shaft into a false straight condition.
- Measure approved shaft zones — the extension rotates or indexes while sensors collect readings at defined axial positions. The plan excludes grooves, cross-holes, socket edges, and non-round zones unless a validated profile-specific method is used; the controller constructs an incoming bend curve and separates repeatable geometry signals from centerline displacement.
- Select the support span and correction point — tooling and software limits block contact with drive corners, retention grooves, socket lips, and bores.
- Apply staged point correction — the press applies controlled displacement or force at the selected location. Correction is incremental because thin shafts, heat-treated zones, and abrupt section changes have different springback; maximum force, stroke, and iteration limits prevent uncontrolled repeated pressing.
- Remeasure using the same datum — after each press action the system measures again without changing the acceptance reference, correcting further only when the residual error is outside the approved window.
- Verify and discharge — the final machine reading is compared with the drawing-specific rule; where functional wobble matters, the sample study correlates the machine result with the customer’s master tool or final gauge.
Tooling and Surface-Protection Strategy
“No damage” is an acceptance requirement, not a generic promise. The actual tooling must match the allowed contact zones, hardness, coating, and end geometry:
| Tooling Element | Design Question |
|---|---|
| End locator | Does it reproduce the functional axis without marking or deforming the hex/holder interface? |
| Supports | Do they carry the correction load on approved smooth zones? |
| Press punch | Is its radius/profile compatible with shaft diameter, hardness, and permitted surface pressure? |
| Measuring probe | Does it read shaft displacement rather than hex corners, groove edges, or socket geometry? |
| Changeover set | Is each variant mechanically keyed and matched to the correct recipe? |
For thin or hardened extensions, the feasibility test should establish a safe correction window. If the drawing or customer quality plan requires crack inspection, surface inspection, or functional torque testing, those checks belong in the validation and production plan.
Automation Is Selected After Feeding Trials
| Automation Level | Suitable Situation | Typical Scope |
|---|---|---|
| Manual loading | Many variants, lower volume, or feasibility stage | Operator loads; machine measures, corrects, and verifies |
| Tray or magazine feeding | Stable orientation and controlled presentation | Guided feeding, automatic cycle, and result indication |
| Validated bulk feeding | High volume and parts proven not to tangle or overlap | Feeder, escapement, orientation checks, and reject/recovery logic |
| Integrated line | Stable family with upstream/downstream interfaces | Buffer, handling, result separation, and agreed communication |
| Traceable cell | Part-level records required | Part ID, recipe, measurement, and correction history |
Cycle time must be measured on the final configuration. It depends on length, measuring positions, number of correction iterations, feeding method, variant checks, and data requirements—a short video clip or one successful sample cannot establish production capacity.
Sample Test and Acceptance Plan
Representative samples: each end-interface and length variant in the proposal; normal parts plus samples near the expected incoming-bend limit; each material, heat-treatment, and coating condition; parts from more than one production batch where springback may vary; and enough samples to evaluate repeatability, not only one corrected part. Evidence to record:
| Record | Acceptance Evidence |
|---|---|
| Part identity | Drawing revision, variant, batch, and process route |
| Incoming measurement | Datum, measuring positions, gauge, and deformation curve |
| Tooling configuration | Locators, support span, punch, and prohibited contact zones |
| Correction history | Position, force/displacement, and iteration count |
| Final machine result | Same datum and method used for incoming measurement |
| Gauge correlation | Comparison with the customer’s final or functional gauge |
| Surface/end inspection | Marks, cracks, and interface condition to the agreed rule |
| Cycle observation | Measured time for the validated configuration |
Common Failure Modes and Controls
| Failure Mode | Likely Cause | Control |
|---|---|---|
| Unstable reading at a hex or groove | Probe follows profile geometry | Move to approved smooth zone or validate profile-specific measurement |
| Shaft passes but holder wobbles | Wrong datum or eccentric end feature | Add interface-axis and functional-gauge correlation |
| Mark on hex, groove, or socket | Incorrect support/punch location | Mechanically protect and software-block prohibited zones |
| Crack after correction | Excess bend, local hardening, or unsuitable span | Stage correction, set limits, and add required crack inspection |
| Variant loads backwards | End geometry not reliably distinguished | Add poka-yoke, presence/orientation sensing, and reject logic |
| Result changes after changeover | Tooling and recipe mismatch | Key tooling and verify the selected variant before cycle start |
What This Solution Does Not Promise Without Validation
- one fixed accuracy for every 1/4-inch extension;
- correction of every incoming bend or every heat-treatment condition;
- zero surface marks, zero wobble, or zero crack risk;
- a universal 10–15 second cycle or a fixed yield percentage;
- random bulk feeding or perfect orientation for every geometry;
- one operator supervising a stated number of machines;
- automatic traceability, MES connection, or line integration unless ordered;
- that a reported 0.2 mm target has already been achieved in stable production.
Information to Send for a Proposal
Send the drawing and revision, representative samples, end-interface details, material and heat treatment, manufacturing route, incoming deformation range, final characteristic and datum, measuring method, allowed contact zones, surface/crack requirements, output target, variant range, and preferred loading method. The proposal will define the measurement datum, tooling, correction limits, automation scope, and acceptance evidence for your real workpiece family. For the wider screwdriver-bit and tool workpiece family, the same platform covers screwdriver bit straightening; long magnetic extension rods are covered by the automatic rod straightening machine line. Contact us for a sample-based extension bar straightening study.
Frequently Asked Questions
Is every 6.35 mm extension measured in the same way?
No. A 6.35 mm or 1/4-inch interface identifies a nominal drive family, not the entire datum and inspection method. The end geometry, shaft zones, retention features, and drawing requirement determine how the part is located and measured.
Can the machine measure directly on the hex shank?
Potentially, but a generic round-shaft probe will react to the hex profile. Measurement on an approved smooth zone is usually simpler. If the hex must define the functional axis, dedicated location or profile-aware measurement must be validated against the customer’s gauge.
Can hardened extension bars be press straightened?
They may be feasible, but the correction window depends on material, hardness, hardened depth, incoming bend, support span, and contact location. Representative sample testing and the required crack/surface inspection are necessary before a guarantee is made.
What accuracy can be guaranteed?
Only the result demonstrated for the agreed workpiece family, incoming-condition window, datum, and acceptance gauge can be guaranteed. A value from an earlier article, competitor page, or video is not a substitute for sample evidence.
Does the machine include automatic feeding?
It can. Manual, tray, magazine, bulk, and integrated-line handling are different project scopes; the final choice follows real-part feeding and orientation trials.