
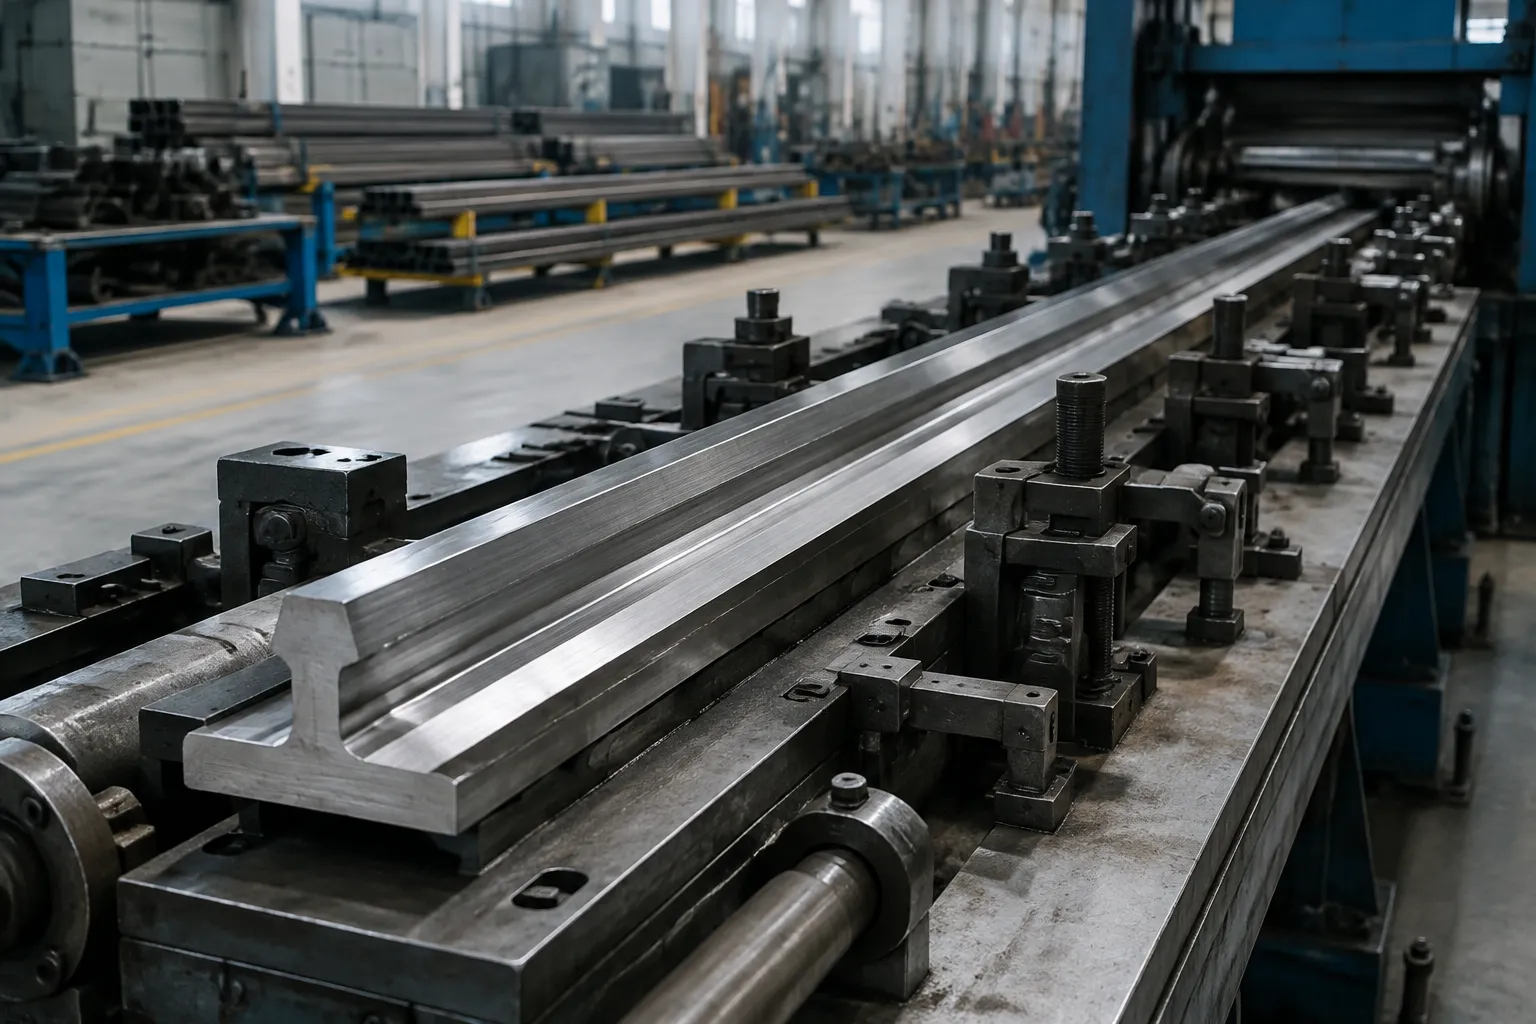
Straightening an elevator guide rail is manufacturing-stage geometry work, and it has nothing to do with aligning rails inside a hoistway. The production route has to control the section, the reference faces, the length, the bow, the lateral sweep, the twist, the surface condition, and every interface to machining, inspection and packing. Elevator guide rail straightening thus carries its own datum, measurement and correction discipline — none of it inherited automatically from round-bar practice.
What follows is a workpiece-based engineering framework. It makes no claim about handling any particular rail profile, length, production rate or acceptance tolerance — those questions need a drawing review, representative rails, measurement agreement and a validated sample process.
Engineering concept illustration. It depicts a candidate manufacturing-stage rail process, not an installed-elevator alignment service or a delivered-machine record.
Separate Manufacturing Straightness From Installation Alignment
Search around elevator guide rail machines and three different intents surface: dedicated straighteners, complete guide-rail production lines, and installation questions. Only the first two belong on a factory page. What manufacturing controls is whether the delivered rail meets its geometric requirement with all correction forces removed; installation alignment is about the building, the brackets, the joints and the field survey. Separate measurement systems, separate acceptance statements — the two must never be merged.
| Scope | Typical controlled issue | Do not substitute |
|---|---|---|
| Rail manufacturing | Section geometry, longitudinal bow, lateral sweep, twist and surface condition | A field plumb or rail-spacing check |
| Production-line integration | Feed, straightening, cutting, machining, inspection and packing interface | A promise that every line configuration is supplied |
| Hoistway installation | Brackets, joint alignment and verticality in the building | A factory straightening result |
The market itself is split the same way: Senbo publishes dedicated guide-rail straightening equipment, Co-effort publishes production-line scope. A sensible site keeps the workpiece solution apart from any production-line buying guide.
Neighboring manufacturing-geometry topics — linear guide rail straightening and railway rail straightening — each demand their own section, datum and process review. Neither substitutes for an elevator rail qualification.
Define the Rail Section, Datum and Error Map
Until the section, reference faces, span and measurement condition are on paper, “rail straightness” is an incomplete phrase. On a T-shaped or otherwise asymmetric profile, vertical bow, lateral sweep and twist coexist; a poorly chosen support pattern then adds apparent geometry of its own whenever the rail sags or seats inconsistently.
The engineering review freezes:
- rail drawing, profile variant, length and manufacturing stage;
- datum faces, permitted support zones and cosmetic or functional protected zones;
- the acceptance characteristic for each plane and the method used to calculate it;
- whether twist is controlled, how orientation is indexed, and how intentional section variation is treated;
- incoming error distribution, handling condition and the reference gauge or inspection fixture;
- machining, cutting, joining, packing and downstream interfaces that can reintroduce distortion.
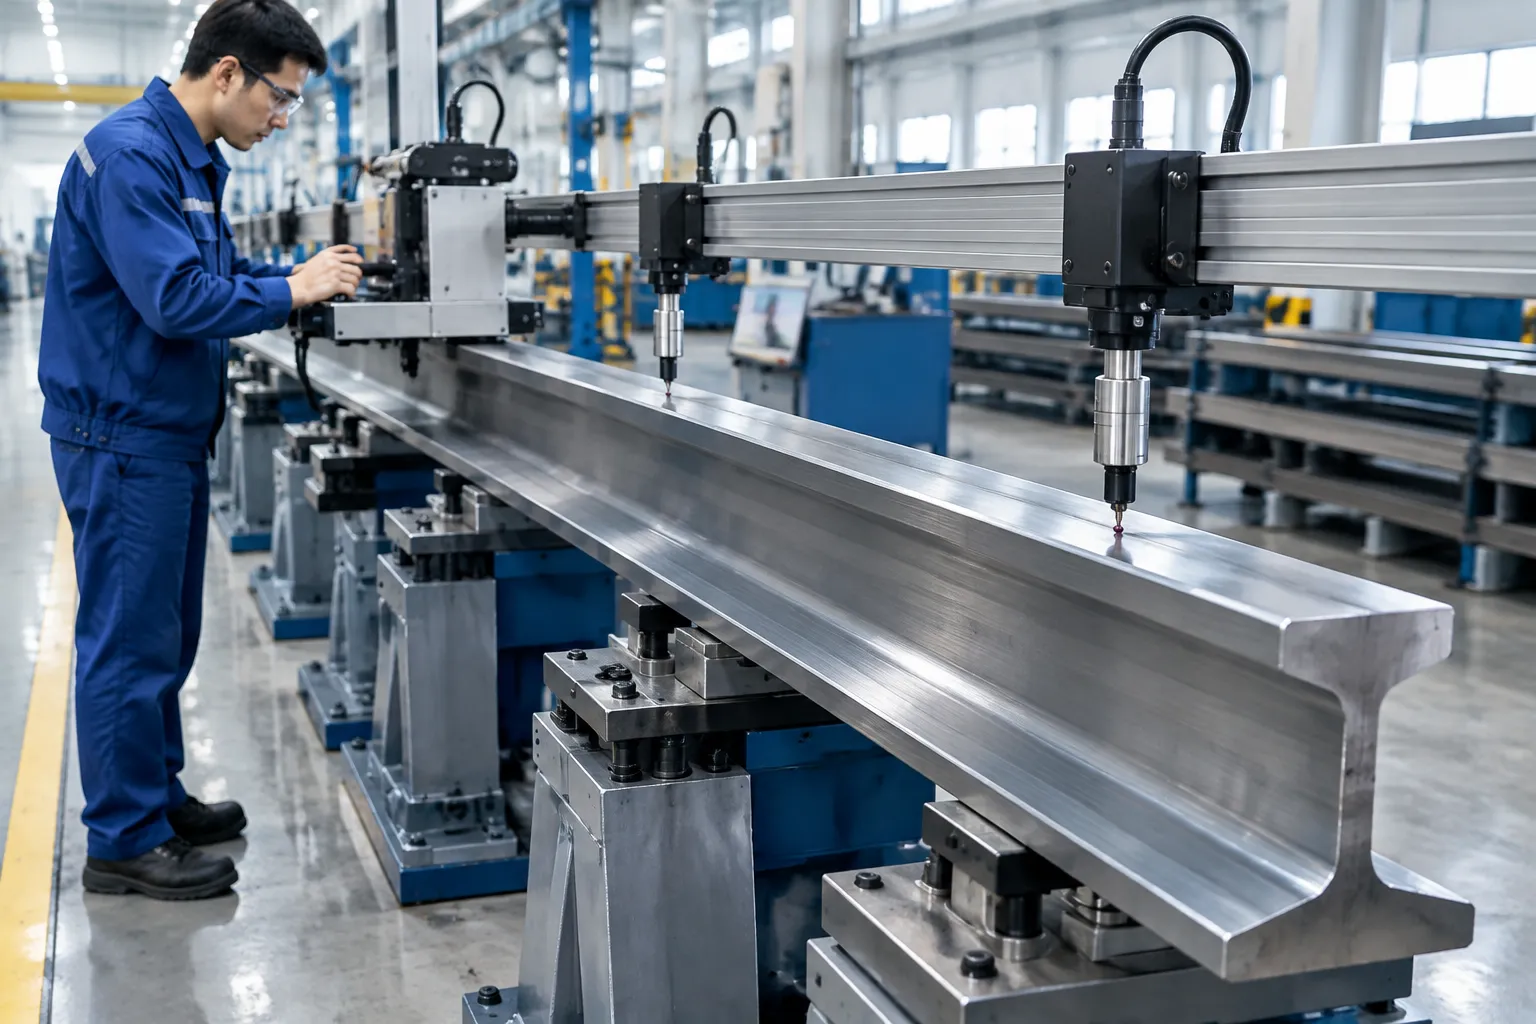
Engineering concept illustration. It shows a possible full-length measurement approach; the actual sensor positions, span and datum must be validated for the rail family.
Where Rail Distortion Comes From
By the time a rail reaches a straightening station, its geometry has a long history. Rolling leaves residual stress through the section — distributed unevenly between the head and the web — and the mill cooling bed adds a field of its own. Any straightening done at the mill counts as prior history: a rail that arrived rotary-straightened has already spent part of its deformation budget and responds differently to further correction, the reverse-loading behavior explained for the Bauschinger effect. Cutting to length frees constraint at the ends, which is why end geometry often behaves unlike mid-length geometry. Machining the guide faces strips surface material and lets buried stresses relax unevenly. Handling closes the story: lift a long rail at the wrong points, or store it standing under its own weight, and it collects bends no process ever intended. Each source predicts a signature — where the peaks sit, whether sweep or twist dominates — and reading that signature off the incoming map is what upgrades correction from generic pressing to a planned route.
The T-Section’s Mechanical Personality
A T-section is not a round bar with corners attached. Direction decides stiffness: bending about one axis of the profile meets far more resistance than bending about the other, so vertical bow and lateral sweep are two different mechanical problems — two correction economics — rather than two readings of one. The open profile is torsion-sensitive as well; a modest rotation about the longitudinal axis displaces the guide faces at the two ends in opposite directions, which is how a rail can pass a bow check at every station yet still present a twisted functional surface to the car shoes. And the guide faces are the product: precisely where contact is unavoidable for measurement reference, it is also cosmetically or functionally restricted — the tension that makes surface-protection tooling practice and conservative contact-zone choice inseparable from the geometry plan itself.
Measure Bow, Sweep and Twist as Different Signals
Straight in one view can still fail in another. Map the agreed stations and directions before touching correction, and keep vertical bow, lateral sweep and twist as separate stored characteristics instead of collapsing them into one “bend” number.
| Characteristic | Measurement question | Engineering consequence |
|---|---|---|
| Vertical bow | Which datum plane and span define the result? | Determines support and correction direction |
| Lateral sweep | Is the web or guide face referenced consistently? | May need a different correction orientation |
| Twist | Which faces establish angular orientation? | Cannot be inferred from one linear probe |
| Fixture/sag signal | Does a reseat or changed support pattern alter the reading? | Requires setup review before correction |
Long-part support is part of the measurement. A map that changes when supports move is not yet a correction map — distinguish free-state behavior from the controlled support condition the drawing and customer inspection use, the separation formalized in loaded versus released measurement and extended to profiled sections in full-length profile scanning.
Choose Contact and Correction Zones Conservatively
Correction itself may take the form of controlled point pressing, roll straightening or another section-specific method; rail geometry, material condition, error pattern, accessible contact areas and surface risk decide which. A point-correction sequence written for a round shaft does not transfer to an asymmetric rail unchanged.
Before any trial: name the approved supports, the reaction path, the load points, the protective contact materials, the orientation controls and the maximum correction attempts. Accessibility alone never qualifies a surface for force. Machined guide faces, reference faces, connection features and cosmetic zones may need protection or may be off-limits as contact points entirely.
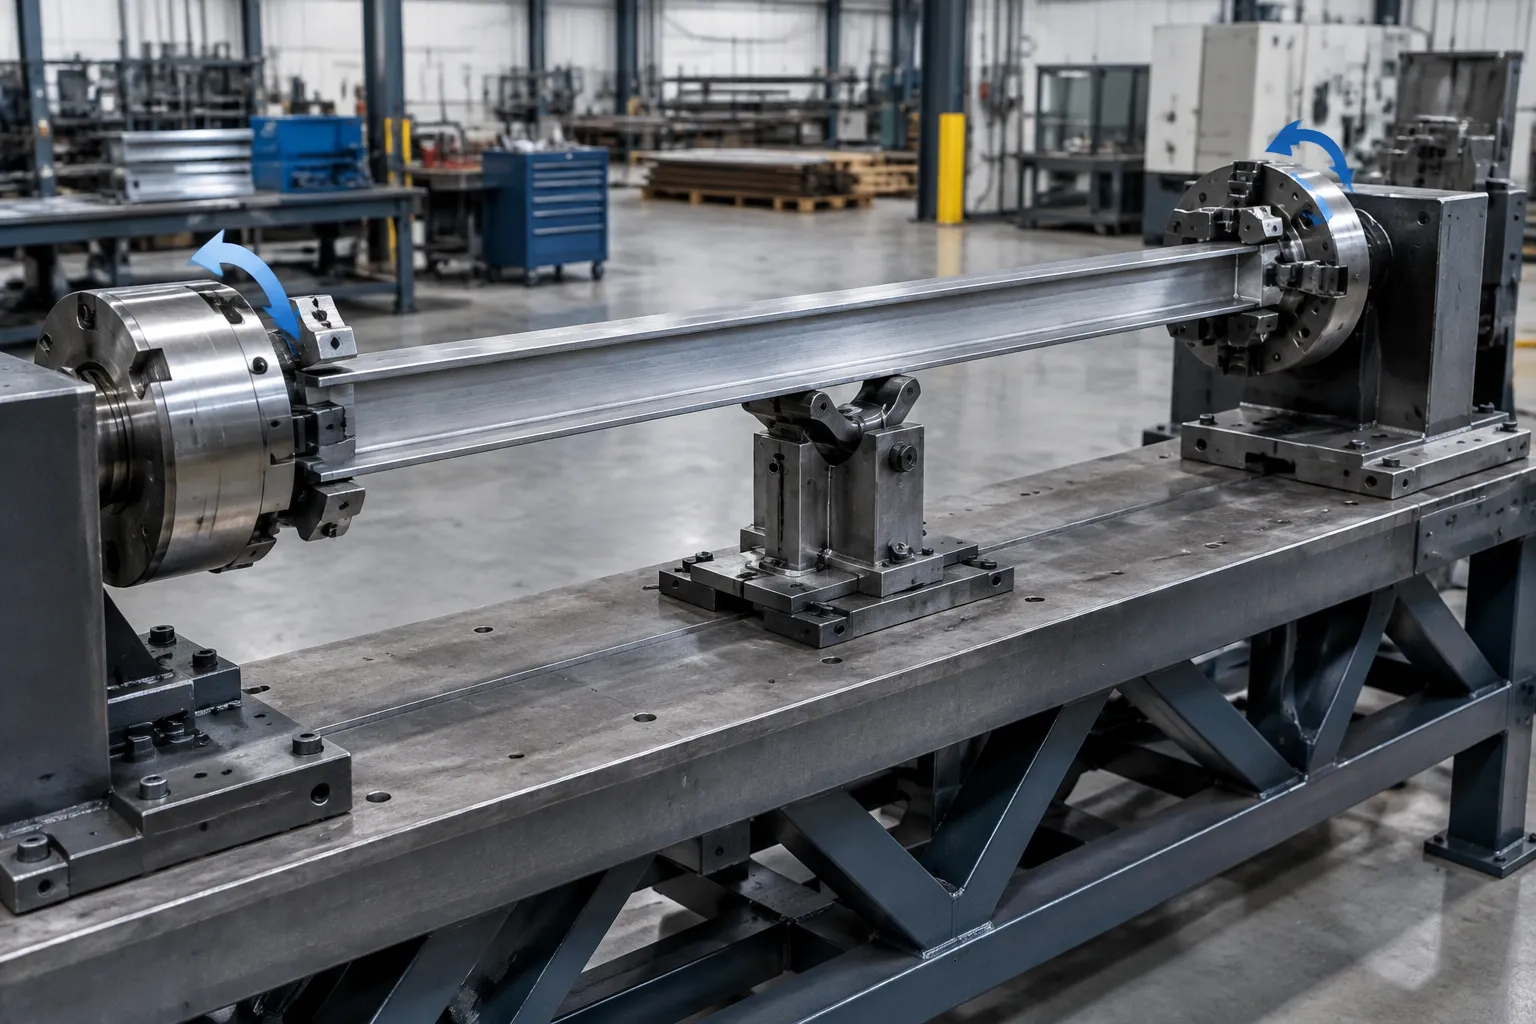
Engineering concept illustration. It distinguishes a possible angular-correction problem from ordinary vertical pressing; it does not prove that a specific rail or machine supports torsion correction.
Use a Measure-Correct-Release-Remeasure Loop
Released geometry is the only geometry that counts. While the rail is held by tooling or still under correction force, a reading proves nothing about final shape.
- identify the rail family, drawing revision and manufacturing stage;
- inspect for damage, wrong profile, unapproved surface condition or out-of-scope deformation;
- load the part in the approved orientation and verify support seating;
- capture the vertical, lateral and angular error map required by the acceptance plan;
- select the permitted correction plan and protect all no-contact zones;
- apply incremental correction within the approved limit;
- release force and restraint completely;
- remeasure, record disposition and route no-progress rails to engineering review.
Build the Sample Test Around the Customer Gauge
Compare the machine method against the customer’s controlled reference method — typical and worst-case incoming rails, repeat setup checks, released-state readings, surface inspection, traceability, and a defined route for rails that need repeated correction or refuse to respond.
| Acceptance item | Evidence needed before a production claim |
|---|---|
| Bow, sweep and twist | Raw before/after readings tied to drawing datums and spans |
| Fixture repeatability | Reseat study and support-condition record |
| Surface protection | Approved inspection criteria and photos or reports |
| Handling and line interface | Qualified transfer, orientation and safety review |
| Throughput and automation | Timed, validated run for the agreed rail family |
The full trial architecture is defined in straightening sample test and acceptance, the measurement-system separation in Gage R&R for straightening lines.
Information Needed for an Elevator Guide Rail Straightening Review
Bring the controlled rail drawing and section variants, length, material and manufacturing stage, incoming geometry data, datum and acceptance method, permitted support and contact zones, surface requirements, production target, handling constraints and representative rails. From there a review can cover candidate measurement, support and correction architecture and define the sample-test evidence needed before any machine configuration is proposed — starting at the contact page.
FAQ
Is this an elevator installation-alignment guide?
No — factory manufacturing geometry only. Hoistway alignment, brackets and field installation form a separate scope with separate measurement systems.
Can one correction station control bow and twist?
Not by default. Each mode — bow, lateral sweep, twist — needs its own datums, measurement tracks and correction validation, per the separation in twist correction.
Can a rail be accepted while it is clamped?
No. Acceptance follows the agreed released-state condition; clamping masks springback and sag.
Can a section, length or cycle time be specified from this article?
No. Those numbers come from a verified rail family, machine capability, tooling review and representative sample test.
Why does the same rail profile distort differently across lots?
Lot to lot, the rolling conditions, cooling-bed position, prior straightening history and storage all shift — and each writes a different residual-stress pattern into the section. Answer with per-lot incoming mapping, not one inherited recipe, the lot-scatter logic of springback variation in straightening.
Is point pressing or roll straightening better for guide rails?
Neither wins by default. Discrete, mapped peaks on an asymmetric section with defined contact zones favor point pressing; continuous correction of compatible sections at volume favors rolls. Draw the boundary — and the sample-test evidence each route owes — from the press versus roller straightening comparison, with the rail’s protected faces in view.
How does twist show up when only linear probes are used?
Twist disguises itself as contradictory bows: the same face displaces in opposite directions at the two ends of a single probe track. Confirming it takes orientation-aware measurement on defined faces at multiple stations — which is exactly why the error map stores bow, sweep and twist separately rather than as one combined value.
Related Reading
See also: Industrial Components Straightening, Linear Guide Rail Straightening, Hydraulic Straightening Machine, Precision Straightener.