
A thin-walled tube rarely arrives with only one defect. Bend, ovality, local dents and twist frequently coexist, and a correction cycle that fixes the centerline can still scrap the part by collapsing the cross-section, wrinkling the wall, marking a finished surface or damaging the weld seam.
Any credible thin-walled metal pipe straightening solution therefore has to control two things at once: the global geometry of the tube and the integrity of the local cross-section. The engineering starts from the drawing, the tube construction and the manufacturing stage — never from a generic press force or an inherited roller setting.
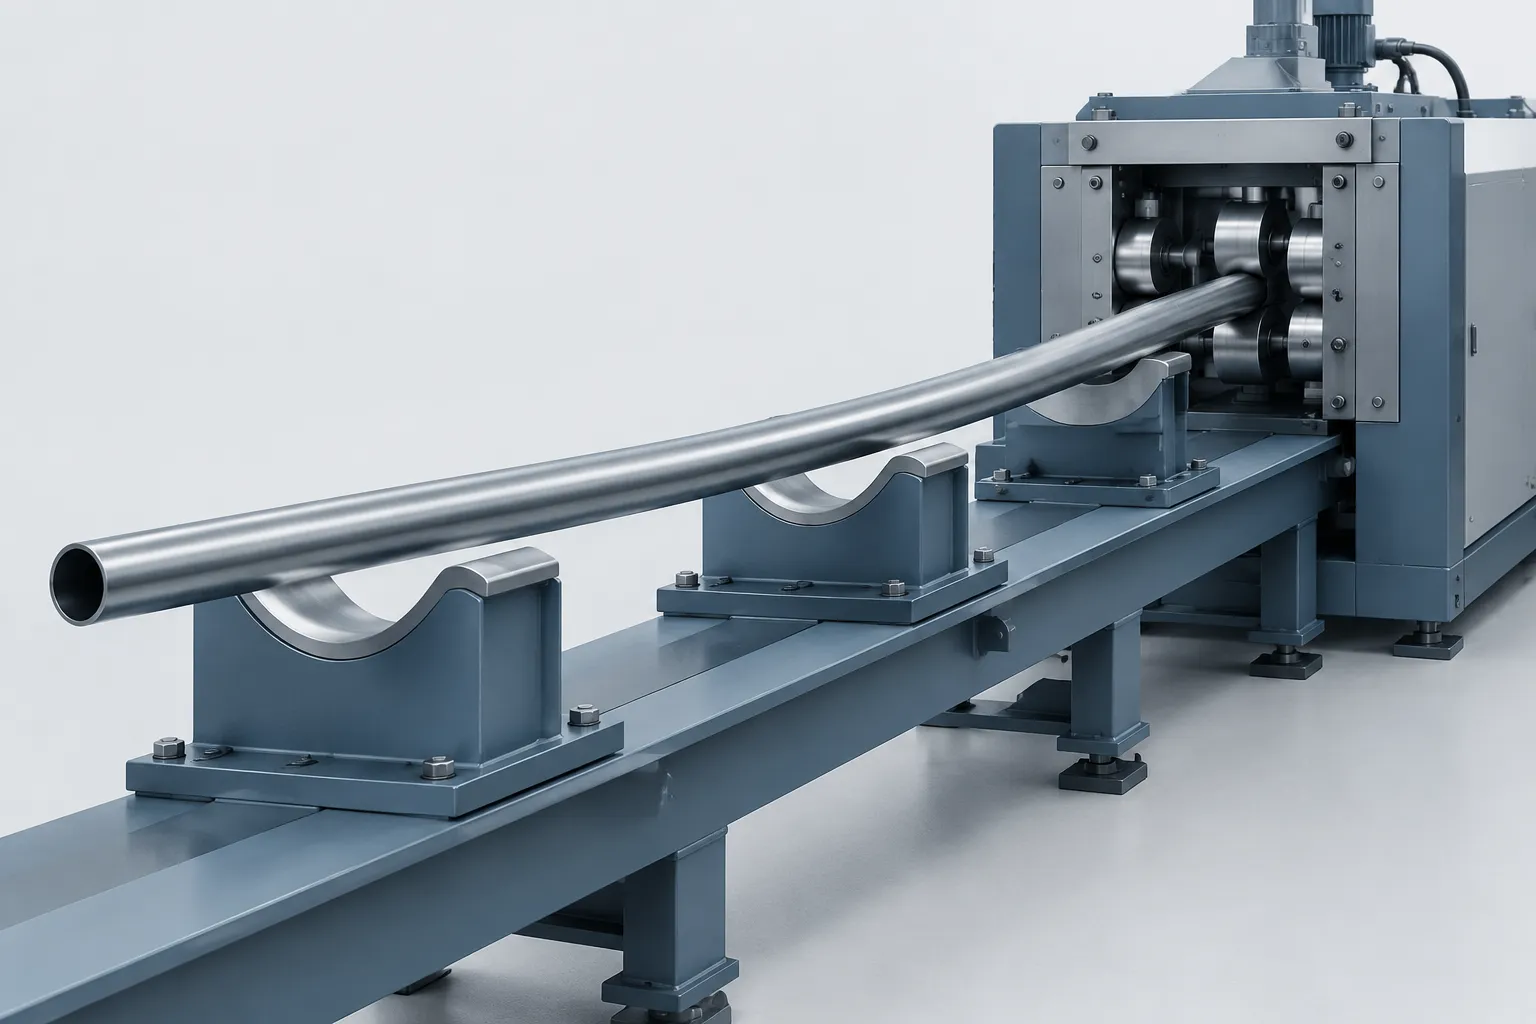
Engineering concept illustration — not a photograph of a customer installation. Real supports, sensors and correction tooling always depend on tube diameter, wall thickness, material, section and sample-test results.
What Makes a Thin-Wall Tube Different
| Tube Property | Risk During Straightening | Engineering Response |
|---|---|---|
| Hollow section | External correction load can flatten or collapse the tube | Control contact geometry, pressure, and decide whether internal support is needed |
| Small wall thickness relative to diameter | Local buckling and wrinkling can appear before any useful correction | Validate strain and support span on worst-case samples first |
| Pre-existing ovality | A rotating measurement can mix form error with true bend | Measure centerline and section shape as separate characteristics |
| Welded seam | Seam stiffness and damage sensitivity change with angular position | Detect or index the seam and define protected sectors |
| Finished outer surface | Rollers or press tools can leave dents and witness marks | Approve contact material, width, cleanliness and surface criteria in advance |
| Long, flexible length | Self-weight sag alters the measured curve | Freeze support span, orientation and sag treatment in the recipe |
| Bent, tapered or stepped tube | Straight rotation and uniform tooling may not apply | Use section-specific supports and station maps |
| Open ends | End sections deform more easily than the body | Define a minimum usable end distance and dedicated end support |
“Straightness achieved” must never be the only success criterion on a thin-wall project. Cross-section shape and surface condition have to stay inside their own agreed limits, otherwise the part fails downstream even though the dial indicator improved.
Separate the Defects Before Choosing a Method
Centerline Bend
The tube axis drifts along its length. This is the classic target of bending correction and the only defect an ordinary straightening recipe is designed to attack.
Ovality and Local Flattening
The cross-section is no longer acceptably round. Ovality may be present on arrival, produced by clamping, or created by the straightening contact itself.
Local Dent or Collapse
A concentrated load pushes a local inward deformation into the wall. Improving the centerline does nothing to remove this damage.
Wrinkling or Buckling
When correction strain is too high or the wall is insufficiently supported, the compression side forms waves or a local buckle.
Twist
A plain round tube can hide twist, but any tube with features, seams, holes or attached brackets exposes it. Rectangular and shaped tubes demand explicit torsion measurement and a different correction strategy.
Weld Distortion
Longitudinal seams, end welds and attached fittings introduce asymmetric deformation and local strength differences. A welded assembly must never be processed as if it were uniform raw tube.
Freeze the Tube Construction and Process Stage
Before any machine parameter exists, the project must pin down whether the workpiece is:
- seamless or longitudinally welded;
- round, oval, square, rectangular or another profile;
- straight raw tube, a cut-to-length blank or a formed part;
- annealed, heat-treated, coated, polished or otherwise finished;
- empty, fitted with internal components, or part of a welded assembly;
- scheduled before or after machining, bending, welding or surface treatment.
Straightening raw tube ahead of finishing follows different surface and allowance rules than correcting a polished automotive tube or a welded cooling manifold. Because later processing can reintroduce distortion, the route may need more than one controlled geometry check — the same stage-freezing logic that governs heavy seamless steel pipe straightening.
Define Global and Local Acceptance Together
| Characteristic | What It Controls | Why It Must Stay Separate |
|---|---|---|
| Axis/centerline straightness | Global tube path | Proves nothing about cross-section roundness |
| Circular/total runout | Rotational variation against a datum | Blends reference error and section-form error together |
| Outside diameter | Local size | Can shift during flattening or expansion |
| Ovality/roundness | Cross-section shape | The direct collapse indicator for round tubes |
| Wall thickness | Section strength and forming response | Varies around welded or drawn tube |
| Surface condition | Dents, scratches, coating and cosmetic marks | Independent of the centerline result |
| Seam condition | Weld integrity and location | Can dictate orientation and correction limits |
| Twist | Angular change along shaped or featured tube | Invisible to a single radial probe |
The drawing and the customer gauge must together define stations, datum, support condition, filters and decision rules. Before anyone reads a rotating indicator signal as tube straightness, work through the geometry definitions in tube ovality vs centerline straightness.
Measure Centerline and Ovality Separately
One contact probe riding on the outside diameter cannot always tell a bent-but-round tube from a straight-but-oval tube. Multiple angular readings, opposing sensor pairs, diameter scans or a suitable non-contact system may all be required before the two effects can be separated.
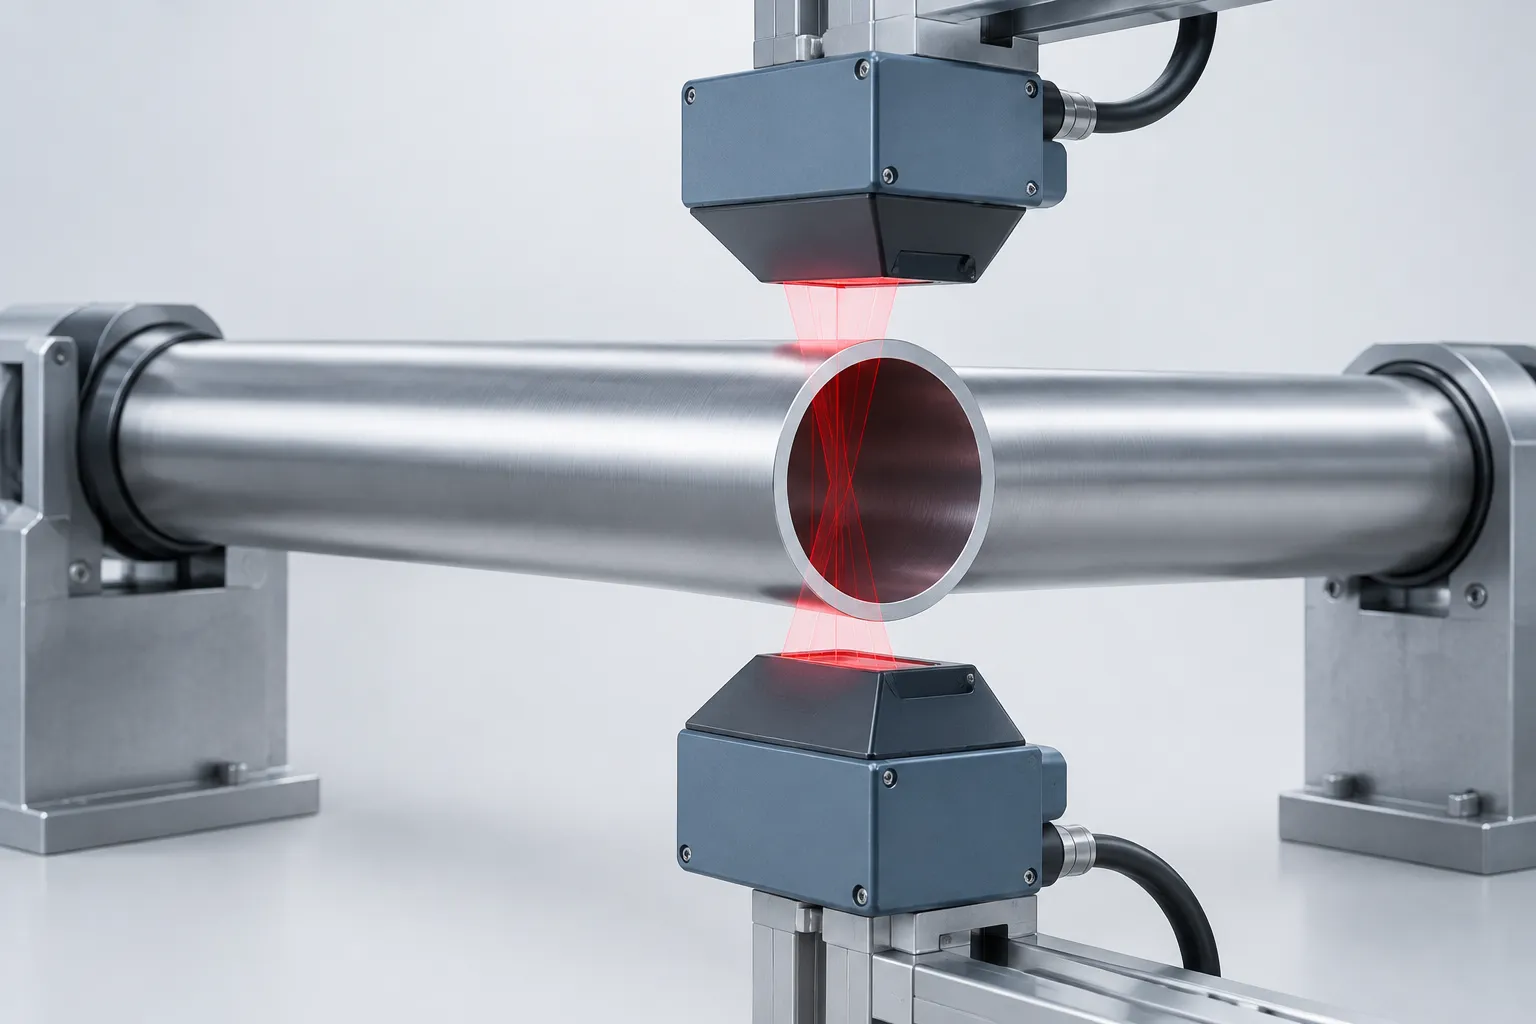
Engineering concept illustration of non-contact centerline and diameter measurement. It does not prescribe optical sensors for every tube.
| Measurement Element | Project Definition Required |
|---|---|
| Datum/reference | Ends, journals, fittings, mathematical axis or customer fixture |
| Axial stations | Global curve points plus high-risk local sections |
| Angular coverage | Enough directions to separate bend from ovality |
| Support plan | Number, span, height and contact pressure |
| Seam indexing | Seam angle at measurement and correction stations |
| Probe method | Contact force, or non-contact range/resolution |
| End exclusion | Minimum distance from unsupported or open ends |
| Released condition | Measure only after external and internal correction loads are removed |
For non-round tube, the system may need multiple faces, edges or section-specific coordinates instead of a simple rotational runout model.
Support the Tube Without Creating the Defect
Supports have to hold and move the tube while keeping contact pressure below the validated local deformation limit. The variables that decide whether they succeed include:
- saddle radius and conformity to the actual OD;
- roller width and edge radius;
- sleeve and pad material, and embedded-particle risk;
- support span and intermediate support positions;
- tube rotation and axial-feed forces;
- clamping pressure and grip length;
- open-end support and minimum contact distance;
- weld-seam angle relative to every contact;
- cleaning and tooling-inspection frequency.
A soft pad can still dent a tube when the contact area is too small or contamination is trapped beneath it. All tooling must be validated on the minimum wall thickness and the weakest included material condition, not on a convenient mid-range sample.
Press Straightening vs Roller Straightening
| Route | Strong Starting Fit | Main Thin-Wall Risk |
|---|---|---|
| Localized press straightening | Discrete bend zones, feature-rich parts, low/medium mix | Local flattening, denting and compression-side wrinkles |
| Multi-roll/continuous straightening | Long uniform tubes with distributed curvature | Repeated contact, ovality growth, end effects and surface marking |
| Moving-frame correction | Long tubes that are difficult to reposition | Support transitions and station correlation |
| Internal-support-assisted correction | High collapse risk at known local zones | Mandrel insertion, fit, friction and removal |
| Hybrid process | Pre-straighten stock, then finish with targeted correction | Clear acceptance and responsibility at each stage |
Method selection follows the general press-vs-roller trade-offs, then adds the thin-wall constraints of section stability and surface protection. A dedicated tube straightening machine is built around exactly those added constraints rather than adapted from solid-bar practice.
Internal Support: an Option, Never a Default
An internal mandrel, expandable support, plug or local backing device can reduce collapse risk at the correction zone — and simultaneously introduce a completely new set of failure modes.
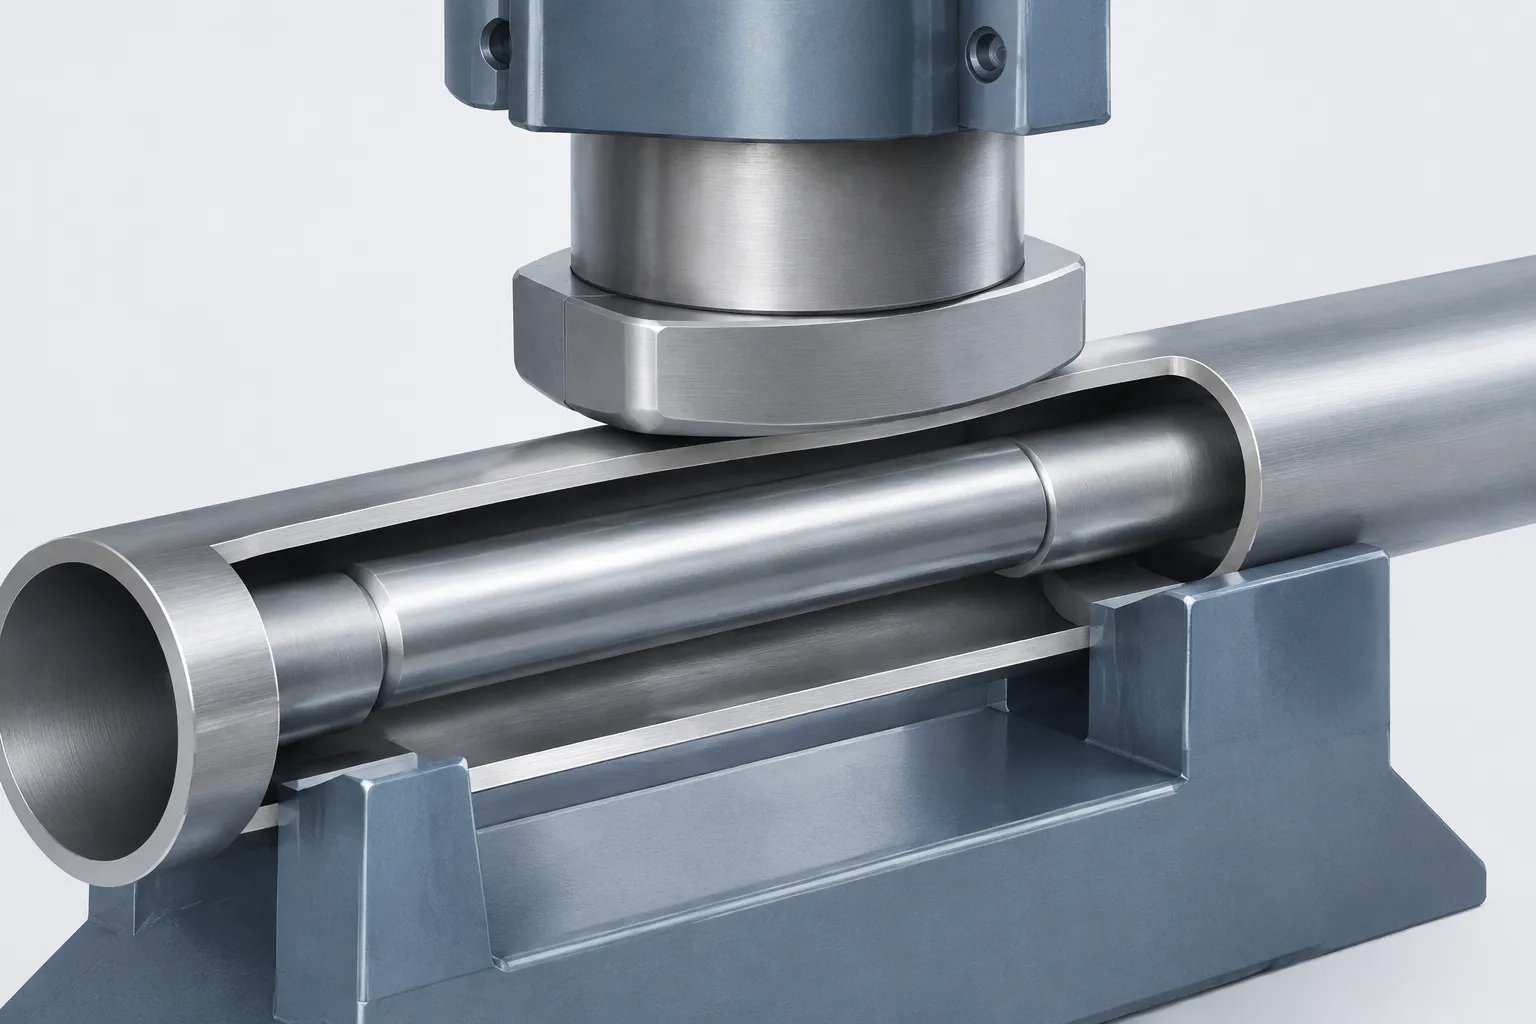
Cutaway engineering concept illustrating one possible internal-support arrangement — not a universal production design.
| Internal-Support Question | Why It Matters |
|---|---|
| Can the device enter and reach the correction zone? | Bends, length, fittings and closed ends may block access |
| What is the support clearance? | Too loose gives almost no support; too tight scores or jams |
| How is it positioned? | The internal support must align with the external load zone |
| Fixed or expandable? | Expansion force can itself change diameter and ovality |
| What is the contact material? | Internal scratches or contamination may be unacceptable |
| How is it removed? | Springback, burrs or deformation can trap the device inside |
| Can several stations be corrected? | Repositioning the support affects cycle time and control complexity |
| How is internal condition inspected? | Damage may be invisible from outside |
Alternatives worth evaluating instead of a mandrel include broader external tooling, lower incremental correction steps, hydro or pneumatic assistance where appropriate, or simply moving the straightening operation to an earlier process stage. Every alternative still requires its own safety and validation plan.
Weld Seam and Feature Indexing
On welded tube, seam position influences stiffness, measurement and damage risk simultaneously. The recipe must state whether the seam is:
- detected automatically or oriented manually;
- permitted to sit under a support or press tool;
- excluded from high-strain correction sectors;
- measured for local profile or integrity;
- tracked through the entire cycle.
Holes, slots, beads, brackets, flares, swages and end fittings all change local stiffness too. An ordinary OD sensor or press tool should never cross these features without a defined method.
Controlled Correction and Springback
Localized correction uses a validated span and broad conforming contacts. The machine applies only enough controlled over-bend to leave permanent correction in the tube after the load releases.
The recipe bounds must cover:
- support and correction coordinates;
- seam and feature angular orientation;
- maximum force, stroke and loaded displacement;
- maximum section deformation allowed during loading;
- correction increment and attempt count;
- reverse-correction or oscillation rules;
- internal-support state and position;
- post-release straightness, ovality and surface checks.
Final acceptance is measured only after the external load and any internal expansion force are fully released. Iteration and stop logic follow the same bounded-springback discipline used across shaft and bar correction, where each additional press is justified by data rather than operator persistence.
A Defensible Automatic Cycle
- Identify the tube family, drawing, construction and process-stage recipe.
- Confirm diameter/section, wall range, material and seam/feature condition.
- Clean the tube and inspect external and internal support tooling.
- Load onto broad validated supports and locate the tube axially.
- Detect or index the seam and prohibited features where required.
- Measure centerline and cross-section characteristics at the agreed stations.
- Separate sag, ovality and local dents from correctable global bend.
- Select the approved correction method, span and optional internal support.
- Apply bounded correction while monitoring force, stroke and section risk.
- Fully release external and internal loads and restore the measurement condition.
- Remeasure centerline, ovality/section and surface/seam criteria.
- Record results and route the part to OK, recheck, secondary operation or NOK.
Round, Rectangular and Formed Thin-Wall Tubes
| Tube Family | Additional Control Required |
|---|---|
| Round seamless tube | Bend/ovality separation and end collapse |
| Longitudinally welded round tube | Seam indexing and integrity |
| Square/rectangular tube | Face flatness, corner radii, twist and wall buckling |
| Oval/formed section | Section-specific supports and measurement model |
| Bent tube assembly | 3D datum, tangent/angle and local bend geometry |
| Tube with fittings | Grip/feature protection and access for internal support |
| Multi-channel/extruded tube | Internal webs, torsion and local crush behavior |
| Coated/polished tube | Surface contact and cosmetic standard |
None of these families should share an unvalidated universal recipe.
Machine and Data Modules
| Module | Project Definition |
|---|---|
| Loading/transfer | Manual, conveyor, gantry or robot, with anti-sag handling |
| Part identification | Section, wall/material family and wrong-recipe prevention |
| Seam/feature detection | Camera, sensor, fixture or manual index |
| Support line | Saddle/roller geometry, span, setup and wear monitoring |
| Measurement | Centerline, diameter/ovality, twist and local-section stations |
| Correction | Press, rollers, moving frame or hybrid process |
| Internal support | Type, positioning, expansion, insertion and removal |
| Surface/seam inspection | External and internal criteria after correction |
| Traceability | Initial map, correction history, final map and reject reason |
| Quality interface | Customer gauge correlation and reference-master checks |
Sample Test and Acceptance Matrix
| Test Group | Representative Samples | Evidence Required |
|---|---|---|
| Diameter/wall range | Largest diameter with thinnest wall, plus boundary combinations | Collapse behavior and tooling envelope |
| Material/condition | Softest, strongest and finished states | Springback, wrinkle and surface response |
| Welded/seam variants | Seam angles and weld batches | Indexing and integrity result |
| Length/bend range | Shortest/longest, good/borderline/worst incoming | Support, sag and correction map |
| Cross-section | Round plus every approved shaped family | Dedicated gauge and tooling result |
| End/features | Open ends, holes, fittings and formed zones | Exclusion and local support rules |
| Internal support | Insertion/position/removal extremes | No jam, no internal damage |
| Gauge correlation | Same parts on machine and customer method | Offset, repeatability and decision agreement |
Feasibility, FAT and SAT evidence should be defined with the same sample-first structure used for every custom straightening project before a tolerance is promised.
Information Required for a Thin-Wall Tube Proposal
To quote a defensible solution, please provide:
- complete tube/assembly drawing and revision;
- seamless or welded construction, with the seam specification;
- material, temper/heat treatment and process stage;
- round or shaped section, OD/width/height, wall thickness and length range;
- bend, straightness, runout, ovality, diameter, twist and surface requirements;
- datum/reference, measuring stations and the customer fixture;
- incoming bend/ovality/dent distribution and representative rejects;
- holes, slots, welds, fittings, bends, flares and prohibited zones;
- approved external and internal contact surfaces;
- cosmetic, coating, seam and internal-surface acceptance criteria;
- access and clearance available for internal support;
- target throughput, loading method, changeover and traceability needs;
- representative good, borderline and NOK samples.
With these inputs, the engineering team can define the support model, measurement architecture, correction method, optional internal tooling and validation matrix. Final accuracy, cycle time and section integrity are confirmed on the actual tube family — never copied from a generic tube-straightening claim. To discuss a specific tube, start from the contact page.
Frequently Asked Questions
Can a standard bar straightener handle thin-wall tube?
Not without validation. A tube is hollow and can collapse, ovalize or wrinkle under contact loads that a solid bar simply tolerates.
Is straightness alone enough to accept the tube?
No. Ovality, diameter, local dents, surface condition, seam integrity and twist can each control the acceptance decision on their own.
Does internal support always prevent collapse?
No. Clearance, position, expansion force, contact material and removal all matter — a poorly specified mandrel introduces its own damage or dimensional change.
Can an ordinary contact probe measure tube bend?
Its reading can blend bend, ovality, surface form and support effects. The project must define enough angular and station information to separate them, or choose another suitable method.
Should the weld seam face away from the press?
There is no universal orientation rule. Seam design, material, weld condition and load path must be reviewed and tested before the recipe fixes an angle.
Which is better for thin-wall tube — rollers or a press?
It depends on section, curvature distribution, surface stage and collapse risk. Rollers suit some uniform long tubes; localized press correction suits some discrete defects. Both require tube-specific tooling.
Is final geometry checked with the internal support still expanded?
No. Final acceptance uses the released tube in the agreed measurement condition, unless the drawing explicitly defines another state.
Can round and rectangular thin-wall tubes share one setup?
Not automatically. Rectangular tubes add face, corner and torsion behavior, and need section-specific supports, measurement and correction tools.
Engineering concept illustration — released thin-wall tube verified for both centerline and cross-section integrity after correction.
Two questions decide most thin-wall projects before the first meeting with a supplier: how to measure ovality against centerline straightness correctly, and how far correction can be pushed before the section degrades — the heavy seamless-pipe case study shows the same limits at the opposite end of the size range.